in a clamp (with an aluminium bushing) as re-
quired..
Specific tooling
020335Y Magnetic support for dial gauge
020074Y Support base for checking crankshaft
alignment
Refitting the crankshaft
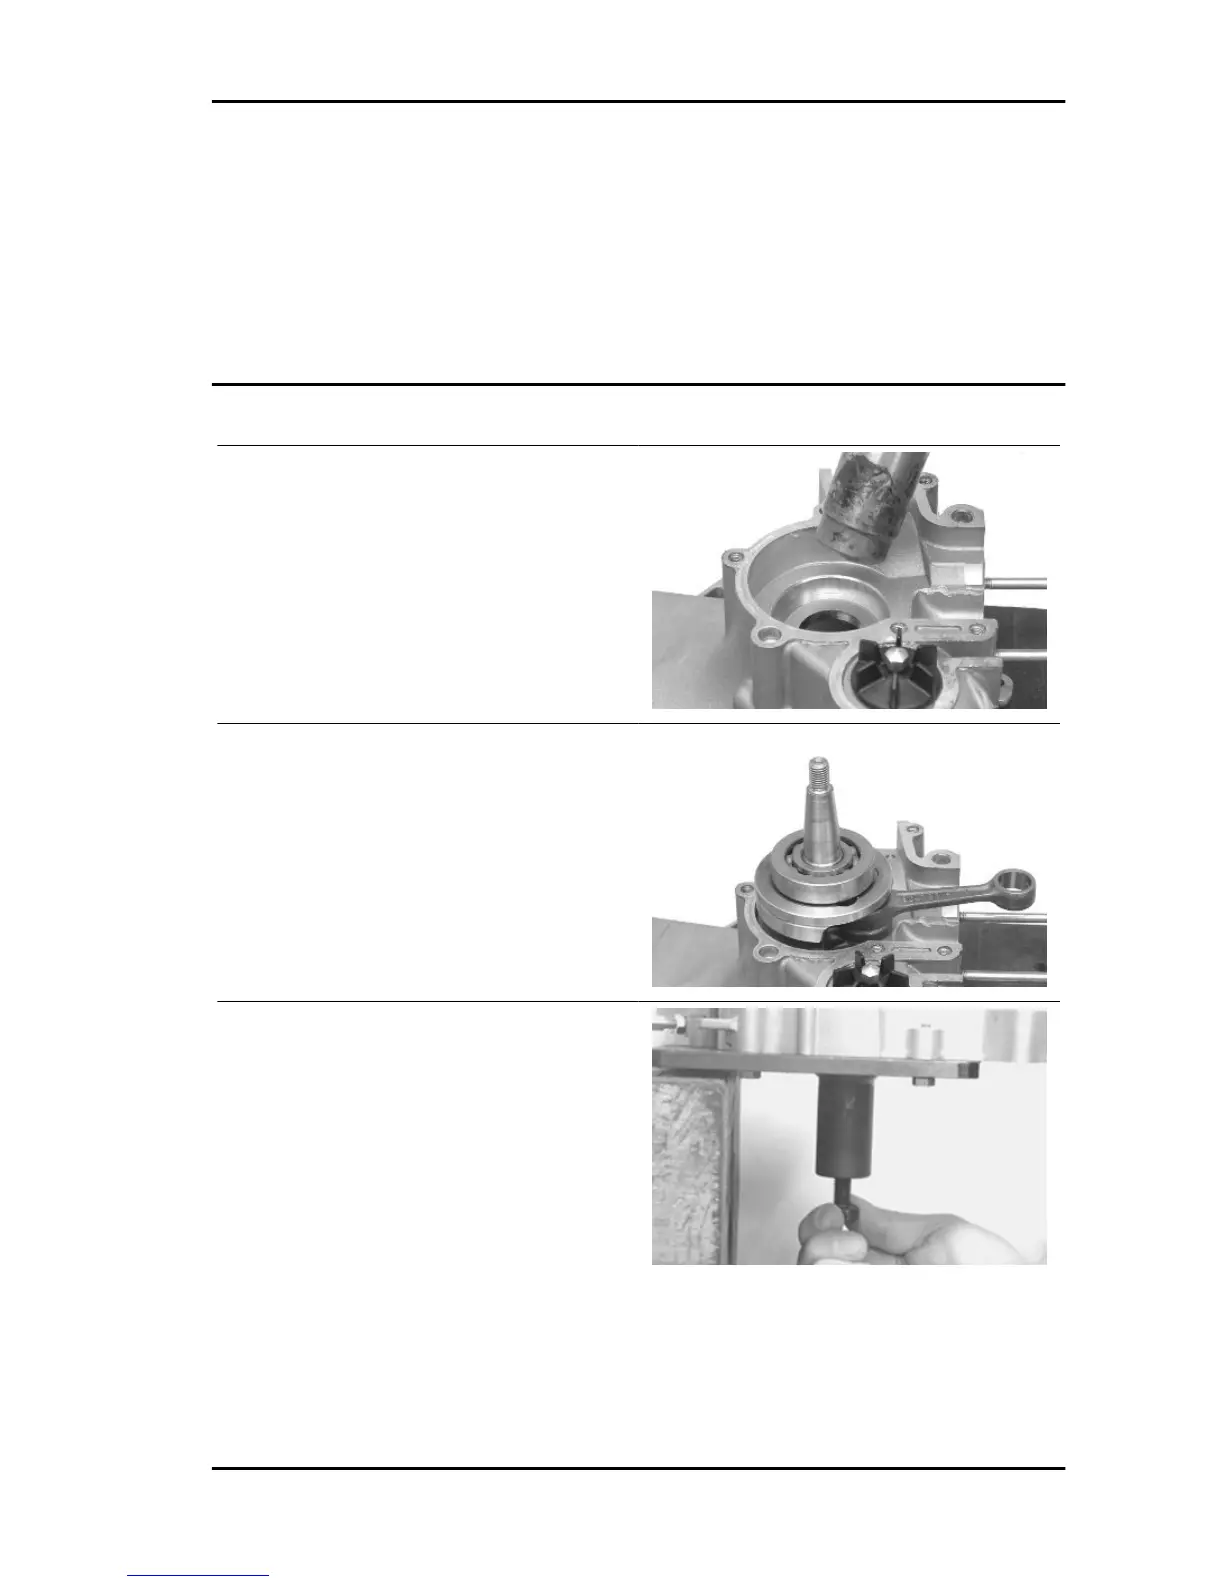
- Position the transmission side half crankcase on
two wooden supports
- Using a thermal gun, heat the bearing seat to
about 120°
- Firmly insert the crankshaft until the bearing rea-
ches the end-of-stroke stop
- Let the temperature of the half crankcase settle
at the temperature of the crankshaft.
- Again install the special crankcase separation
plate NOT installing the crankshaft protection
- During the assembly phase keep the central
thrust screw loose.
- Take the four clamping screws to the end of the
stroke and loosen them again with the same angle
(e.g. 90°)
- When the temperature has settled, preload the
thrust screw of the tool manually until the ball bear-
ing clearance is cancelled out.
Specific tooling
DNA 50 Engine
ENG - 87


 To Next Page