OPERATION
second, making the arc appear constant to the human eye.
Basic MIG Welding
Good weld quality and weld profile depends on gun angle, direction of travel, electrode
extension (stick out), travel speed, thickness of base metal, wire feed speed and arc voltage.
To follow are some basic guides to assist with your setup.
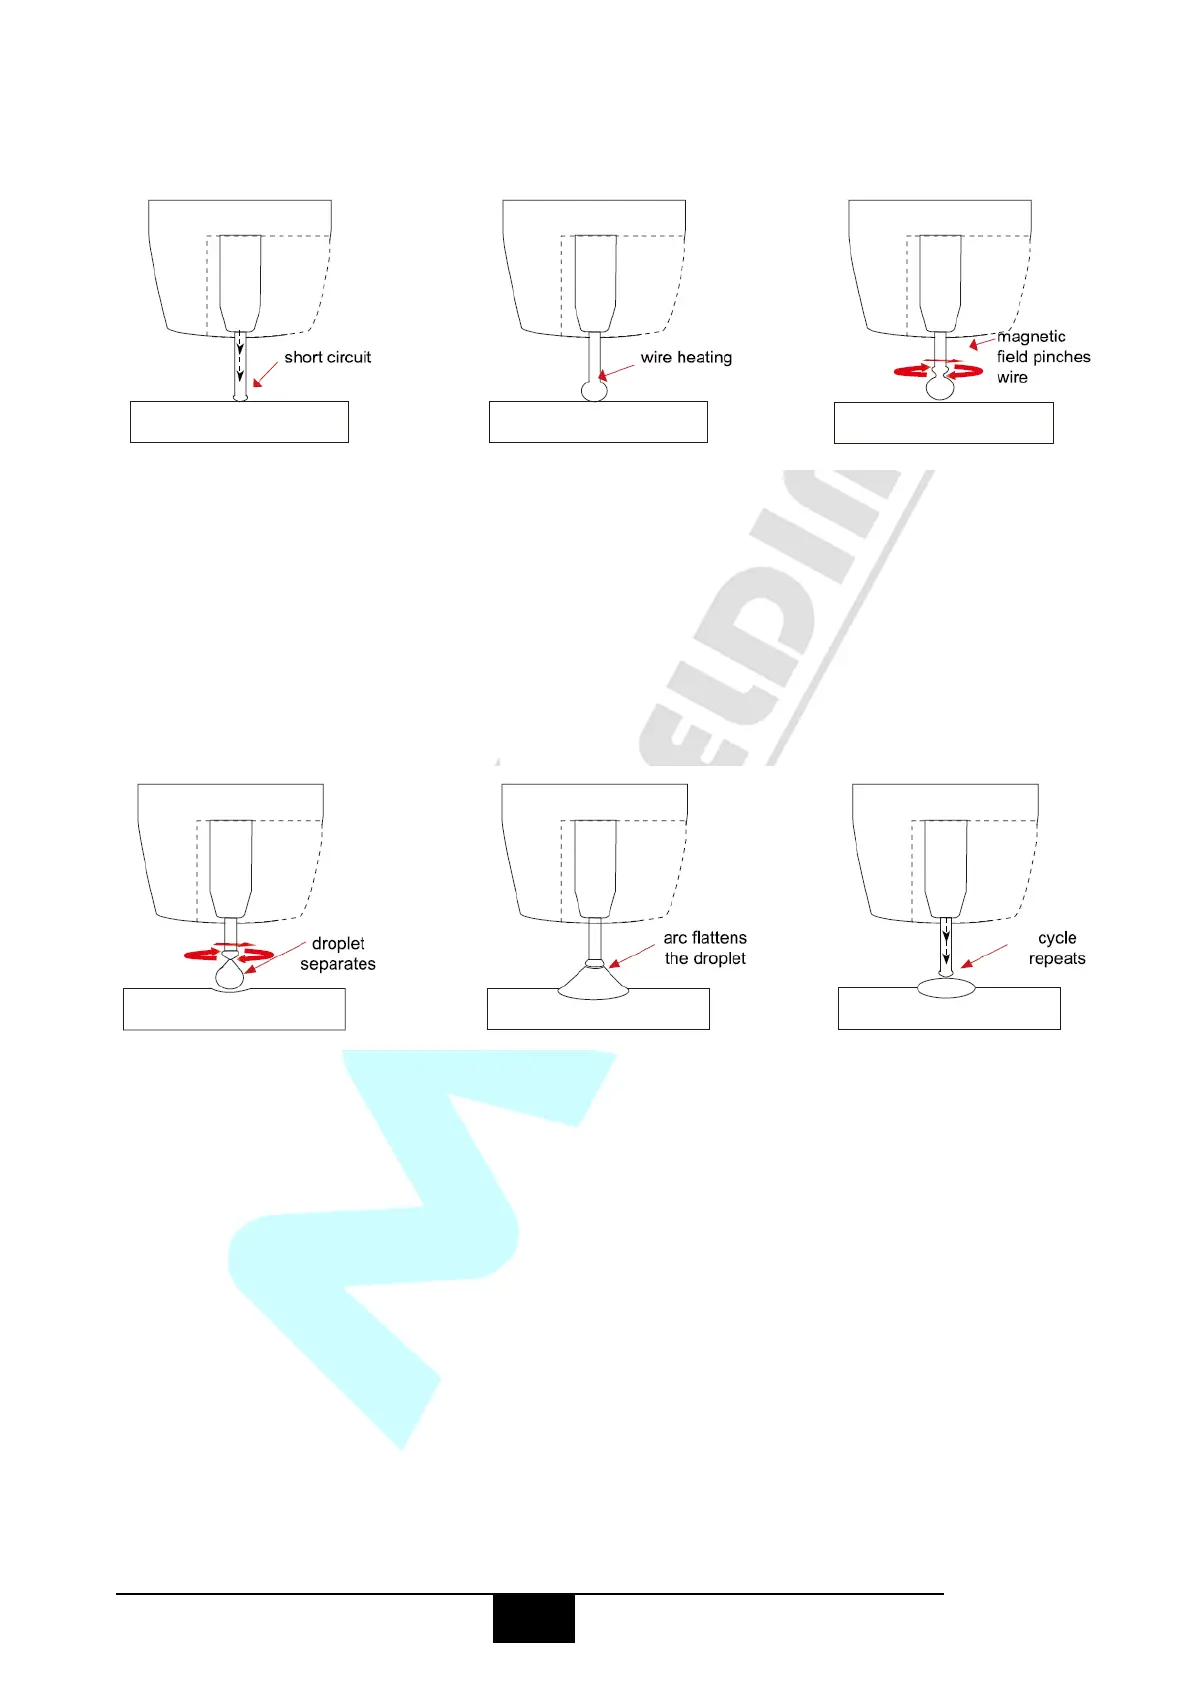
The wire approaches the work
piece and touches the work
creating a short circuit between
the wire and the base metal,
because there is no space
between the wire and the base
metal there is no arc and current
flows through the wire.
The wire cannot support all
the current flow, resistance
builds up and the wire
becomes hot and weak and
The current flow creates a
magnetic field that begins to
pinch the melting wire forming
it into droplet.
The pinch causes the forming
droplet to separate and fall
towards the now creating weld
separation of the droplet and the
heat and force of the arc flattens
out the droplet into the weld
pool. The heat of the arc melts
the end of the wire slightly as it
feeds towards the base metal.
overcomes the heat of the
arc and the wire again
approaches the work to
short circuit and repeat the


 To Next Page