OPERATION
Gun Position - Travel Direction, Work Angle: Gun position or technique usually refers to
how the wire is directed at the base metal, the angle and travel direction chosen. Travel
speed and work angle will determine the characteristic of the weld bead profile and degree
of weld penetration
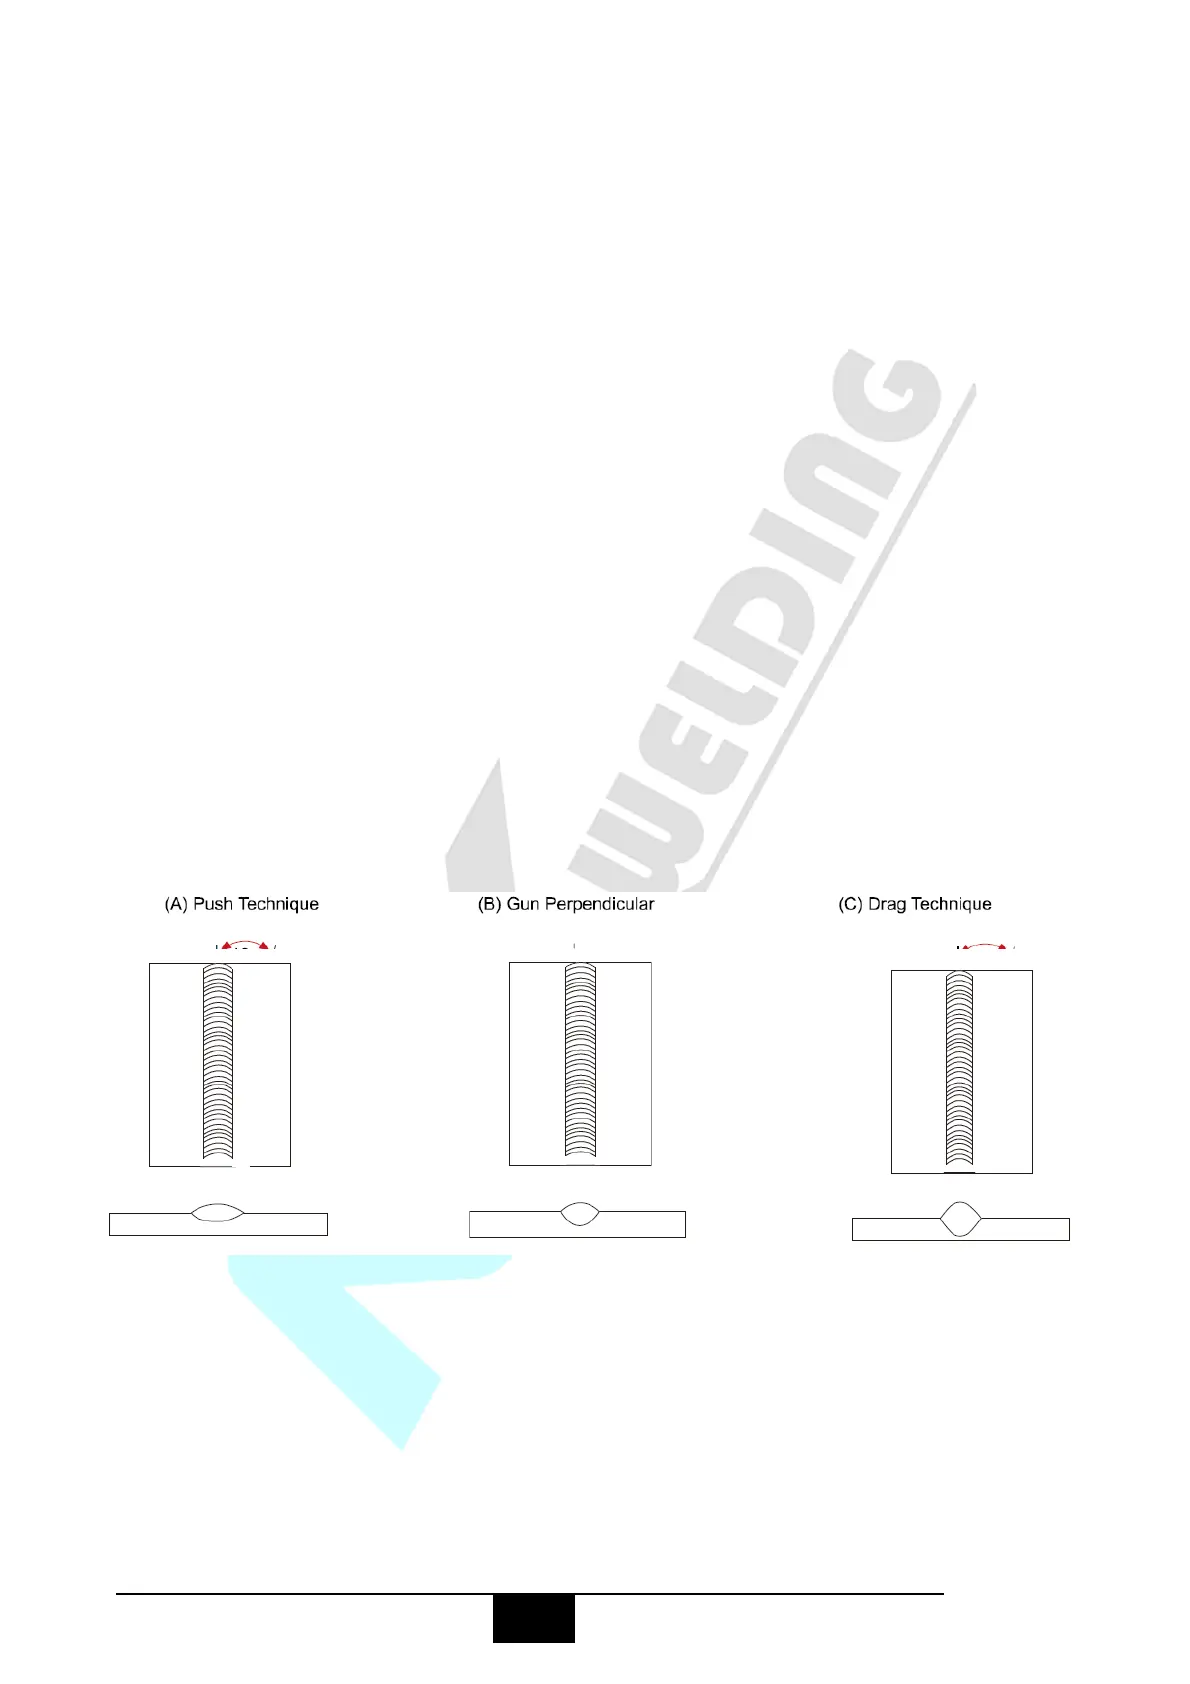
Push Technique - The wire is located at the leading edge of the weld pool and pushed
towards the un-melted work surface. This technique offers a better view of the weld joint and
direction of the wire into the weld joint. Push technique directs the heat away from the weld
puddle allowing faster travel speeds providing a flatter weld profile with light penetration -
useful for welding thin materials. The welds are wider and flatter allowing for minimal clean
up / grinding time.
Perpendicular Technique - The wire is fed directly into the weld, this technique is used
primarly for automated situations or when conditions make it necessary. The weld profile is
generally higher and a deeper penetration is achieved.
Drag Technique - The gun and wire is dragged away from the weld bead. The arc and heat
is concentrated on the weld pool, the base metal receives more heat, deeper melting, more
penetration and the weld profile is higher with more build up.
Travel Angle - Travel angle is the right to left angle relative to the direction of welding. A
travel angle of 5°- 15° is ideal and produces a good level of control over the weld pool. A
travel angle greater that 20° will give an unstable arc condition with poor weld metal transfer,
flat even weld
profile light
penetration
narrower weld profile
even penetration
narrow higher
weld profile more
penetration


 To Next Page