OPERATION
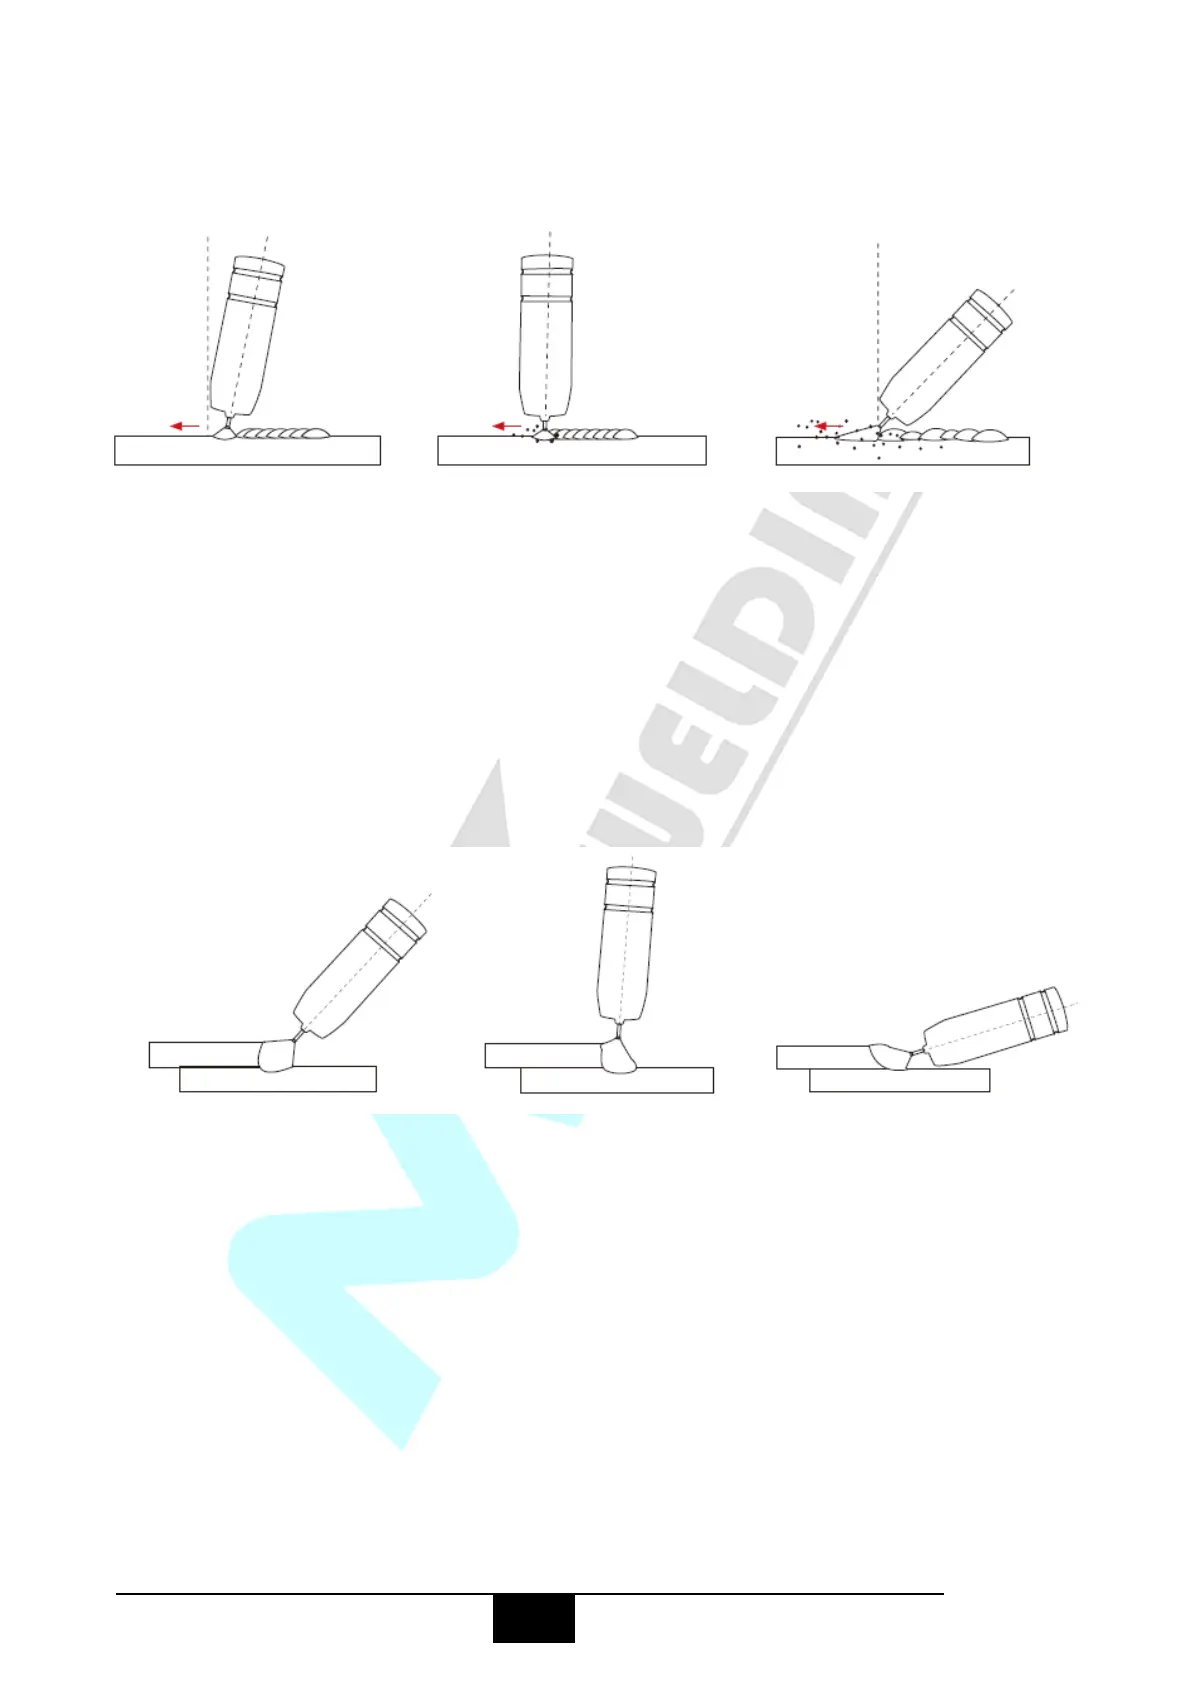
less penetration, high levels of spatter, poor gas shield and poor quality finished weld.
Angle to Work - The work angle is the forward back angle of the gun relative to the work
piece. The correct work angle provides good bead shape, prevents undercut, uneven
penetration, poor gas shield and poor quality finished weld.
Stick Out- Stick out is the length of the unmelted wire protruding from the end of the contact
tip. A constant even stick out of 5-10mm will produce a stable arc, and an even current flow
providing good penetration and even fusion. Too short stick out will cause an unstable weld
pool, produce spatter and over heat the contact tip. Too long stick out will cause an unstable
arc, lack of penetration, lack of fusion and increase spatter.
good level of control over
the weld pool, even flat
less control over the weld
pool more spatter.
poor control, unstable arc,
less penetration, lots of
good level of control
over the weld pool,
even flat weld.
less control over the weld
pool more spatter.
poor control, unstable arc,
less penetration, lots of
spatter.


 To Next Page