OPERATION
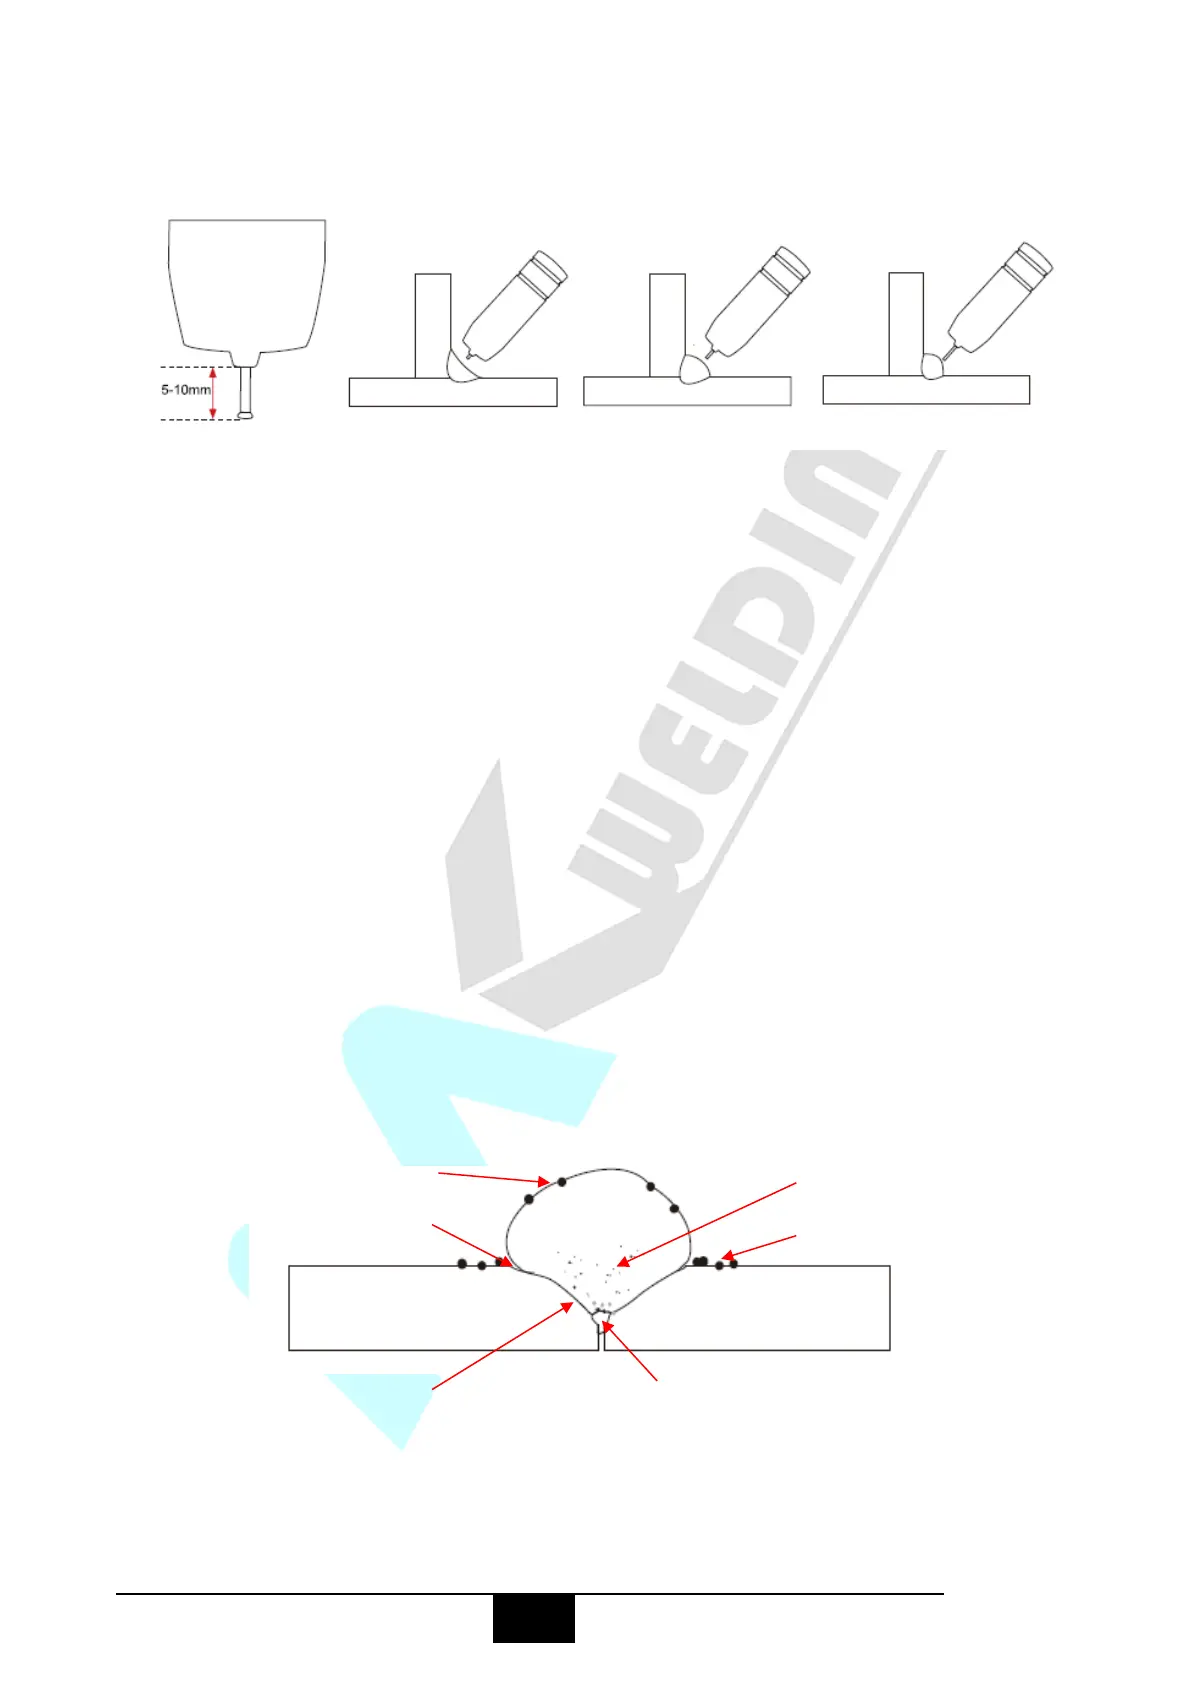
Travel Speed - Travel speed is the rate that the gun is moved along the weld joint and is
usually measured in mm per minute. Travel speeds can vary depending on conditions and
the welders skill and is limited to the welders ability to control the weld pool. Push technique
allows faster travel speeds than Drag technique. Gas flow must also correspond with the
travel speed, increasing with faster travel speed and decreasing with slower speed. Travel
speed needs to match the amperage and will decrease as the material thickness and
amperage increase.
Too Fast Travel Speed - A too fast travel speed produces too little heat per mm of travel
resulting in less penetration and reduced weld fusion, the weld bead solidifies very quickly
trapping gases inside the weld metal causing porosity. Undercutting of the base metal can
also occur and an unfilled groove in the base metal is created when the travel speed is too
fast to allow molten metal to flow into the weld crater created by the arc heat.
Too Slow Travel Speed - A too slow travel speed produces a large weld with lack of
penetration and fusion. The energy from the arc dwells on top of the weld pool rather than
penetration even
Unstable arc, spatter,
over heat contact tip.
poor penetration and
lack of joint penetration


 To Next Page