OPERATION
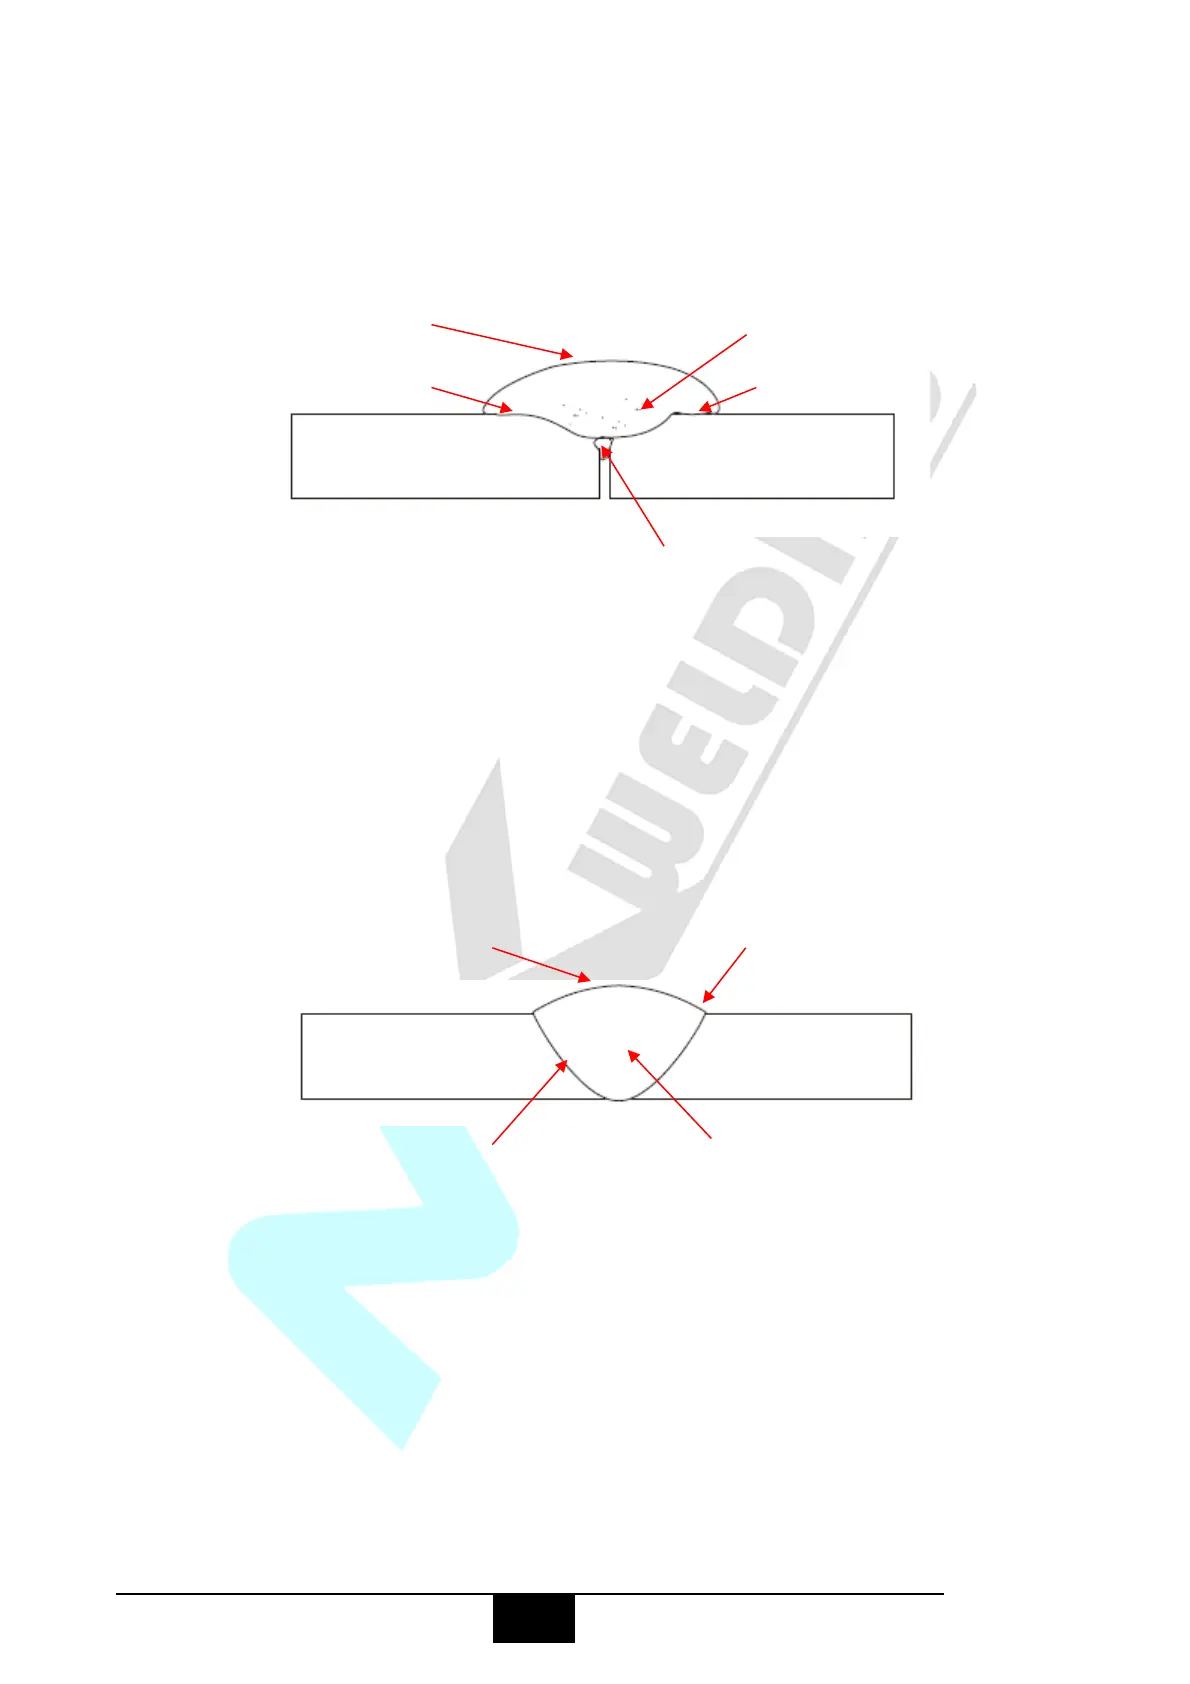
lack of joint penetration
penetrating the base metal. This produces a wider weld bead with more deposited weld
metal per mm than is required resulting in a weld deposit of poor quality.
Correct Travel Speed - The correct travel speed keeps the arc at the leading edge of the
weld pool allowing the base metal to melt sufficiently to create good penetration, fusion and
wetting out of the weld pool producing a weld deposit of good quality.
Wire types and sizes - Use the correct wire type for the base metal being welded. Use
stainless steel wire for stainless steel, aluminium wires for aluminium and steel wires for
steel.
Use a smaller diameter wire for thin base metals. For thicker materials use a larger wire
diameter and larger machine, check the recommended welding capability of you machine.
As a guide refer to the “Welding Wire Thickness Chart” below.


 To Next Page