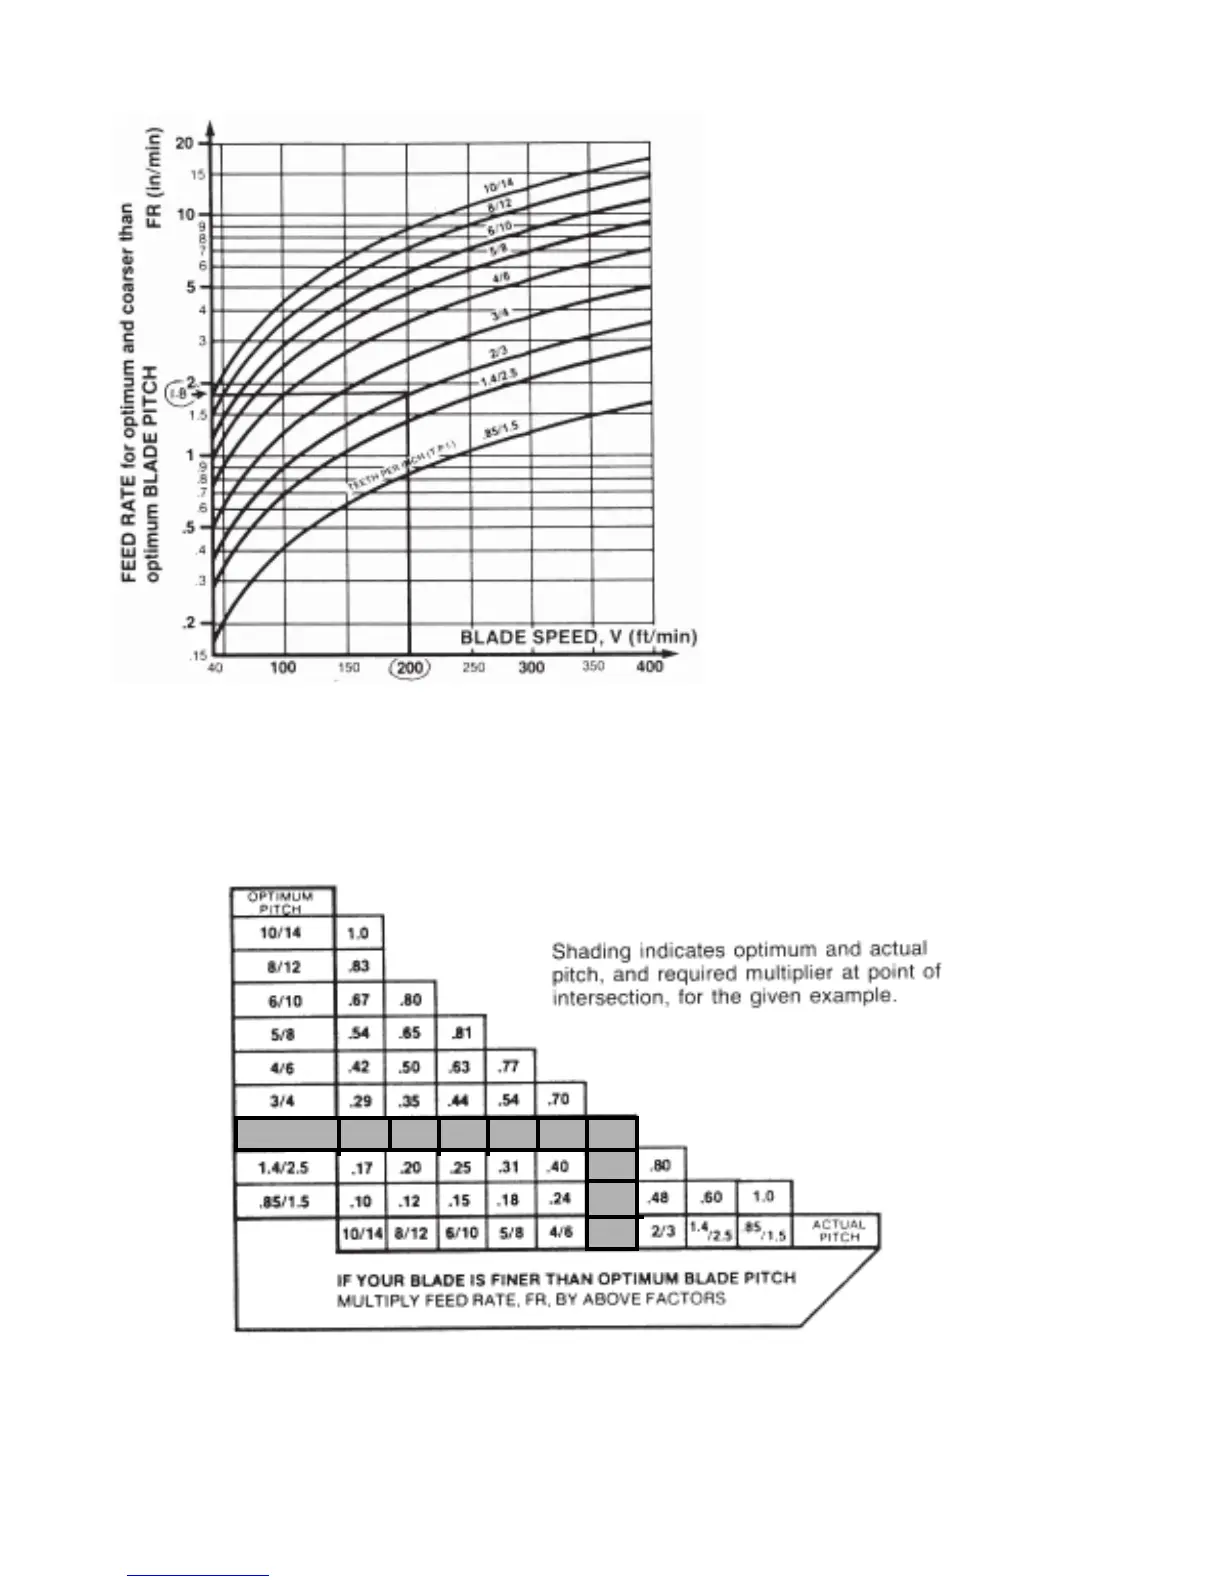
Fig. 2B-10
If the machine is fitted with a blade coarser than optimum (eg. 1.4/2.5 TPI) we can still use the graph, but we go
to the 1.4/2.5 curve. As a result we find that the FEED RATE is decresed to 1.3 in/min for this blade.
If however, the machine is fitted with a finer than optimum blade (eg. 3/4 TPI) we use the graph for the optimum
blade as before, and then use a multiplier given by the table 2B-2.
2.19
As a result we find that we must decrease our FEED RATE of 1.8 in/min by a factor of .71. In this case we
should use FEED RATE of 1.8 in/min x .71 = 1.3 in/min.
TABLE 2B-2
3/4
.34
.57
2/3 .21 .25 .31 .50.38 .71
- Find the point where a vertical line
from 200 ft/min would intersect the
` For Example #1, it is known from Step
3 that otimum blade pitch is 2/3, and
from Step 4 that blade speed ,200 ft/
min. From the graph, Fig. 2B-10 the
FEED RATE is determined in the
following way:
- On the horizontal axis (blade speed
axis), find 200 ft/min.
2/3 blade pitch curve.
- From this intersection point run
horizontally left to the vertical (FEED
RATE) axis, to arrive at 1.8 in/min
FEED RATE. Thus 1.8 in/min is the
FEED RATE for cutting 8" diameter,
1045 Carbon Steel when the optimum
2/3 pitch blade is used.








 To Next Page