êëìí î
ìí
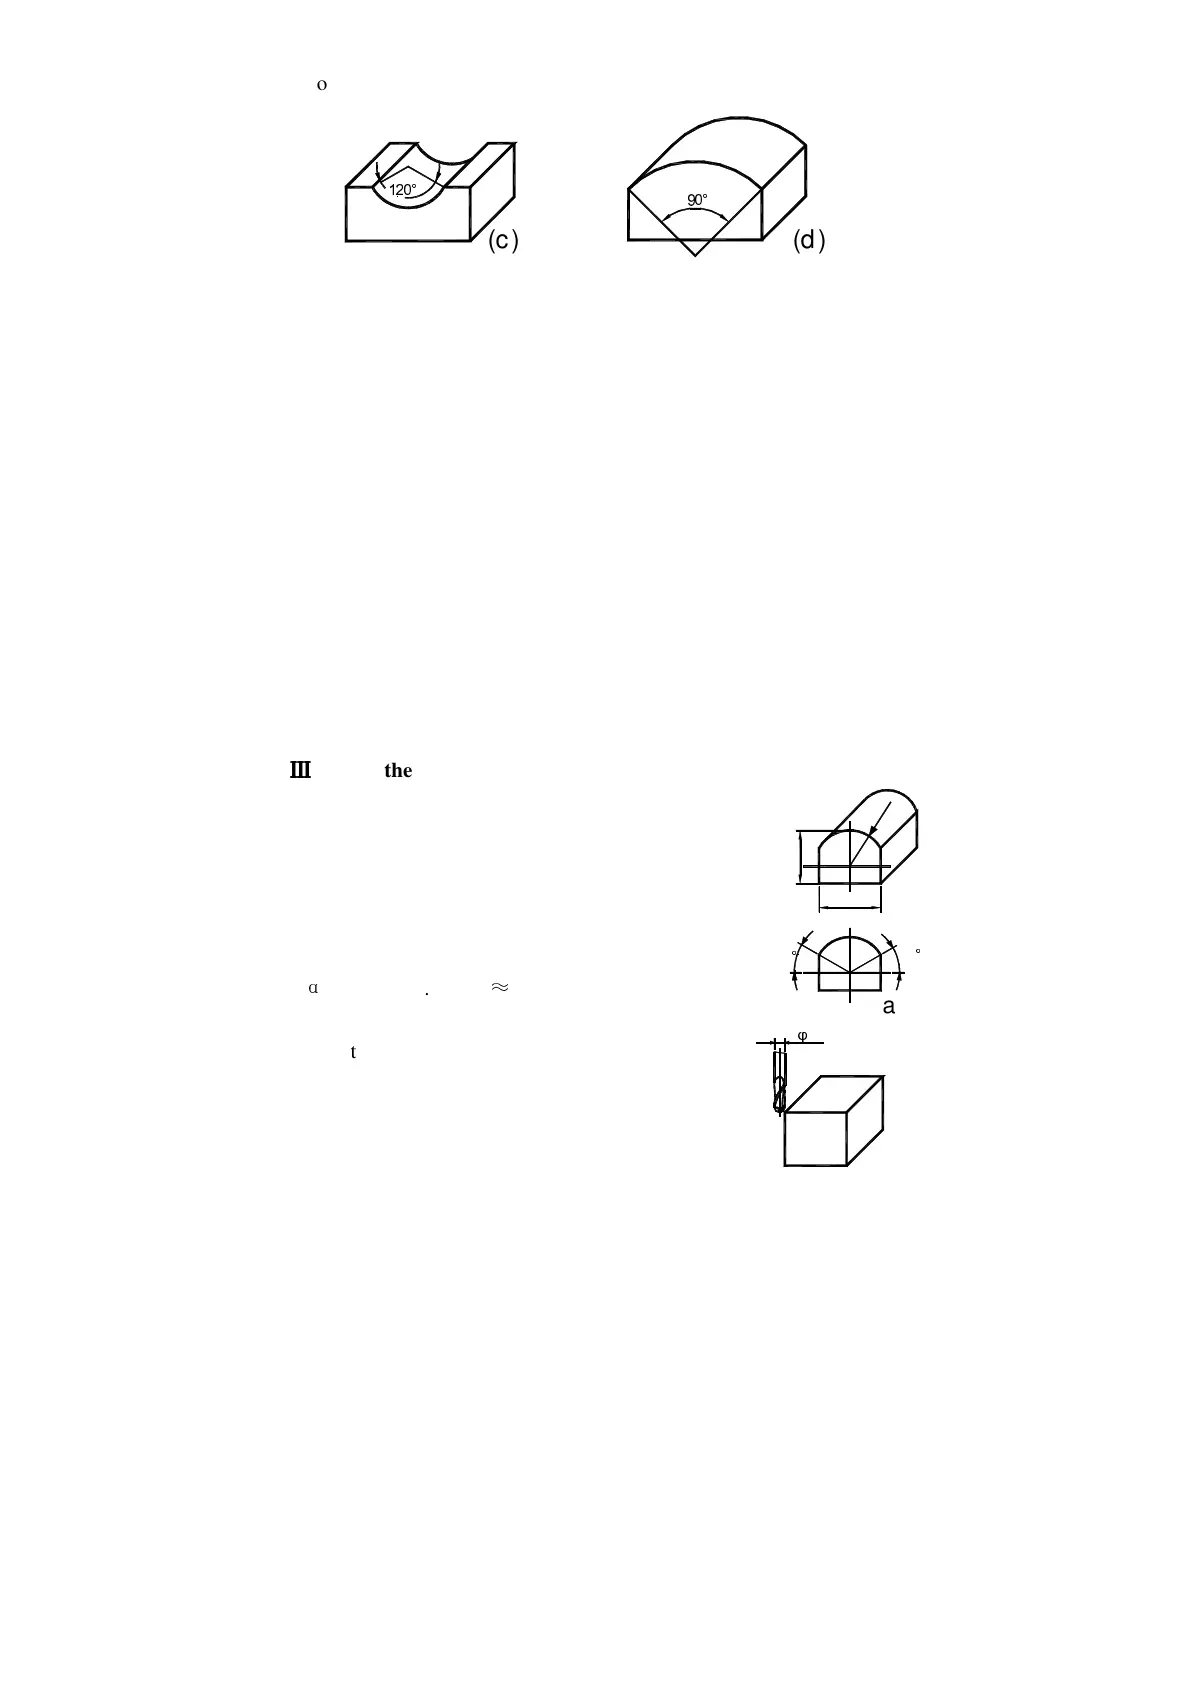
(c) (d)
on the both axes into zero and reach the position of the corresponding
point of the R circular arc.
Note: When the arc to be processed in Planes XZ and YZ covers the 90° or the
270° position, for example, the one from 210° to 330° covers 270° in
Fig.(c), and the other from 135° to 45° covers 90° in Fig. (d),end mill
shall not be used.
Note: When Model SDS2-2 digital display box is used to realize the arc R
processing in Planes XZ and YZ, it is necessary to make use of the
method of emulation. When emulation processing is used, the
position of each processing point on Z axis will be displayed on the
message window and the feeding value of every step will be
displayed on the unused X-/Y-axis. The operator can take the
displayed value as reference, and what should do is only turning the
Z axis star wheel to let the machine rise up or drop down a value
equal the displayed value. (Let the machine table drop down when
the displayed value on Z axis is positive, and let it rise up when the
value is negative).
(
ï
ïï
ï
) *Take the processing of the working piece shown in the figure on the
right as the third example (Example 3):
1. For the processing of this working piece, it is
necessary to calculate out the start and end angles
of the arc at first.
Refer to the figure.
ð
=arc cos(17.3/2)/10
ñ
30°
The start angle (ST ANG)of the arc is 30°,
and the end angle (ED ANG) is 150°.
30
ò
1
5
17.3
R
1
0
30
ó
5
(a)
(b)


 To Next Page