4200T CNC Programming and Operations Manual
P/N 70000412F - Canned Cycles
All rights reserved. Subject to change without notice. 5-15
31-July-05
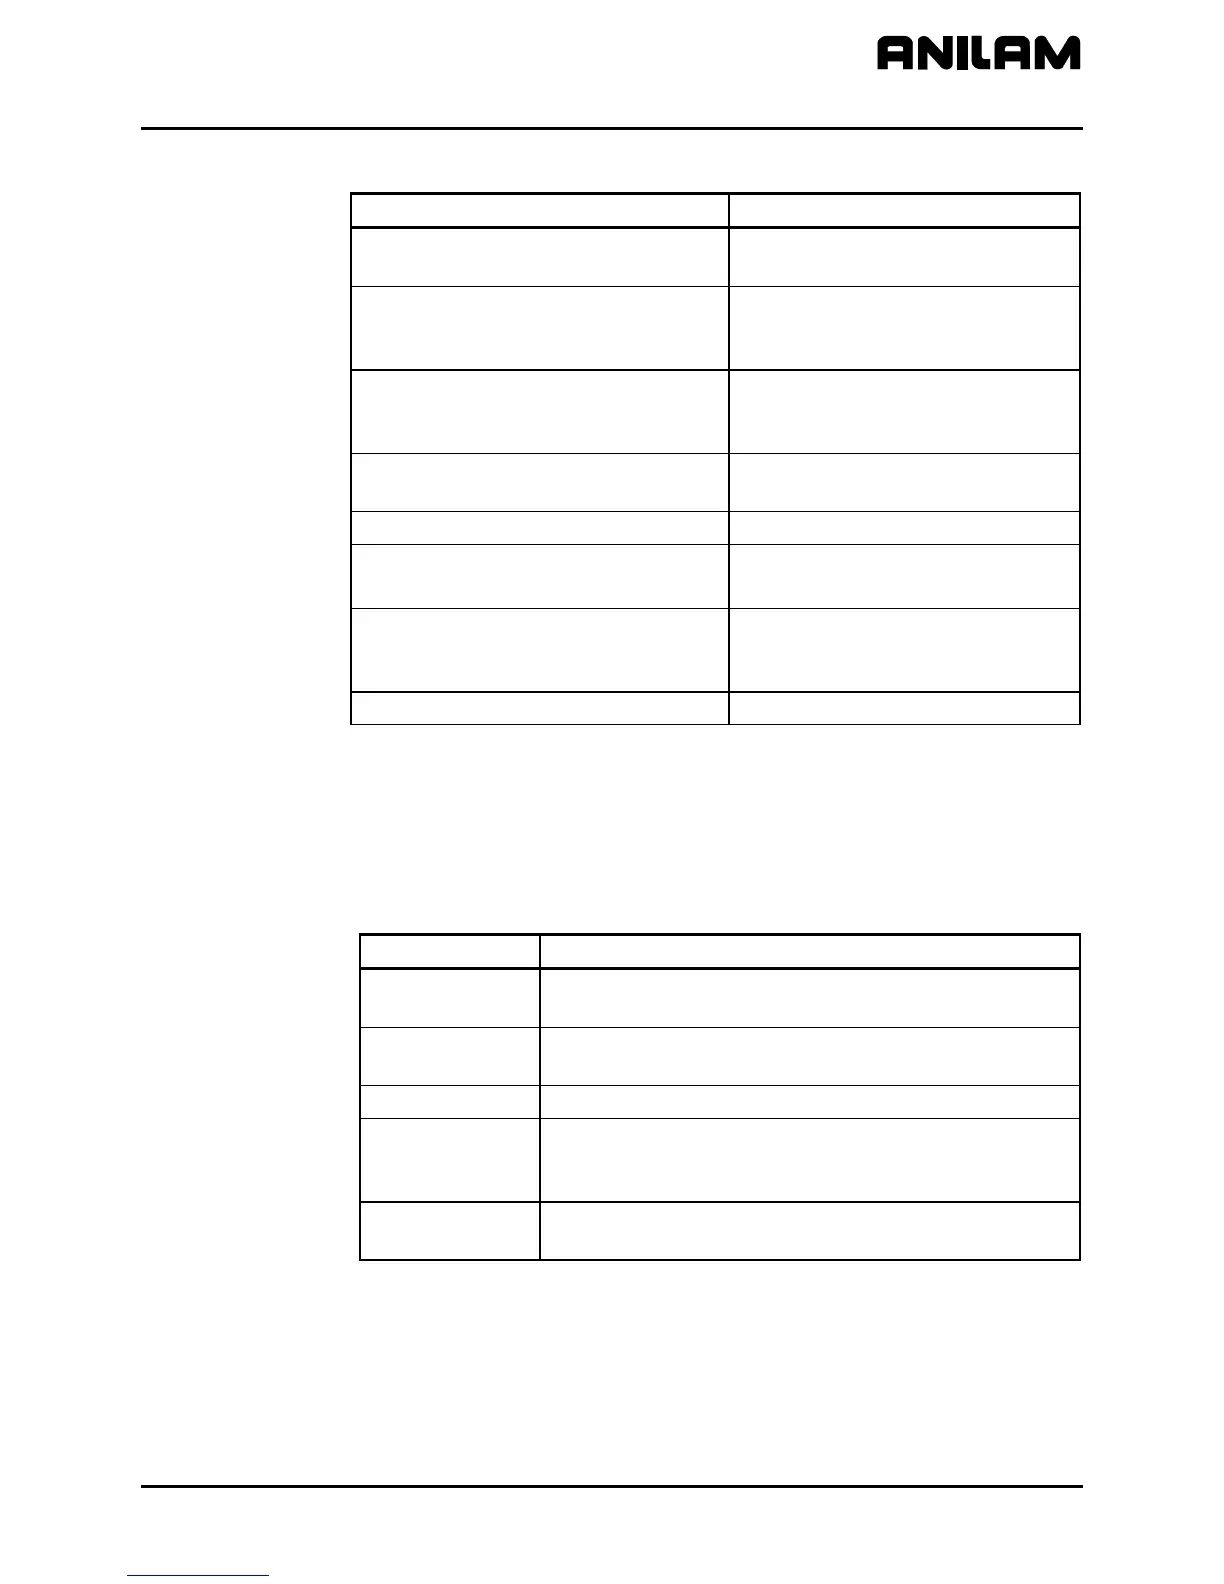
Table 5-9, G81 Programming Example
Program Block Description
N1 O7 *GROOVY Establishes program name and
number.
N2 G90 G70 G0 T0 X0 Z0 M5 Sets Absolute/Inch/Rapid Modes.
Cancels tool offsets and positions
tool at X0, Z0.
N3 T1 *.125 (3.175) WIDE
GROOVE INSERT
Activates tool length offsets for
Tool 1. Contains a comment
regarding tool width.
N4 X1.2 (30.48) Z-.725 (-18.415)
M3 S980
Positions axes, turns on spindle
and sets spindle speed to 980.
N5 G95 F.0012 (.03) Sets feedrate.
N6 G81 Z-.75 (-19.05) X-.0625
(-1.588) W.125 (3.175) B.1(2)
Defines and activates G81 canned
cycle.
N7 G0 T0 X0 Z0 M5 Cancels tool offset, positions
axes at Machine Home and turns
off the spindle.
N8 M2 End of program. Return to N1.
Programming a Radial Grooving Cycle (G82)
Format G82 Zn Xn Wn Bn Dn
Refer to Table 5-10 for a list and description of the Address Words used
to define a Radial Grooving Cycle (G82).
Table 5-10, G82 Address Words
Address Word Description
X
Incremental X distance (length) from start radius to
end radius (excludes B). Required.
Z
Total incremental Z dimension of groove (depth).
Required.
W
Tool width. Required.
B
Incremental X standoff distance from diameter (0.1
in/2mm outer diameter; -0.1in/2mm inner diameter).
Optional.
D
Dwell time at bottom of groove, in seconds.
Optional.


 To Next Page