-- 4 2 --
fzb2d3ea
12.3 POWER SOURCE MENU
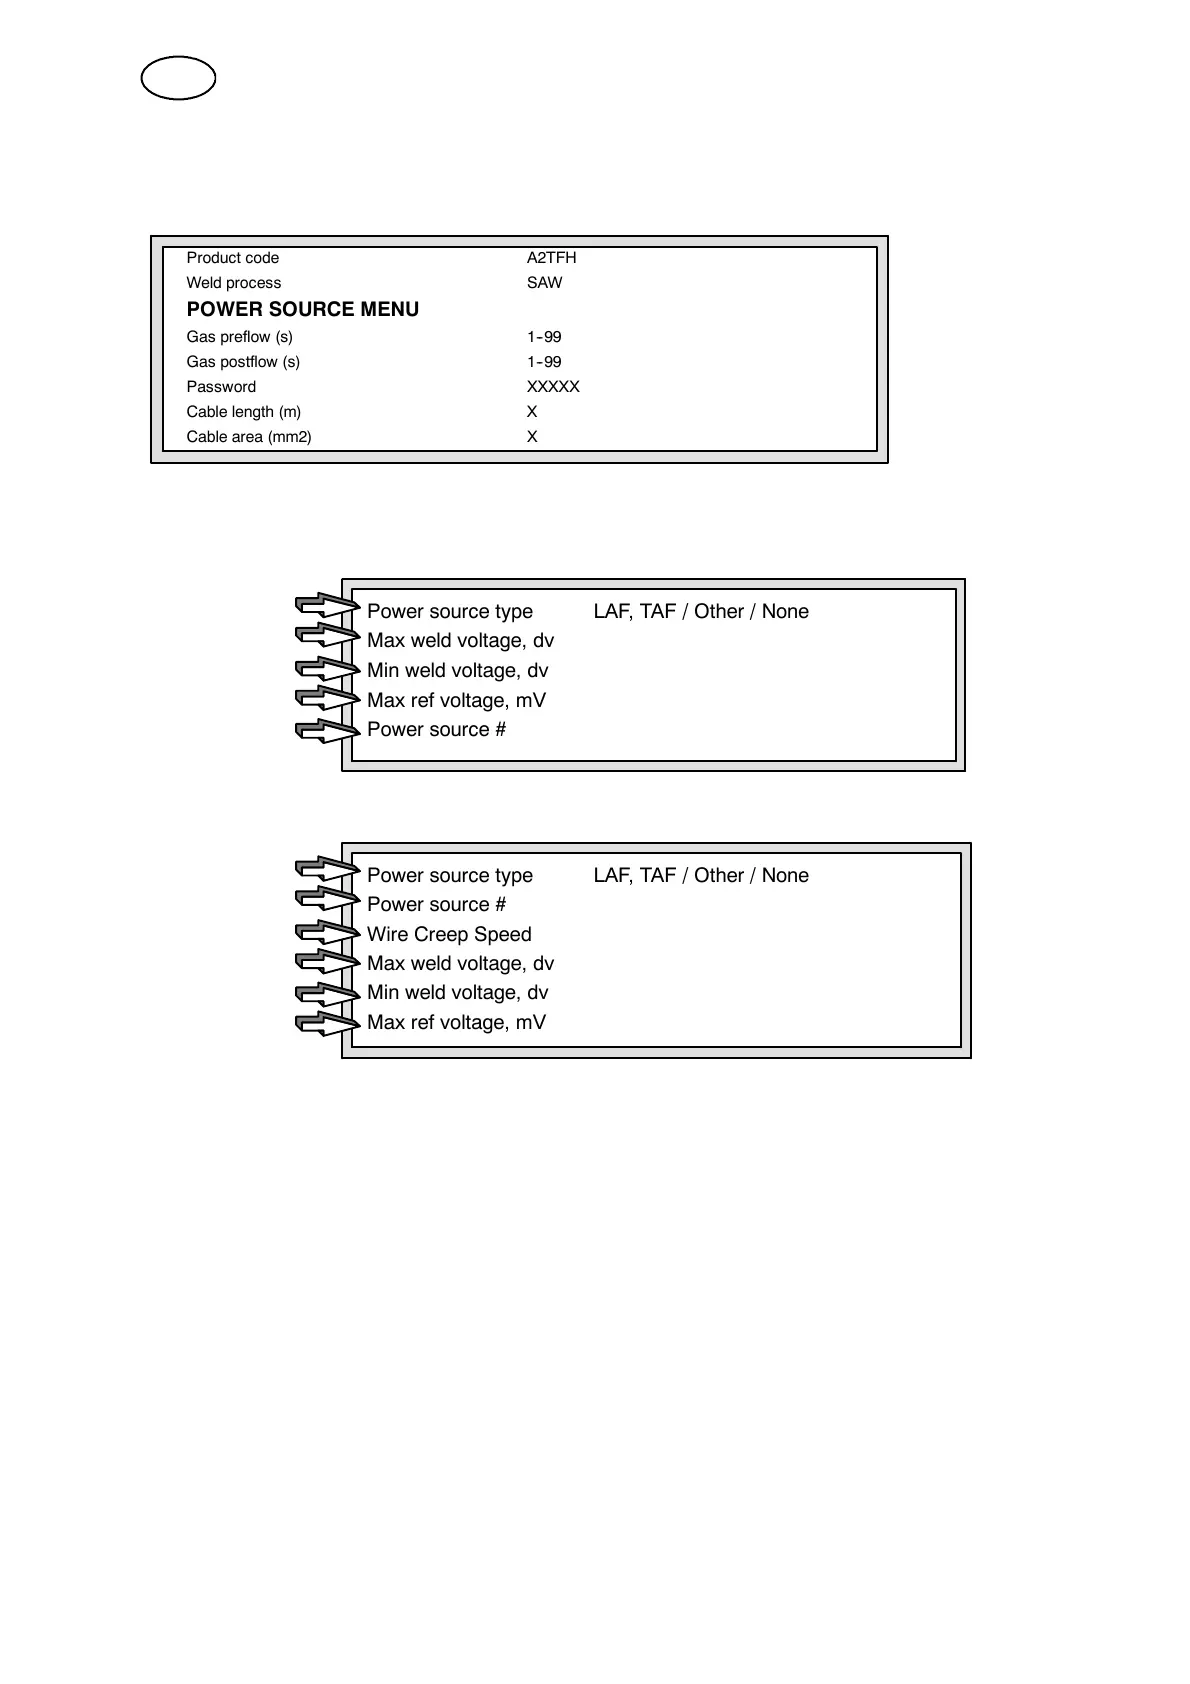
This menu is used for configuration of the welding power source.
Product code A2TFH
Weld process SAW
POWER SOURCE MENU
Gas preflow (s) 1--99
Gas postflow (s) 1--99
Password XXXXX
Cable length (m) X
Cablearea(mm2) X
The following menu is shown when POWER SOURCE MENU has been selected:
For program version 4.0 and 4.01:
Power source type LAF, TAF / Other / None
Max weld voltage, dv
Min weld voltage, dv
Max ref voltage, mV
Power source #
See on page 42
See on page 43
See on page 43
See on page 43
See on page 44
For program version 4.2, 4.3 and 5.0:
Power source type LAF, TAF / Other / None
Power source #
Wire Creep Speed
Max weld voltage, dv
Min weld voltage, dv
Max ref voltage, mV
See on page 42
See on page 43
See on page 43
See on page 44
See on page 43
See on page 43
1. Power source type:
LAF, TAF -- Welding power sources that are specially adapted to work with the
A2--A6 Process Controller.
Other -- Welding power source other than LAF/TAF, that is used together
with an analogue PCB card to get a voltage reference and
start/stop signal.
If Other has been selected it’s only possible to weld with a constant
wire feed speed (CW),
N.B This alternative is not available in the Chinese version.
None -- Control box PEH is used only to steer the travel direction.
GB


 To Next Page