2.24
COOLANT FLOW
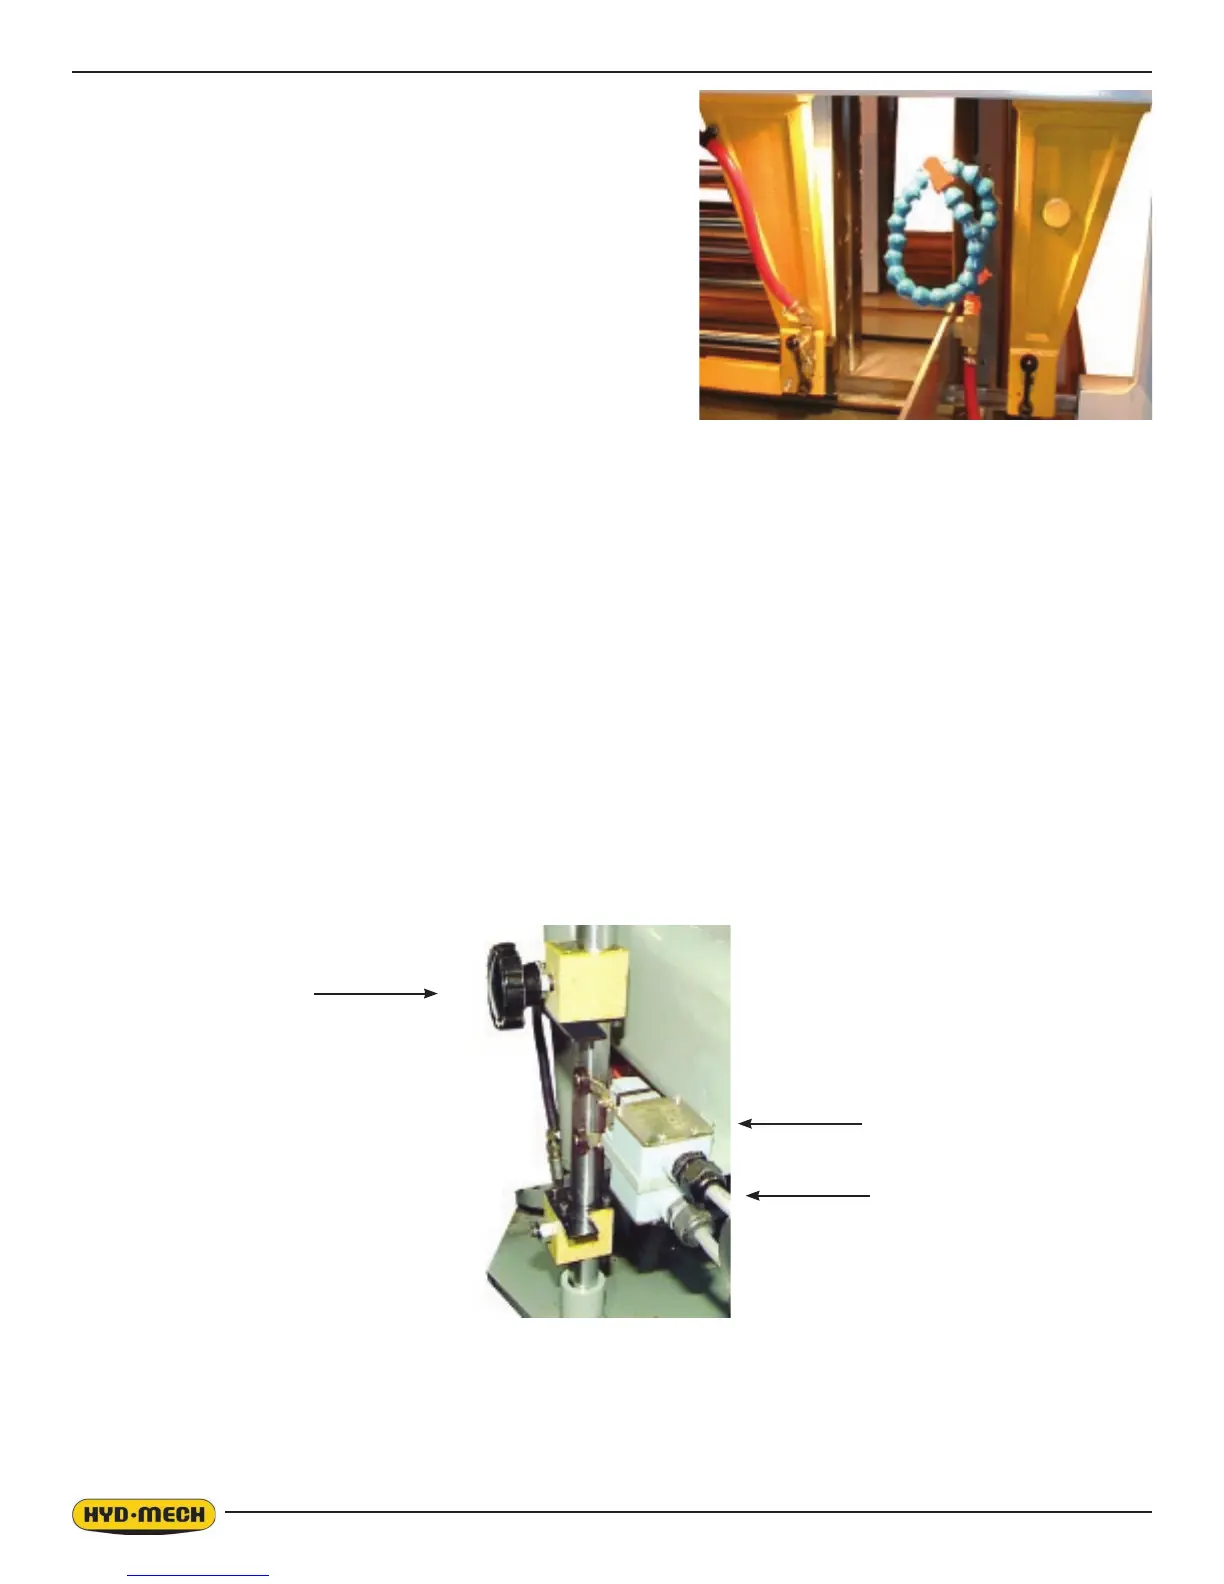
A generous ow of coolant should be applied in order to increase
production and blade life. The machine is provided with a switch on
the control panel as well as two independently controlled coolant
spouts. One is on the adjustable guide arm, this one should always
ood the blade with coolant. Slight adjustment may be required
when changing the blade speed. A properly adjusted ow of coolant
should cover the blade which in turn will carry it into the cutting area.
The ow adjusting tap is shown below. The second is mounted on
the fence for the coolant hose which should be used in cases when
cutting solid bars, bundles or wide structurals. The ow of coolant
should be directed into the opening created by the blade.
NOTE: When cutting materials that do not need coolant (cast iron)
some coolant ow is required to provide blade lubrication to prevent
blade scoring by carbides
Coolant ow adjusting taps
HEAD UP AND DOWN LIMIT SETTING
Head Up Limit: In order to maximize production in the automatic cycle the Head Up Limit should be set to just clear the
height of the material.
Head Down Limit: This limit is factory set and under ordinary cutting requirements should not be changed. If changed, it
may cause the machine to malfunction in the automatic cycle.
Adjusting Block and Knob
Head Up Limit Switch
Head Down Limit Switch
Head up and head down limit setting.



 To Next Page