OPTIMUM
MASCHINEN - GERMANY
Version 1.0.1 dated 2018-01-31 Page 47Translation of the original instructions
TM4010 | TM4010D GB
TM4010_TM4010D_GB_4.fm
4.15.6 Thread cutting
The thread cutting process requires that the operator has a good knowledge of turning and suf-
ficient experience.
NOTES!
Example of an external thread:
The workpiece diameter must have been turned to the diameter of the desired thread.
The workpiece requires a chamfer at the beginning of the thread and an undercut at the
thread run out.
The speed must be as low as possible.
The thread cutting tool must be exactly the same shape as the thread, it must be absolutely
rectangular and must be clamped in a way that it coincides exactly with the turning centre.
The threading engaging lever must be engaged during the whole thread cutting process.
This does not apply to thread pitches that can be carried out with the thread gauge.
The thread is produced in various cutting steps in a way that the cutting tool has to be
turned out of the thread completely (with the cross slide) at the end of each cutting step.
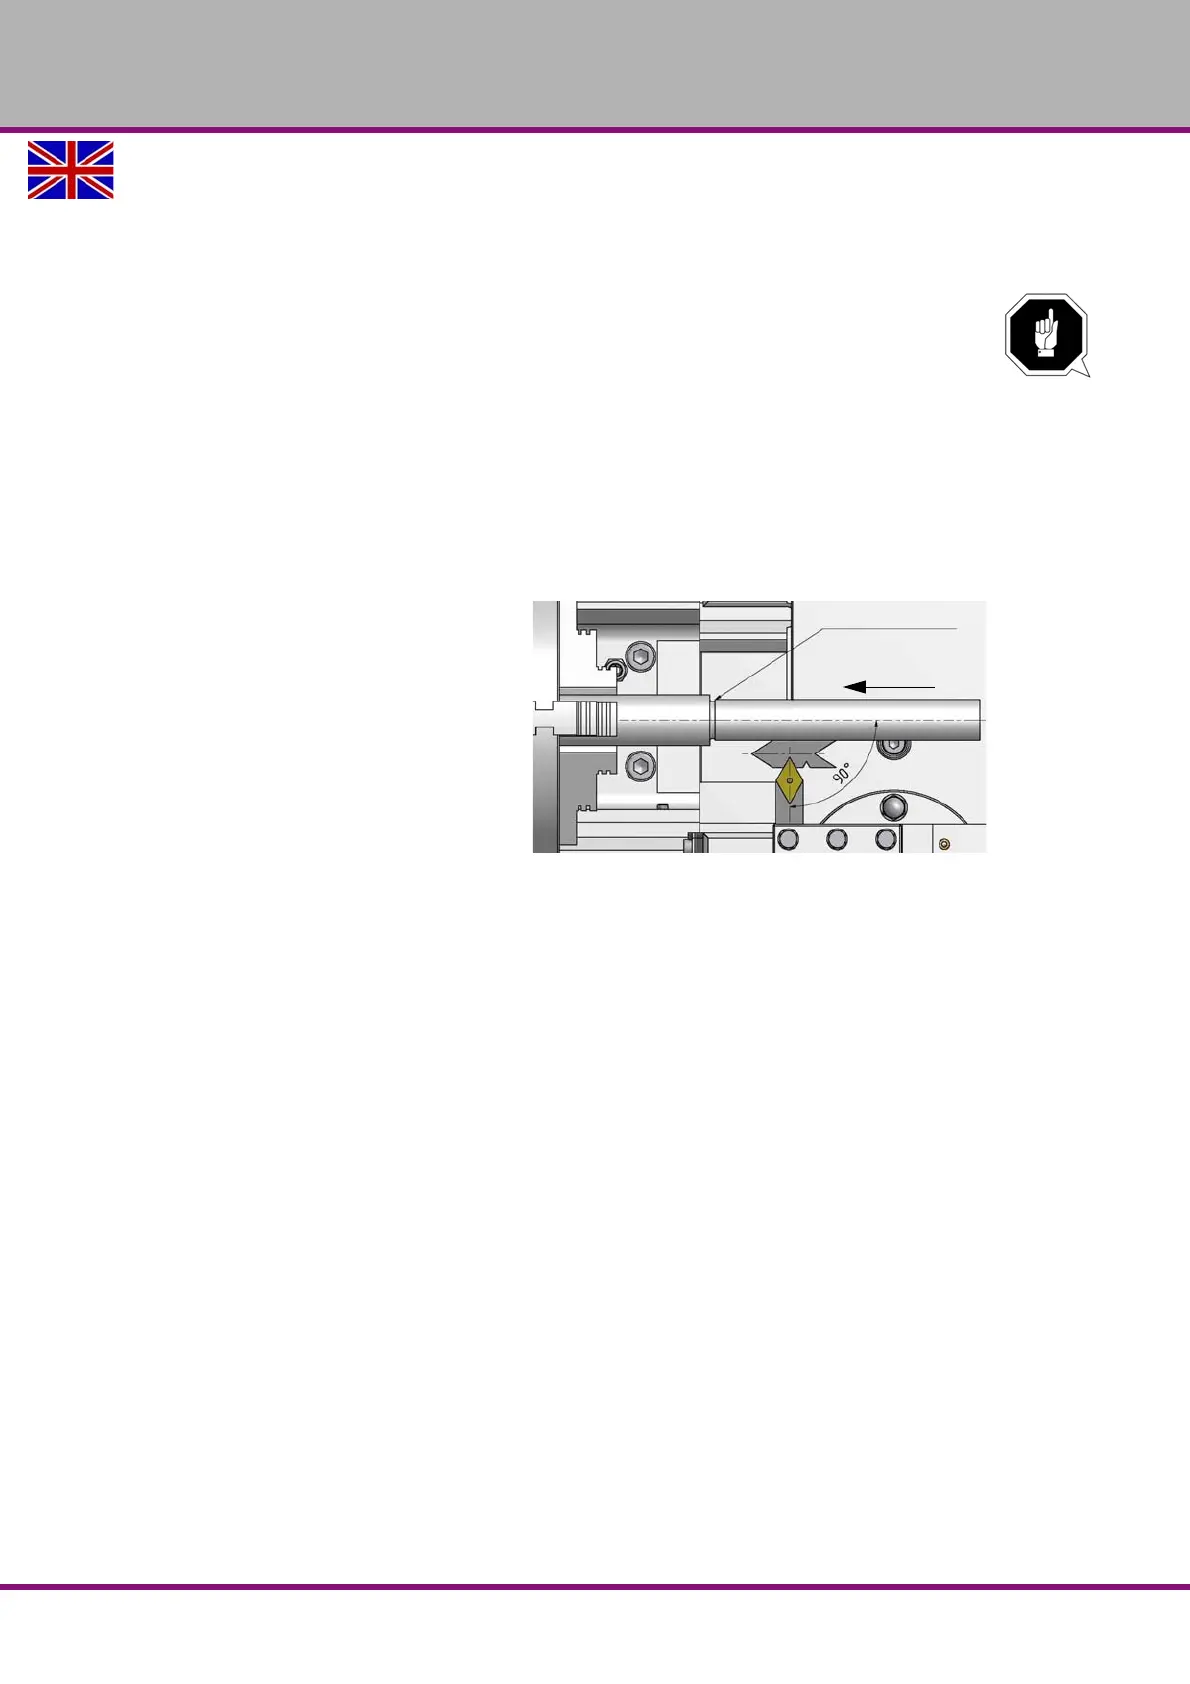
The tool is withdrawn with the lead
screw nut engaged and the thread cut-
ting tool disengaged by actuating the
"Direction of rotation control lever".
Stop the lathe and feed the thread cut-
ting tool in low cut depths using the
cross slide.
Img.4-13: Illustration: Thread cutting
Before each passage, place the top slide approximately 0.2 to 0.3 mm to the left and right
alternately in order to cut the thread free. In this way, the thread cutting tool cuts only on
one thread flank with each passage. Do not execute any more free cutting, just before
reaching the full thread depth.


 To Next Page