Functional characteristics
MIG/MAG welding
099-5TLPXQ-EW501
29.01.2021
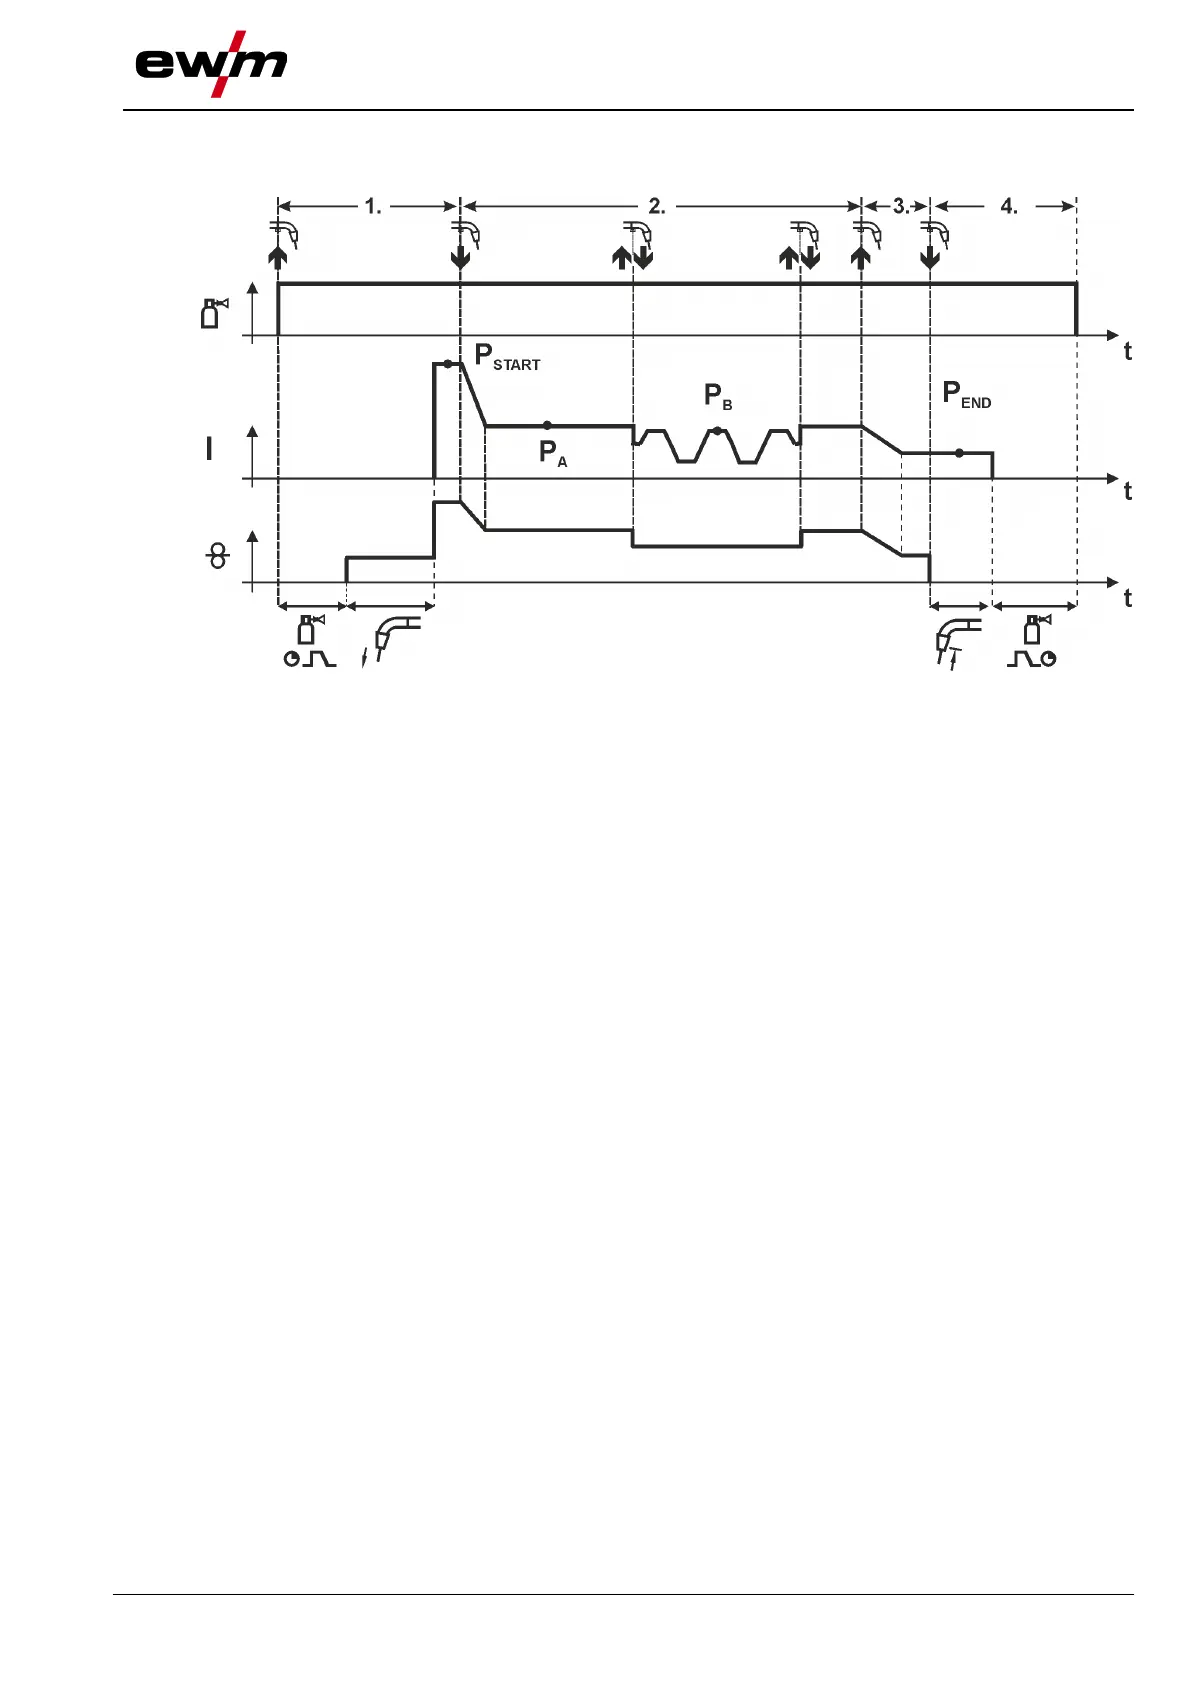
Special latched with changing welding method by tapping (process switching)
To activate or set the function > see 5.2.9 chapter.
Figure 5-23
1st cycle
• Press and hold torch trigger.
• Shielding gas is expelled (gas pre-flows)
• Wire feed motor runs at "creep speed"
• Arc ignites after the wire electrode makes contact with the workpiece, welding current is flowing (start
program P
START
)
2nd cycle
• Release torch trigger
• Slope on main program P
A
The slope on main program P
A
is given at the earliest after the set time t
START
elapses and at the
latest when the torch trigger is released.
Tapping (pressing the torch trigger for less than 0.3 sec.) changes over the welding process (P
B
).
If a standard process has been defined in the main program, tapping changes to the pulse
process, and tapping again will return to the standard process, etc.
3
rd
cycle
• Press and hold torch trigger
• Slope to end program P
END
4th cycle
• Release torch trigger
• WF motor stops
• Arc is extinguished after the pre-selected wire burn-back time elapses
• Gas post-flow time elapses
This function can be activated using the PC300.NET software.
Refer to the software operating instructions.


 To Next Page