. A complete Parts List is available at www.MillerWelds.com
OM-281426 Page 39
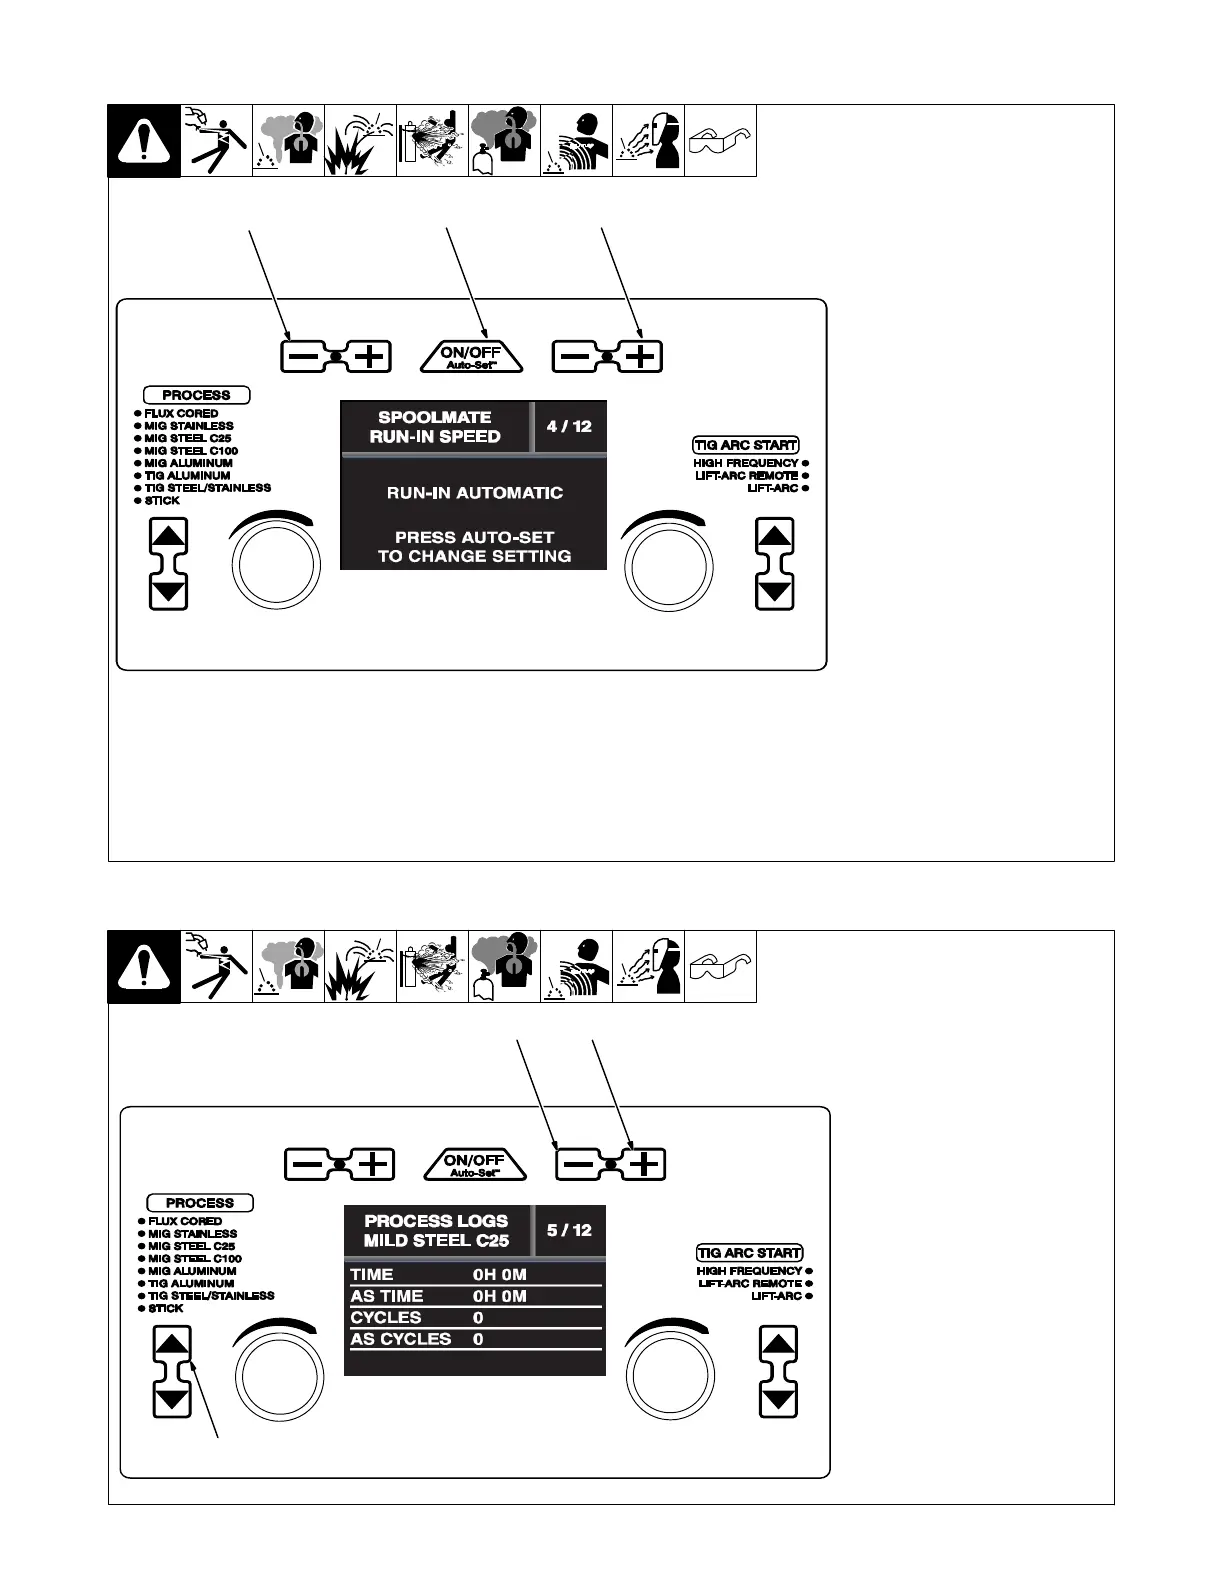
6-12. Spoolmate Run-In Speed (Menu 4 Of 12)
1 Wire/Rod/Tungsten Minus (−)
Button
2 Auto-Set Button
3 Material Thickness Plus (+)
Button
Follow instructions in Section 6-8 to
enter the setup menu.
To change the run−in setting, press
the Auto−Set button.
Run−in is the speed of the wire prior
to the welding arc being struck.
When set to Automatic, the welder
determines the optimal run−in
speed for each start.
When set to Disabled, the run−in
speed is the same as the weld wire
speed.
To exit menu, simultaneously press
and release the Wire/Rod/Tung-
sten Minus (−) button and Material
Thickness Plus (+) button, or turn
unit off and on.
Ref. 281252A
1
23
6-13. Process Logs (Menu 5 Of 12)
1 Material Thickness Minus (−)
Button
2 Material Thickness Plus (+)
Button
3 Process Select
Follow instructions in Section 6-8 to
enter the setup menu.
Process Logs menu displays man-
ual time, Auto−Set time, weld cy-
cles, and Auto−Set cycles for the
selected process.
To view other processes, use the
Process Select buttons to select
the desired weld process.
To exit menu, simultaneously press
and release the Wire/Rod/Tung-
sten Minus (−) button and Material
Thickness Plus (+) button, or turn
unit off and on.
Ref. 281252A
12
3



 To Next Page