OPTIMUM
MASCHINEN - GERMANY
808D
Page 141
ISO Mode
Brief instruction 808D Milling
Operating and Programming — Milling
Basic Theory
Brief description of typical, frequently used ISO codes
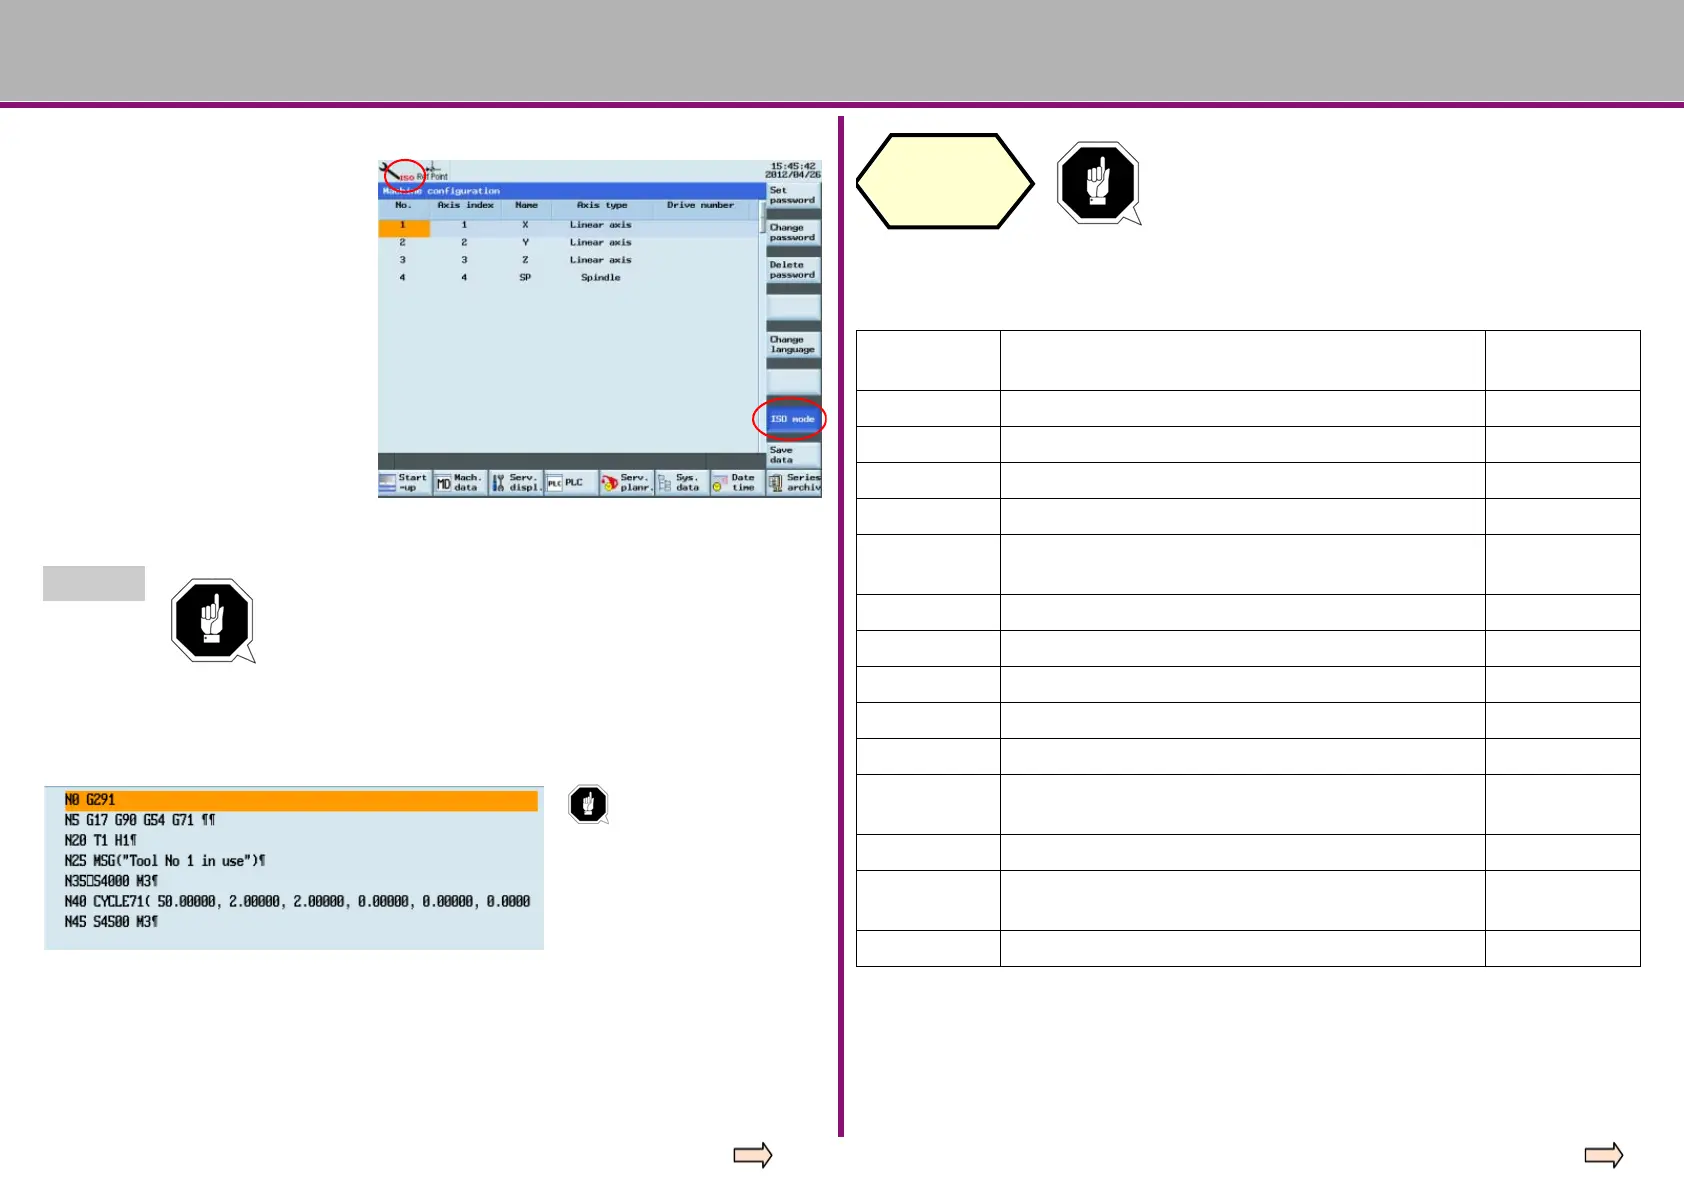
After pressing “OK”, the system
restarts automatically.
After restarting, press “Shift” +
“System - Alarm” again and if the
symbol in the red circle appears,
ISO mode is already activated.
A red ISO appears at the top of the screen and the ISO mode button on the right is
highlighted in blue.
Method 2
When using method 2 to activate the ISO mode, it will exit
ISO mode and return to the default DIN mode via “Reset”
button or after finishing the machining program.
Insert G291 in the first line of the ISO part program to be executed and insert G290 in
front of M30.
G291/G290
commands must
be set separately
in a line!
If ISO is displayed at the top of the screen, it is activated.
ISO code Description Compare with
DIN
G00 Orientation (rapid traverse) As DIN
G1 Linear difference As DIN
G17/G18/G19 XY plane / ZX plane / YZ plane As DIN
G20/G21 Input in inch/mm G70/G71
G41/G42/G40 Left tool tip radius compensation / right tool tip radius
compensation / cancel tool radius compensation
As DIN
G54 ~ G59 Select workpiece coordinate system As DIN
G80 Cancel fixed cycle
G90/G91 Absolute/incremental programming
G94/G95 Feedrate F in mm/min / mm/r As DIN
S Spindle speed As DIN
, R Reverse circle (note the form there must be ”, ”
before R parameter)
RND
M3/M4/M5 Spindle right / spindle left / spindle stop As DIN
M98 P _L_ Subprogram call (P+ subprogram name/ L+ times) Program name
+ L
M99 End of Subroutine M17
ISO code
explanation
All the ISO codes described in this unit can be
implemented in the ISO mode of the 808D system!




 To Next Page