www.parweld.com
19
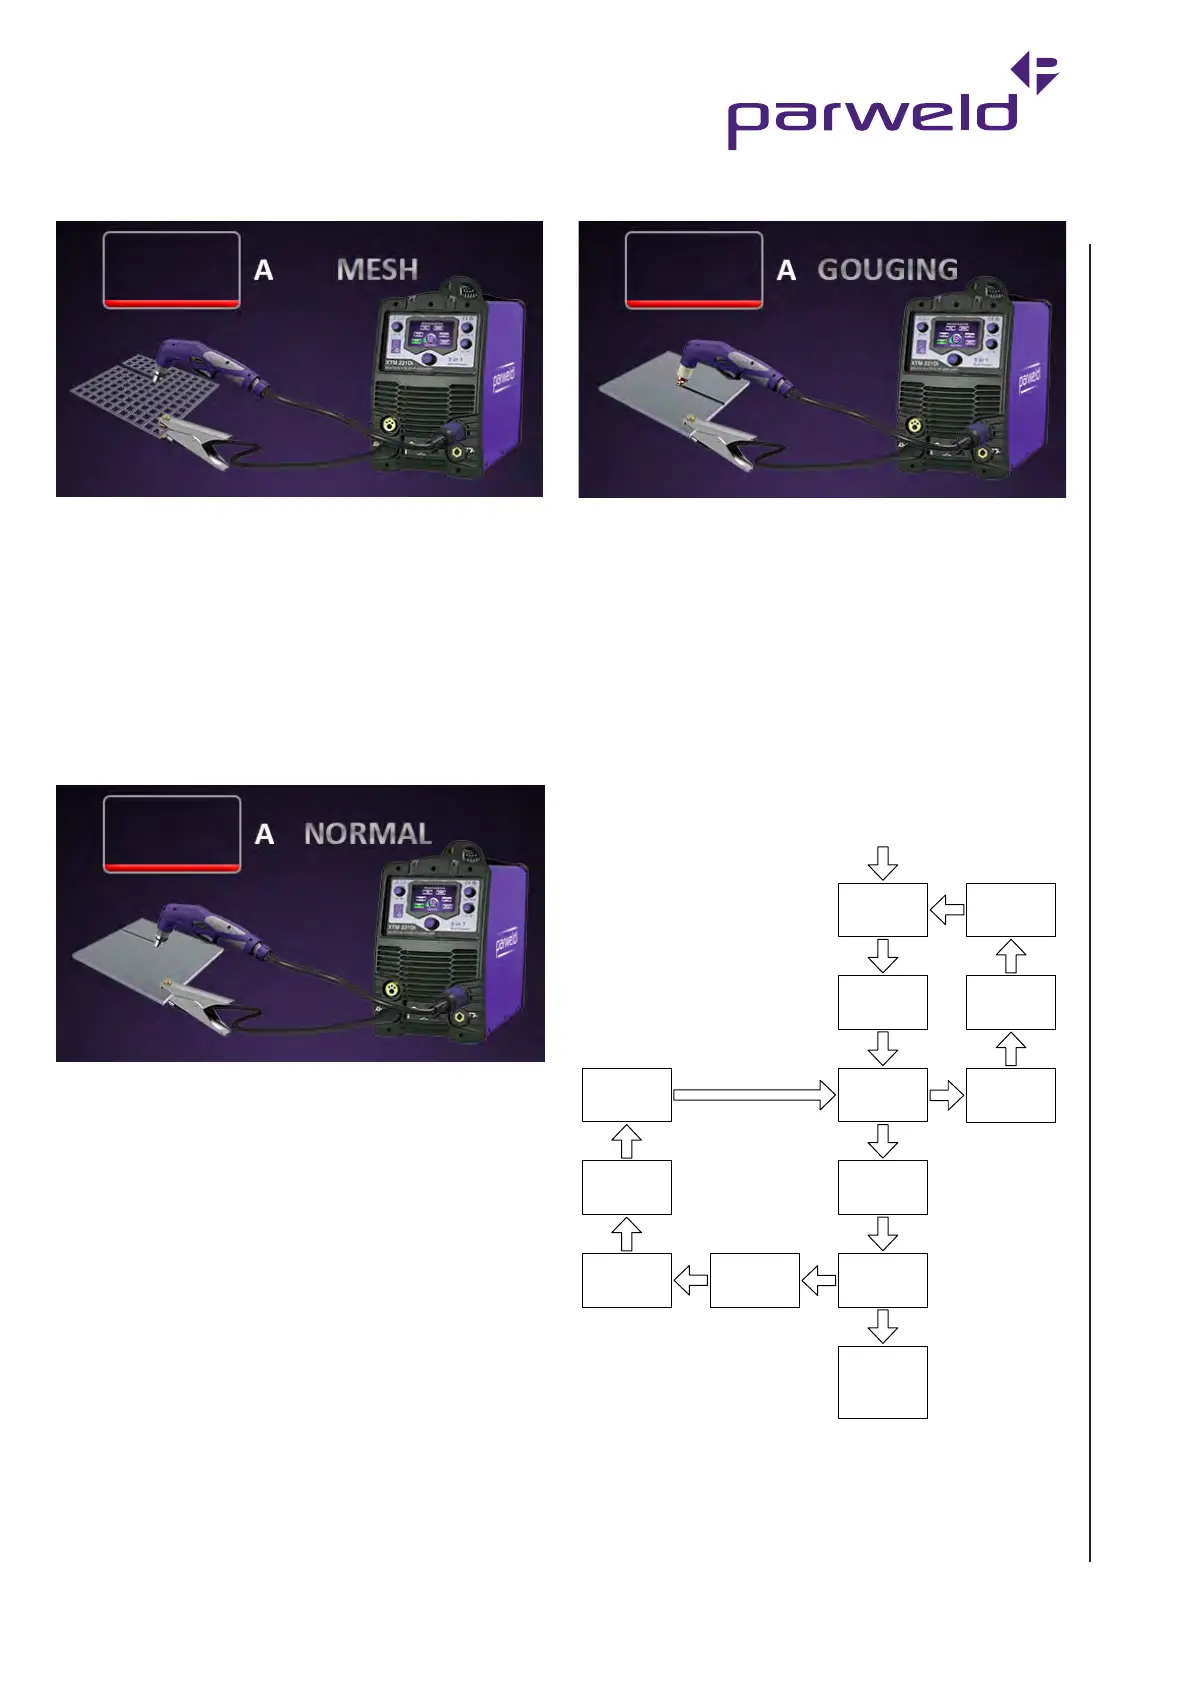
7.8.3 Mesh cutting
With the torch in starting position press and hold the trigger. After an
initial gas purge, the main arc will come on. Once on, the main arc
remains on as long as the trigger switch is held down. As you move
across the mesh the machine will automatically switch between
cutting mode and pilot arc mode when in a gap before swtching
back to cutting mode when the arc contacts the material again. To
shut o the torch simply release the trigger switch. When the switch
is released a 15 second post-ow will occur. If the torch switch is
closed during the post-ow, the cutting arc will restart after switching
o the air. Refer to the ow chart below for the operating sequence.
7.8.4 Normal cutting
With the torch in starting position press and hold the trigger. After an
initial gas purge, the main arc will come on. Once on, the main arc
remains on as long as the trigger switch is held down, unless the
torch is withdrawn from the work or torch motion is too slow. If the
cutting arc is interrupted, the cutting process must be restarted. To
shut o the torch simply release the trigger switch. When the switch
is released a 15 second post-ow will occur. If the torch switch is
closed during the post-ow, the cutting arc will restart after switching
o the air. Refer to the ow chart below for the operating sequence.
7.8.5 Gouging
Hold the torch so that the nozzle is 1-2mm from the workpiece
before starting the torch. Angle the torch 40 Deg. to the workpiece
with a small gap between the torch tip and the workpiece. Maintain
an approximate 40 Deg. angle to the workpiece as you move
along the gouge in the direction of the uncut material. Keep a
small distance between the torch tip and the molten metal to avoid
reducing consumable life or damaging the torch.
Changing the torch angle changes the dimensions of the gouge.
A steeper angle (closer to 90 Deg) and slower forward movement
gives a deeper gouge, while a lower angle (less than 40 Deg) and
faster movement gives a shallower gouge.
7.8.6 Torch Operation logic
Press Torch
Trigger
Air flows for
15 seconds
Air flow
switches on
Release
trigger
Pilot arc
strikes
Pilot arc
runs for 5
seconds
Cutting
starts
Release
trigger
Cutting
stops air
flows for 15
seconds
Cutting
stops
Press
trigger
Air flow
goes off
Air flow
switches on
Switch on
power
source
Air purges
for
10 seconds
Machine self
tests for
5 seconds
Machine
ready to run


 To Next Page