Rectifying faults
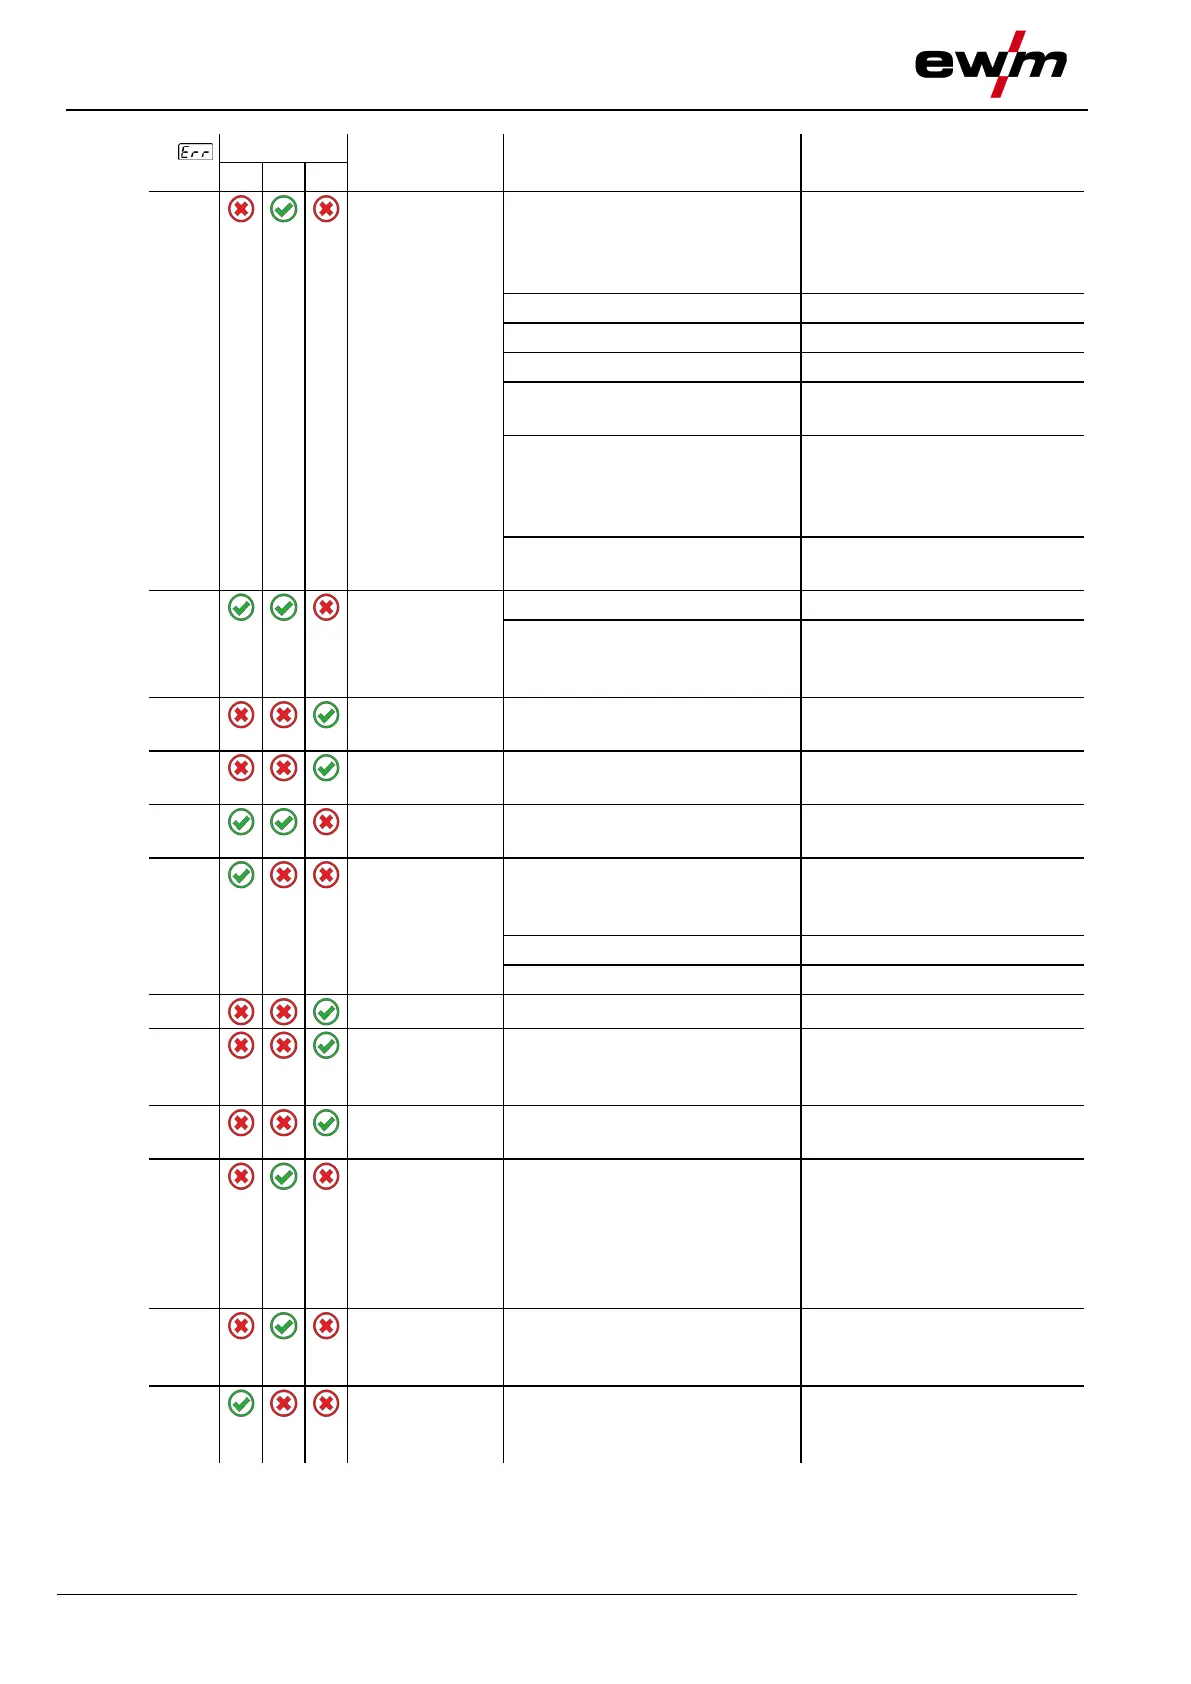
Error messages (power source)
099-5TLPXQ-EW501
29.01.2021
Flow rate too low (< = 0.7 l/min)
/ (< = 0.18 gal/min)
[1] [3]
Check coolant flow, clean wa-
ter block, remove kinks in
hose package, adjust flow
threshold
Air in the coolant circuit
Hose package not completely
filled with coolant
Switch machine off / on (pump
runs for 2 min)
Operation with gas-cooled
welding torch
Connect coolant feed and
coolant return (insert hose
bridge); deactivate water
block
Failure of automatic circuit-
breaker
[4]
Press to reset automatic cir-
cuit-breaker
Check shielding gas supply
Remove kinks in the hose
package; nominal value:
4-6 bar primary pressure
Overvoltage at output: Inverter
error
Connection between welding
wire and machine casing
Remove electrical connection
Removing the logical signal “ro-
bot ready” during the process
Eliminate errors on the higher-
level control
Coolant excess
temperature
[3]
Coolant is overheating (>=70°C
/ >=158°F)
[1]
measured in the
coolant return line
Allow the power source to
cool down (mains switch to
“1”)
Fan blocked, dirty or defective
Check fan, clean or replace
Air inlet or outlet blocked
Check air inlet and outlet
Short circuit in welding circuit
before welding
Eliminate short circuit in
welding circuit; remove exter-
nal sensor voltage
Short circuit in welding circuit
before welding
Eliminate short circuit in
welding circuit
No ignition occurred during a
process start with automated
machines
Check the wire feeding, check
the connections of the load
cables in the welding circuit,
clean corroded surfaces on
the workpiece before welding
if applicable
An arc interruption occurred
during welding with an automa-
ted system
Check wire feeding; adjust
welding speed.
The emergency stop circuit of
the power source has been ac-
tivated.
Disable the activation of the
emergency stop circuit (re-
lease protective circuit)


 To Next Page