SECTION 2 - PROCEDURES
2-10 3121801
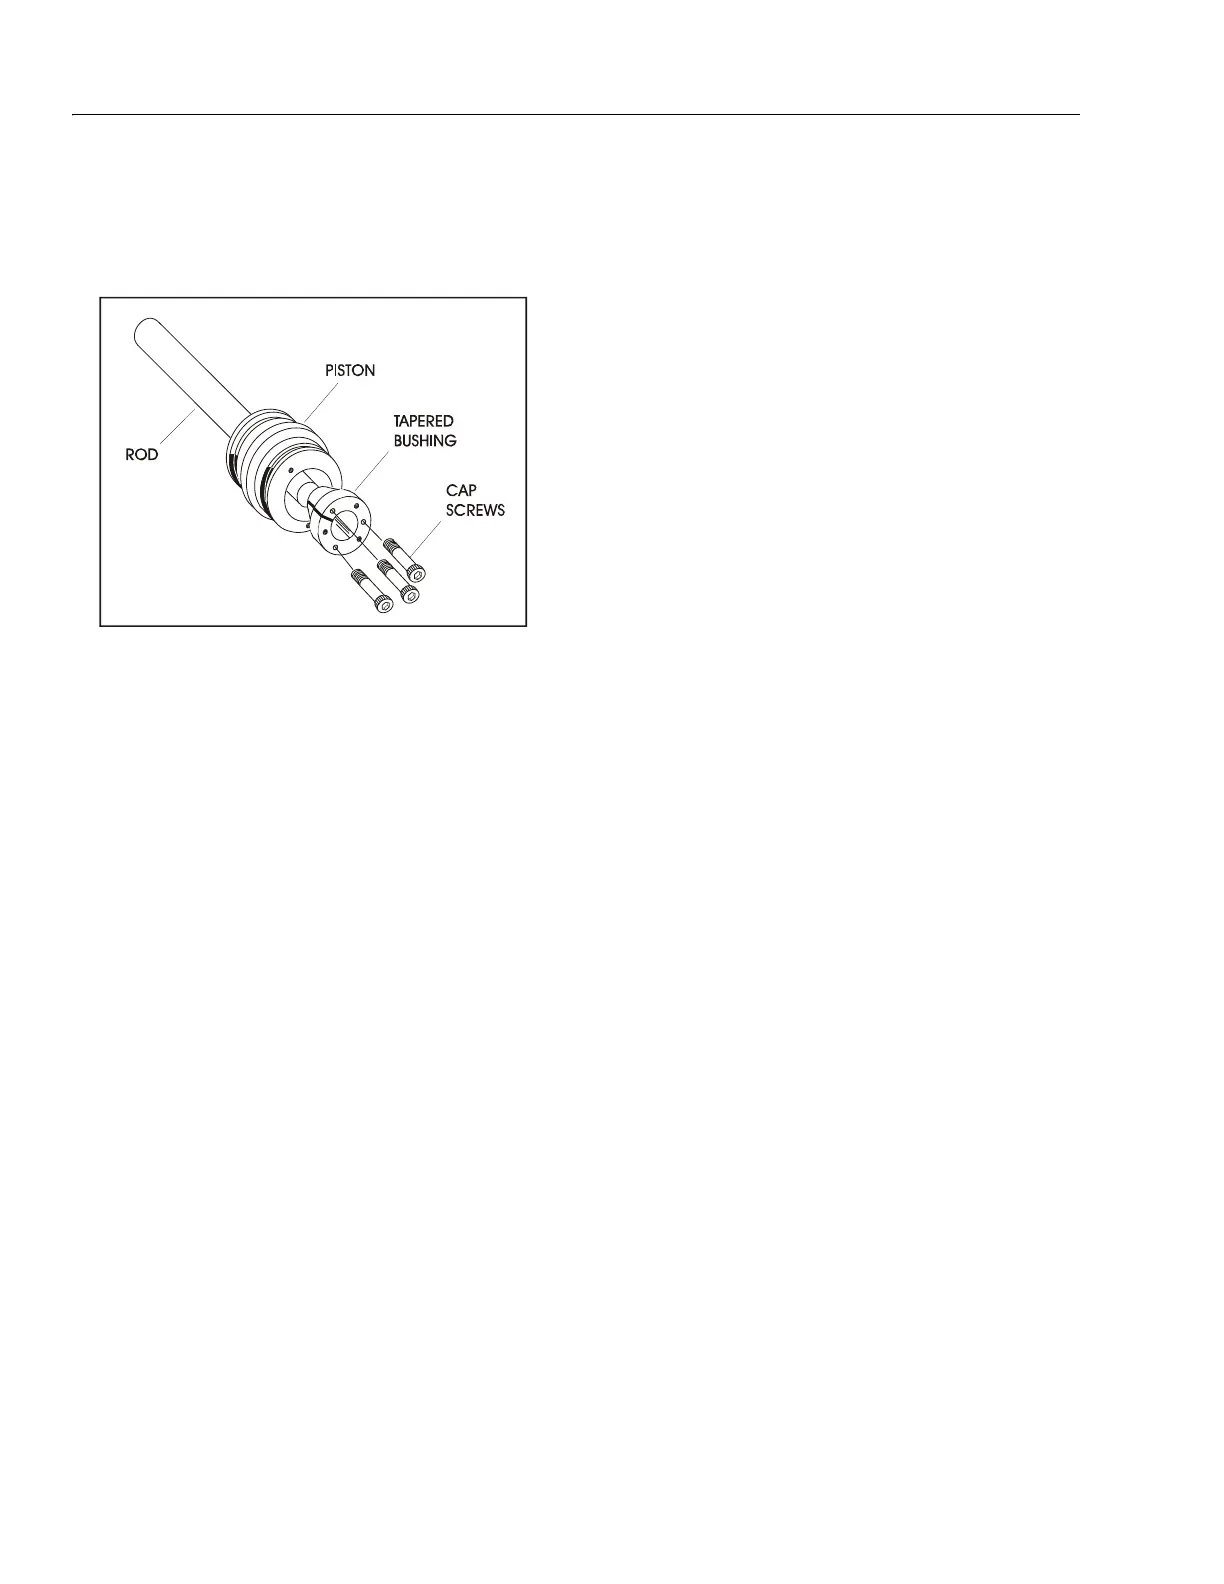
11. Insert the cap screw(s) in the threaded holes in the outer
piece of the tapered bushing. Progressively tighten the
cap screw(s) until the bushing is loose on the piston.
12. Remove the bushing from the piston.
13. Screw the piston CCW, by hand, and remove the piston
from cylinder rod.
14. Remove and discard the piston o-rings, seal rings, and
backup rings.
15. Remove piston spacer, if applicable, from the rod.
16. Remove the rod from the holding fixture. Remove the
cylinder head gland and retainer plate, if applicable. Dis-
card the o-rings, back-up rings, rod seals, and wiper
seals.
Cleaning and Inspection
1. Clean all parts thoroughly in an approved cleaning sol-
vent.
2. Inspect the cylinder rod for scoring, tapering, ovality, or
other damage. If necessary, dress rod with Scotch Brite
or equivalent. Replace rod if necessary.
3. Inspect threaded portion of rod for excessive damage.
Dress threads as necessary.
4. Inspect inner surface of cylinder barrel tube for scoring
or other damage. Check inside diameter for tapering or
ovality. Replace if necessary.
5. Inspect threaded portion of barrel for damage. Dress
threads as necessary.
6. Inspect piston surface for damage and scoring and for
distortion. Dress piston surface or replace piston as nec-
essary.
7. Inspect threaded portion of piston for damage. Dress
threads as necessary.
8. Inspect seal and o-ring grooves in piston for burrs and
sharp edges. Dress applicable surfaces as necessary.
9. Inspect cylinder head inside diameter for scoring or
other damage and for ovality and tapering. Replace as
necessary.
10. Inspect threaded portion of head for damage. Dress
threads as necessary.
11. Inspect seal and o-ring grooves in head for burrs and
sharp edges. Dress applicable surfaces as necessary.
12. Inspect cylinder head outside diameter for scoring or
other damage and ovality and tapering. Replace as nec-
essary.
13. If applicable, inspect rod and barrel bearings for signs of
correct excessive wear or damage. Replace as necessary.
a. Thoroughly clean hole, (steel bushing) of burrs, dirt
etc. to facilitate bearing installation.
b. Inspect steel bushing for wear or other damage. If
steel bushing is worn or damaged, rod/barrel must
be replaced.
c. Lubricate inside of the steel bushing with WD40
prior to bearing installation.
d. Using an arbor of the correct size, carefully press the
bearing into steel bushing.
14. Inspect travel limiting collar or spacer for burrs and
sharp edges. If necessary, dress inside diameter surface
with Scotch Brite or equivalent.
15. If applicable, inspect port block fittings and holding
valve. Replace as necessary.
16. Inspect the oil ports for blockage or the presence of dirt
or other foreign material. Repair as necessary.
17. If applicable, inspect piston rings for cracks or other
damage. Replace as necessary.
Figure 2-7. Tapered Bushing Removal


 To Next Page