Valve
seat
1.
The valve seat
is
subject
to
severe wear.
Whenever the
valve
is
replaced or the
valve face
is
resurfaced
(see
caution),
the
valve seat should
be
resurfaced at a
45° angle. If a new valve guide has been
installed, the valve seat must
be
recut to
guarantee
complete sealing between the
valve face and seat.
If
the
valve
seat is
obviously
pitted
or
worn,
it
should
be
cleaned
with
a
valve
seat
cutter.
Use
the
45°
cutter.
When
twisting
the
cutter,
keep
an even
downward
pressure
to
prevent
chatter
marks.
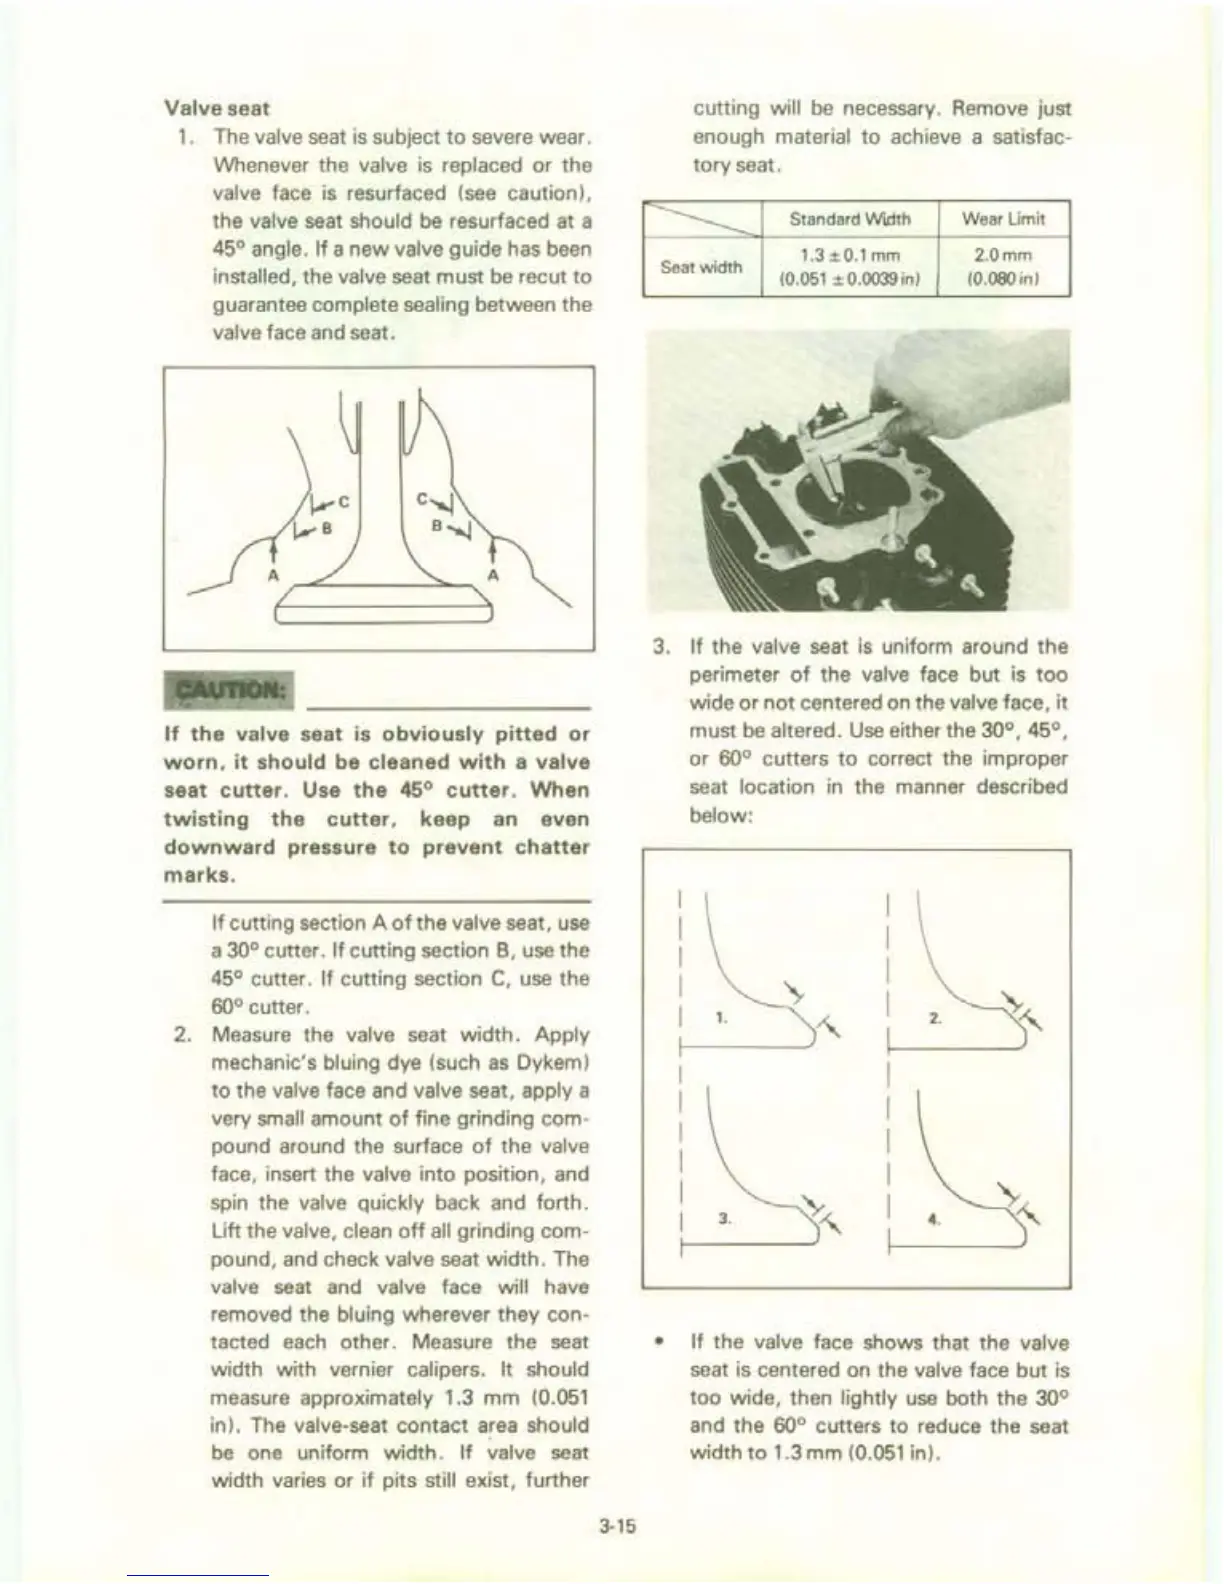
If
cutting section A
of
the valve seat,
use
a 30° cutter. If cutting section 8,
use
the
45° cutter. If cutting section
C,
use
the
60° cutter.
2.
Measure the valve seat width. Apply
mechanic's bluing dye (such
as
Dykem)
to
the valve face and valve seat, apply a
very
small amount
of
fine grinding com-
pound around the surface
of
the valve
face, insert the valve into position, and
spin the
valve quickly back and forth.
Lift the
valve, clean
off
all
grinding com-
pound, and check
valve seat width. The
valve seat and valve face will have
removed the
bluing wherever they con-
tacted each other. Measure the seat
width with vernier
calipers. It should
measure approximately 1.3 mm
(0.051
in). The valve-seat contact
area
should
be
one uniform width.
If
valve seat
width varies or
if
pits still exist, further
3-15
cutting will
be
necessary. Remove just
enough
material to achieve a satisfac-
tory
seat.
-----------
Standard Width
Wear Limit
Seat width
1.3
±0.1
mm 2.
0mm
(0.051 ± 0.0039 in)
(0.080 in)
3.
If the valve seat
is
uniform around the
perimeter
of
the valve face but
is
too
wide or
not
centered
on
the valve face,
it
must
be
altered.
Use
either the 30°, 45°,
or 60° cutters
to
correct the improper
seat
location
in
the manner described
below:
1.
2.
3.
• If the valve face shows that the valve
seat is centered
on
the valve face but is
too wide, then
lightly
use
both the 30°
and the 60° cutters to reduce the seat
width
to
1.3 mm
(0.051
in).


 To Next Page