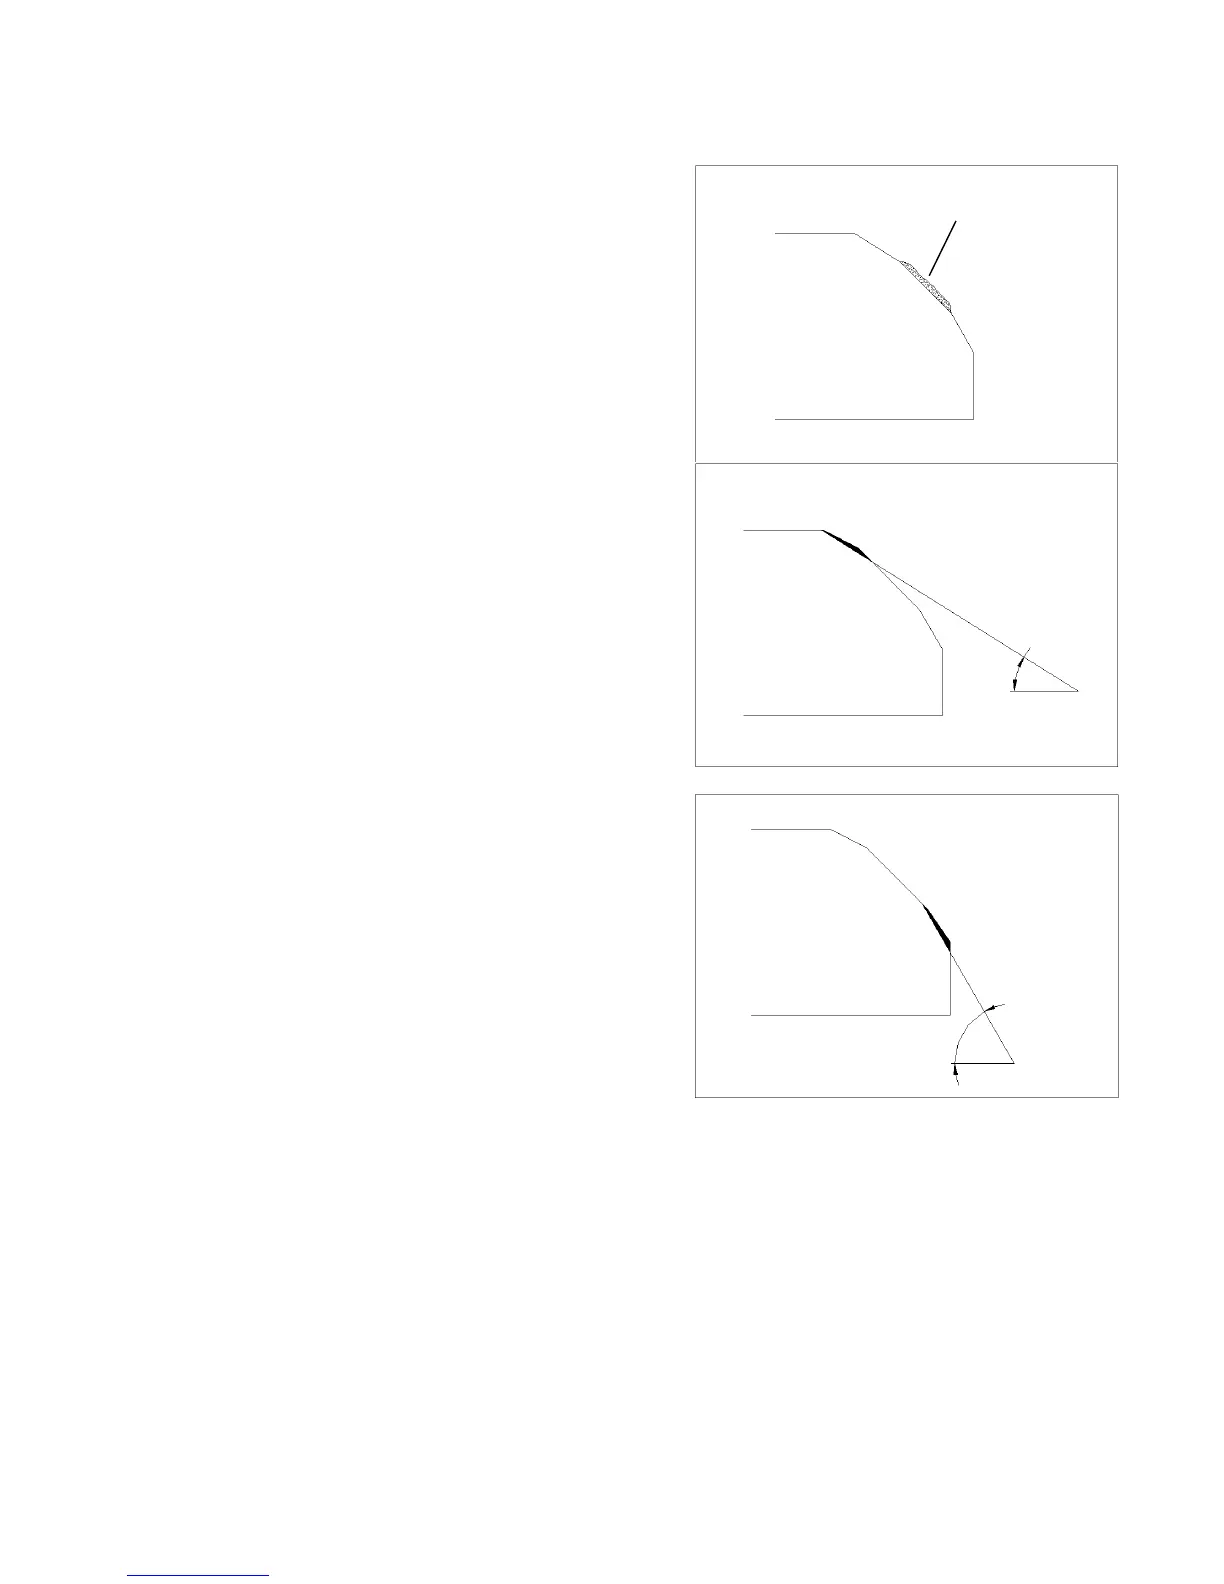
Refinishing of the Valve Seat
Use a 45° milling cutter to clear out the rough or
uneven parts on the surface of the valve seat.
Note: Coat the valve seat ring with a transparent or
Prussian blue coating to see more clearly.
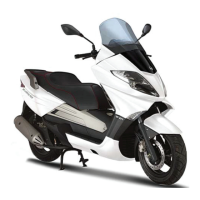
Use a 32° milling cutter to clear out the 1/4 of the
outer end of valve seat.
rough
32°
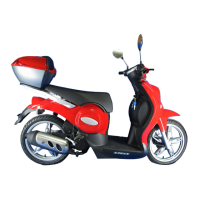
Use a 60° milling cutter to clear out the 1/4 of the
bottom of valve seat. Take down the milling cutter and
inspect the treated parts.
60°


 To Next Page