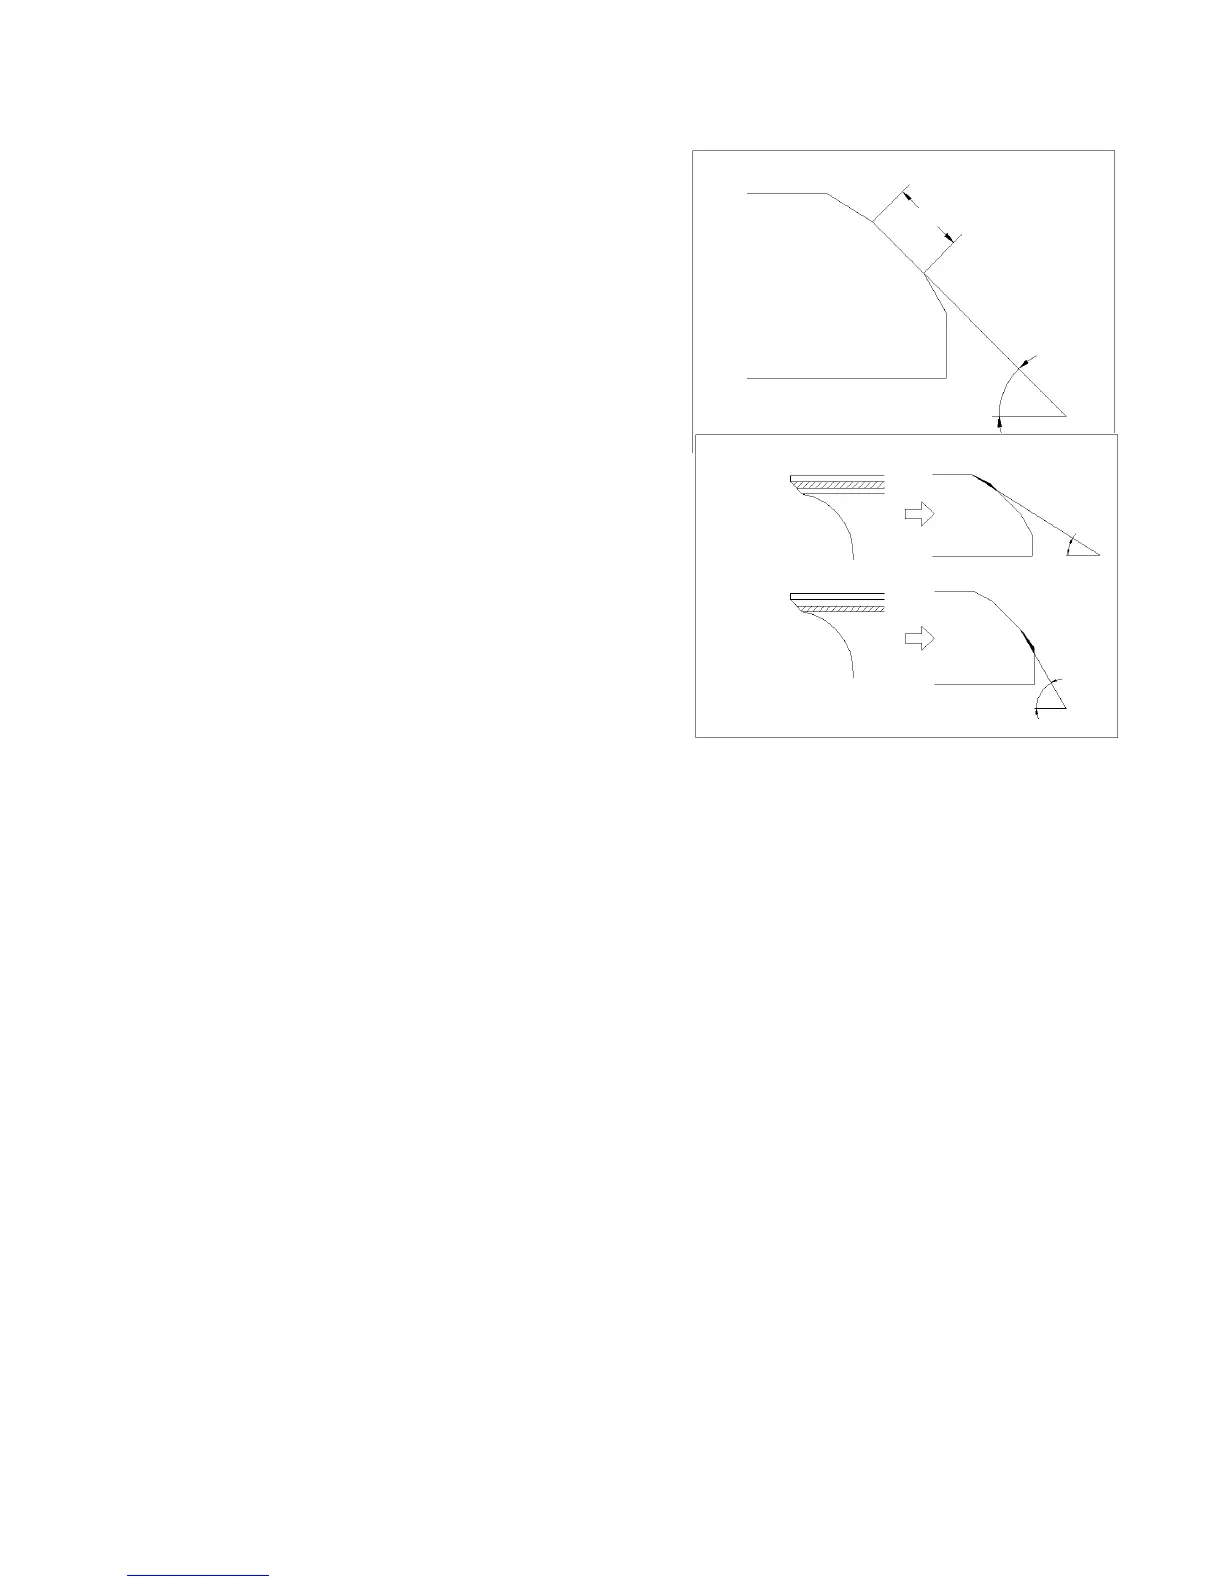
Use a 45° milling cutter to cut the valve seat to its
appropriate width.
All the indentation and uneven parts have to be
eliminated.
Standard width of valve seat ring:Inlet:0.8mm
Exhaust:0.8mm
If the contacting part is the place where the valve is too
high, please use a 32° flat milling cutter to lower the
valve seat.
If the contacting part is the place where the valve is
①
too low, please use a 60° inner milling cutter to elevate
the valve seat.
Use a 45° finishing milling cutter to cut the valve seat
to its appropriate specification.
After the cutting of the valve seat, please coat
②
polishing agent onto the surface of valve and polish the
valve slightly.
①:high contacting surface
②:low contacting surface
0.8mm
Installation
The installation sequence shall be in reversed sequence of removal.
Note:
When installing the valve spring, put the spring pitch span of smaller end towards the combustion
chamber. When installing the valve collet, please use valve spring compression tools.
When installing the valves, please grease the surface of valve lever with machine oil first, then
put it into the valve guide.


 To Next Page