OM-258 035 Page 27
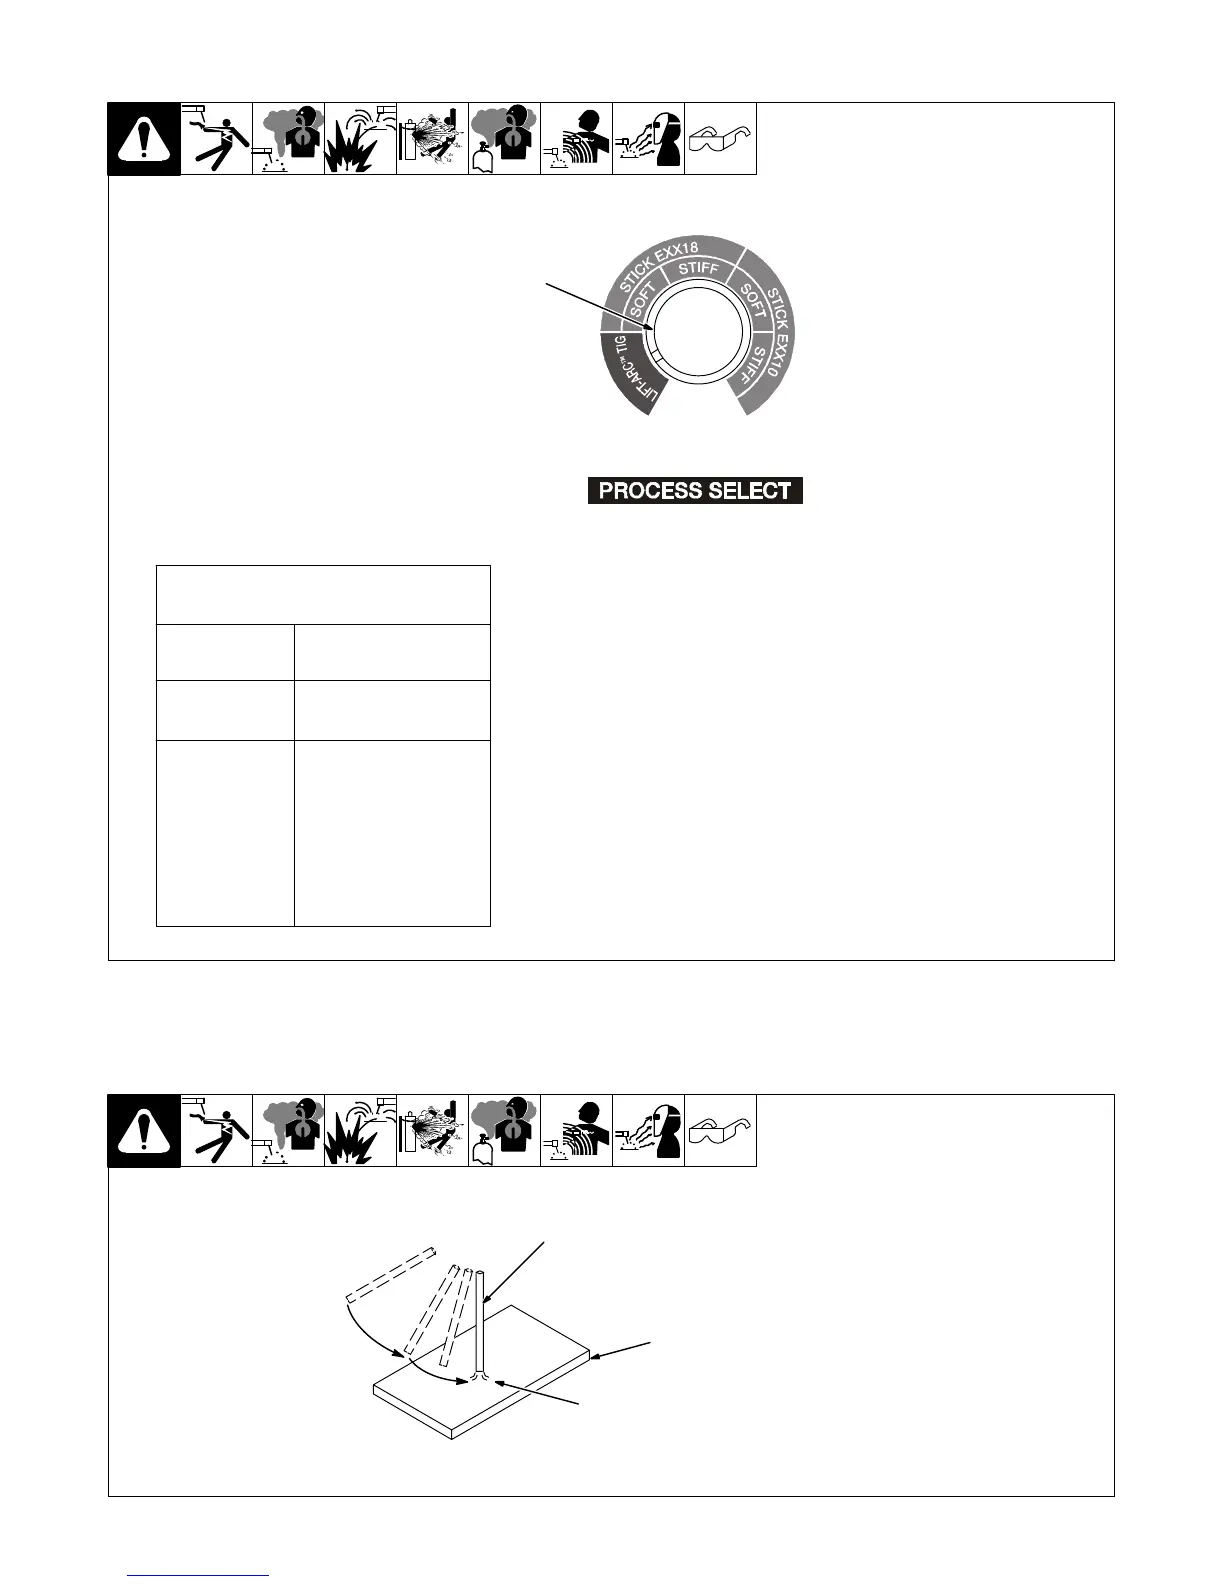
6-2. Process Select Control
1 Process Select Control
Rotate knob to select desired
process.
Lift-Arc TIG - Normal open-cir-
cuit voltage is not present between
the electrode and workpiece. A sol-
id-state contactor does not ener-
gize until after the electrode
touches the workpiece, preventing
overheating, sticking, or contamin-
ating the electrode (see Section
6-4). Make connections according
to Section 5-4.
Stick EXX18 Soft - This setting
provides a lower dig/arc force
setting for smooth weld perfor-
mance. A stable weld puddle with
little arc “snap” gives excellent weld
bead appearance with minimal
spatter. Make connections
according to Section 5-5.
Stick EXX18 Stiff - This setting
provides a higher dig/arc force that
gives a slightly more fluid weld
puddle, more arc “snap”, and
reduces the potential for electrode
sticking at shorter arc lengths.
Make connections according to
Section 5-5.
Stick EXX10 Soft - This setting
provides lower dig/arc force for
open root vertical up joints or joints
that do not require additional
current for fit up inconsistencies.
Make connections according to
Section 5-5.
Stick EXX10 Stiff - This setting
provides a higher dig/arc force for
open root vertical down joints
where additional current is needed
to compensate for tight joint fit up
without the need to increase overall
welding current. Make connections
according to Section 5-5.
ELECTRODE
TYPE
SUGGESTED PROCESS
SETTING
EXXX1
EXXX2
EXX10
EXX10
EXXX3
EXXX4
EXXX5
EXXX6
EXXX7
EXXX8
STAINLESS
EXX18
EXX18
EXX18
EXX18
EXX18
EXX18
EXX18
RECOMMENDED PROCESS
SELECTIONS VS ELECTRODE TYPE
1
6-3. Stick Start Procedure − Scratch Start Technique
With Stick selected, start arc as
follows:
1 Electrode
2 Workpiece
3 Arc
Drag electrode across workpiece like
striking a match; lift electrode slightly
after touching work. If arc goes out
electrode was lifted to high. If
electrode sticks to workpiece, use a
quick twist to free it.
VRD Model Only: Normal open-cir-
cuit voltage is not present before elec-
trode touches workpiece; only a low
sensing voltage is present between
electrode and workpiece. This allows
electrode to touch workpiece without
overheating, sticking, or getting con-
taminated.
1
2
3



 To Next Page