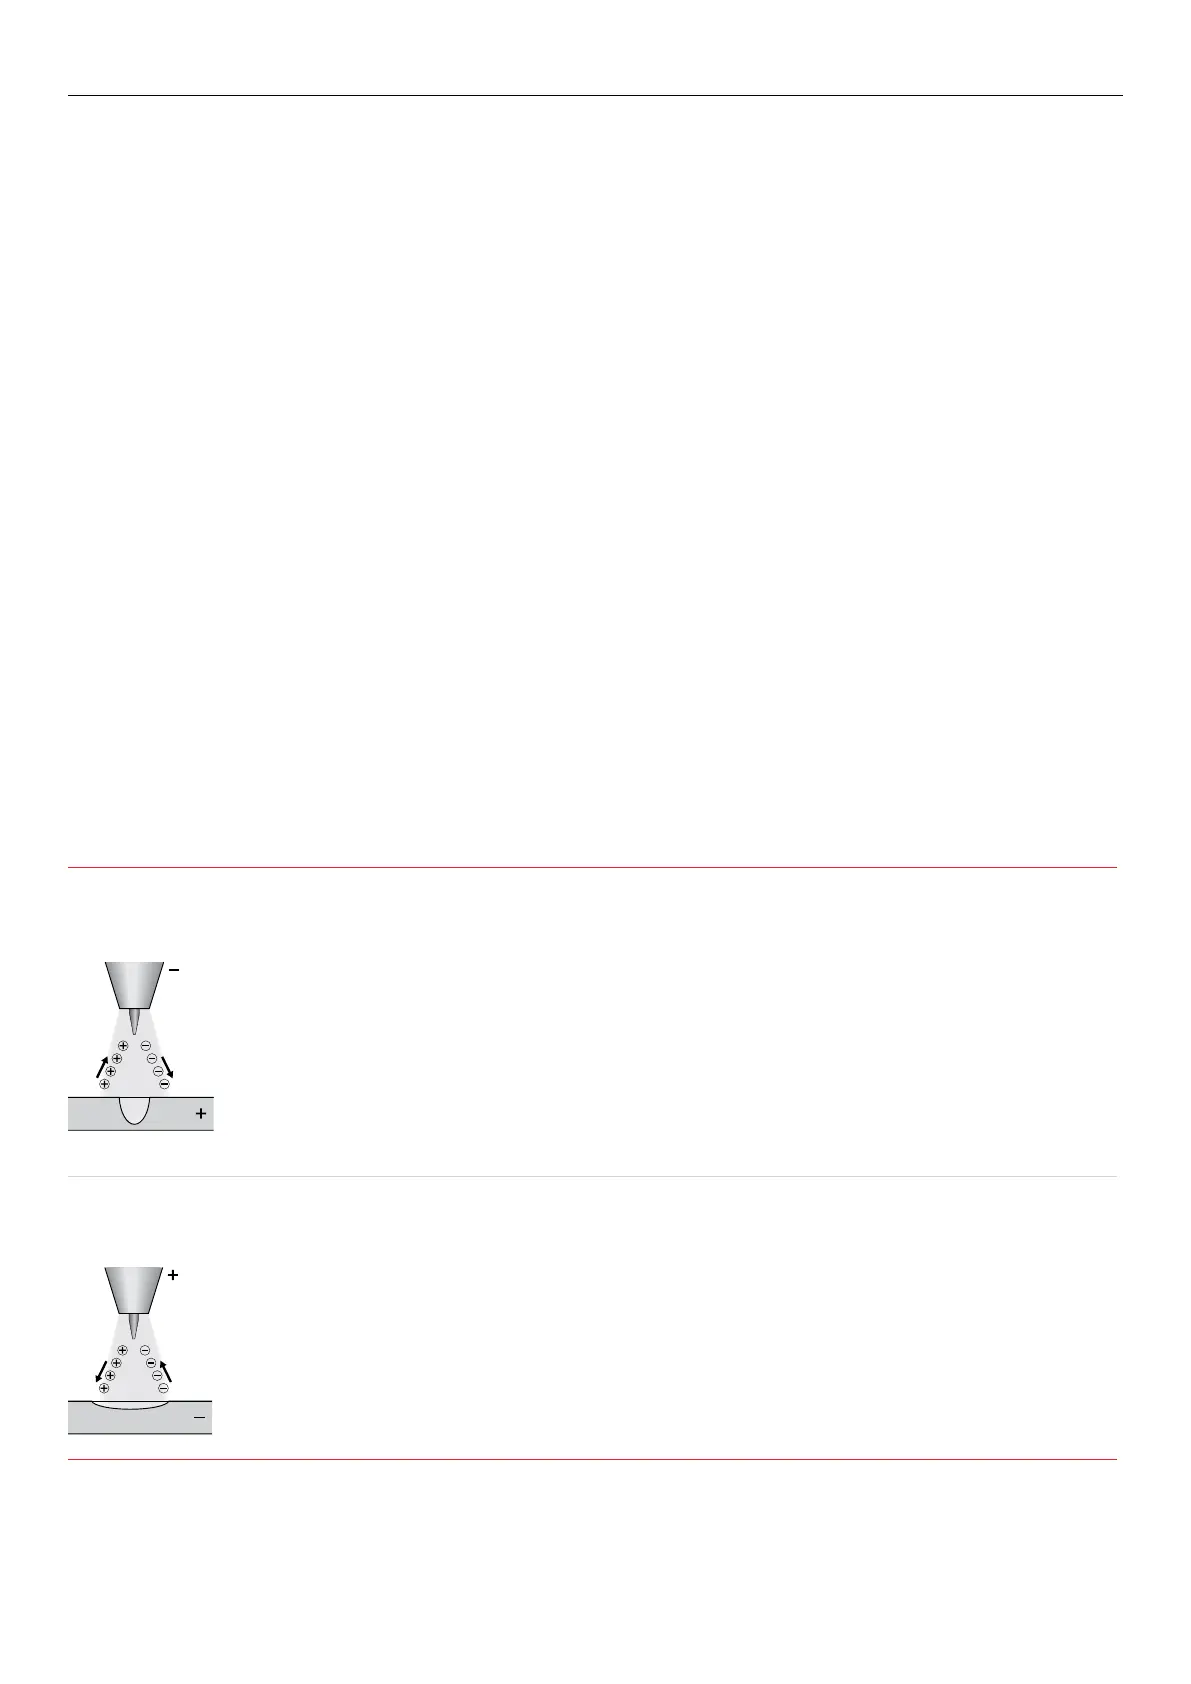
Process variable Explanation Usage
DCEN
Narrow bead,
deeppenetration
Nozzle
Ions Electrons
When direct-current electrode-negative (straight polarity)
is used:
→ Electrons strike the part being welded at a highspeed
→ Intense heat on the base metal is produced
→ The base metal melts very quickly
→ Ions from the inert gas are directed towards the
negative electrode at a relatively slow rate
→ Direct current with straight polarity does not require
post-weld cleaning to remove metaloxides
For a given diameter of tungsten electrode, higher
amperage can be used with straight polarity. Straight
polarity is used mainly for welding:
→ Carbon steels
→ Stainless steels
→ Copper alloys
The increased amperage provides:
→ Deeper penetration
→ Increased welding speed
→ A narrower, deeper, weld bead
DCEP
Wide bead,
shallowpenetration
Nozzle
Ions Electrons
The DCEP (reverse polarity) are dierent from the DCEN in
followingways:
→ High heat is produced on the electrode rather on the
base metal
→ The heat melts the tungsten electrode tip
→ The base metal remains relatively cool compared to
sing straight polarity
→ Relatively shallow penetration is obtained
→ An electrode whose diameter is too large will reduce
visibility and increase arc instability
→ Intense heat means a larger diameter of electrode
must be used with DCEP
→ Maximum welding amperage should be relatively low
(approximately six times lower than with DCEN)
43BOC Smootharc Multi 180/200 Operating manual




 To Next Page