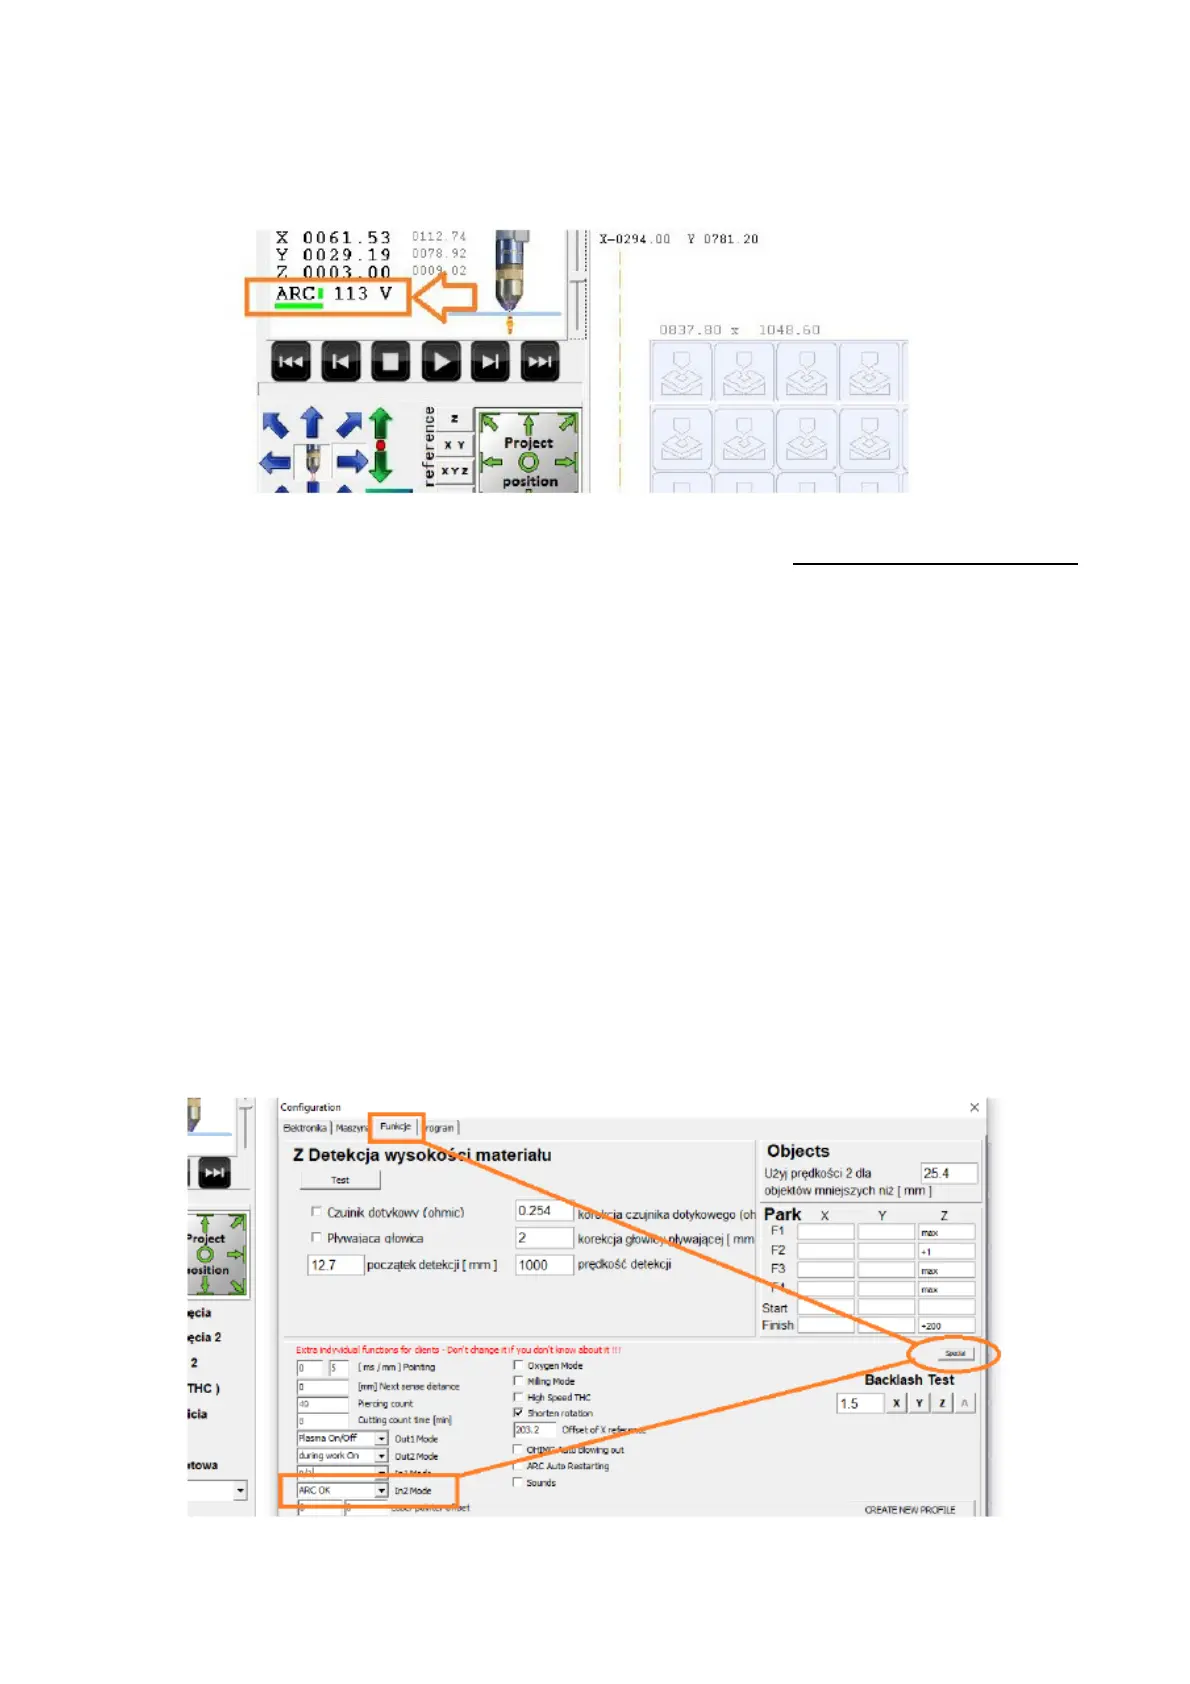
When performing the test cut, observe the displayed ARC voltage,
which should be 70 - 170 V*, other values indicate incorrect configuration
and/or incorrect connection - stop the test cut immediately and ensure that
everything has been connected and configured correctly ( point 8.3 , 8.4 ).
If there is a slight discrepancy in the readings, the readings can be
corrected with the actual measurement in the Voltage Calibration
parameter.
If everything is working correctly, a wait for the feedback signal can
be switched on which will cancel the "delayed" plasma engagement in
relation to the XY movement.
The signal confirming the main arc is generated automatically on the
basis of the arc voltage analysis ( ARC ). It is not necessary to provide
such a signal externally.
If you have problems with the correct detection of the main arc
despite correct measurement, you can use the signal from the cutter ( if the
source has this option ), usually called ARC OK, OK TO MOVE etc. by
connecting them to Input2 of the MyPlasm CNC controller ( IN and
MINUS pins ) and selecting the corresponding option in the special
functions.
28


 To Next Page