Pg 23 S22A/S23A 2001b 2100 v1.0
MECHANICAL CONTROLS
HEAD SWING and BRAKE
An integral function of the S-23A is the ability to make mitred
cuts at angles between 90
O
and 45
O
.The Head swing of the S-23A
is easily changed to set a different cutting angle by first releasing
the Angle Brake lever, and then manually moving the Head to the
cutting angle desired. An angle scale with a pointer in clear view of
the saw operator allows for accurate setting of the cutting angle.
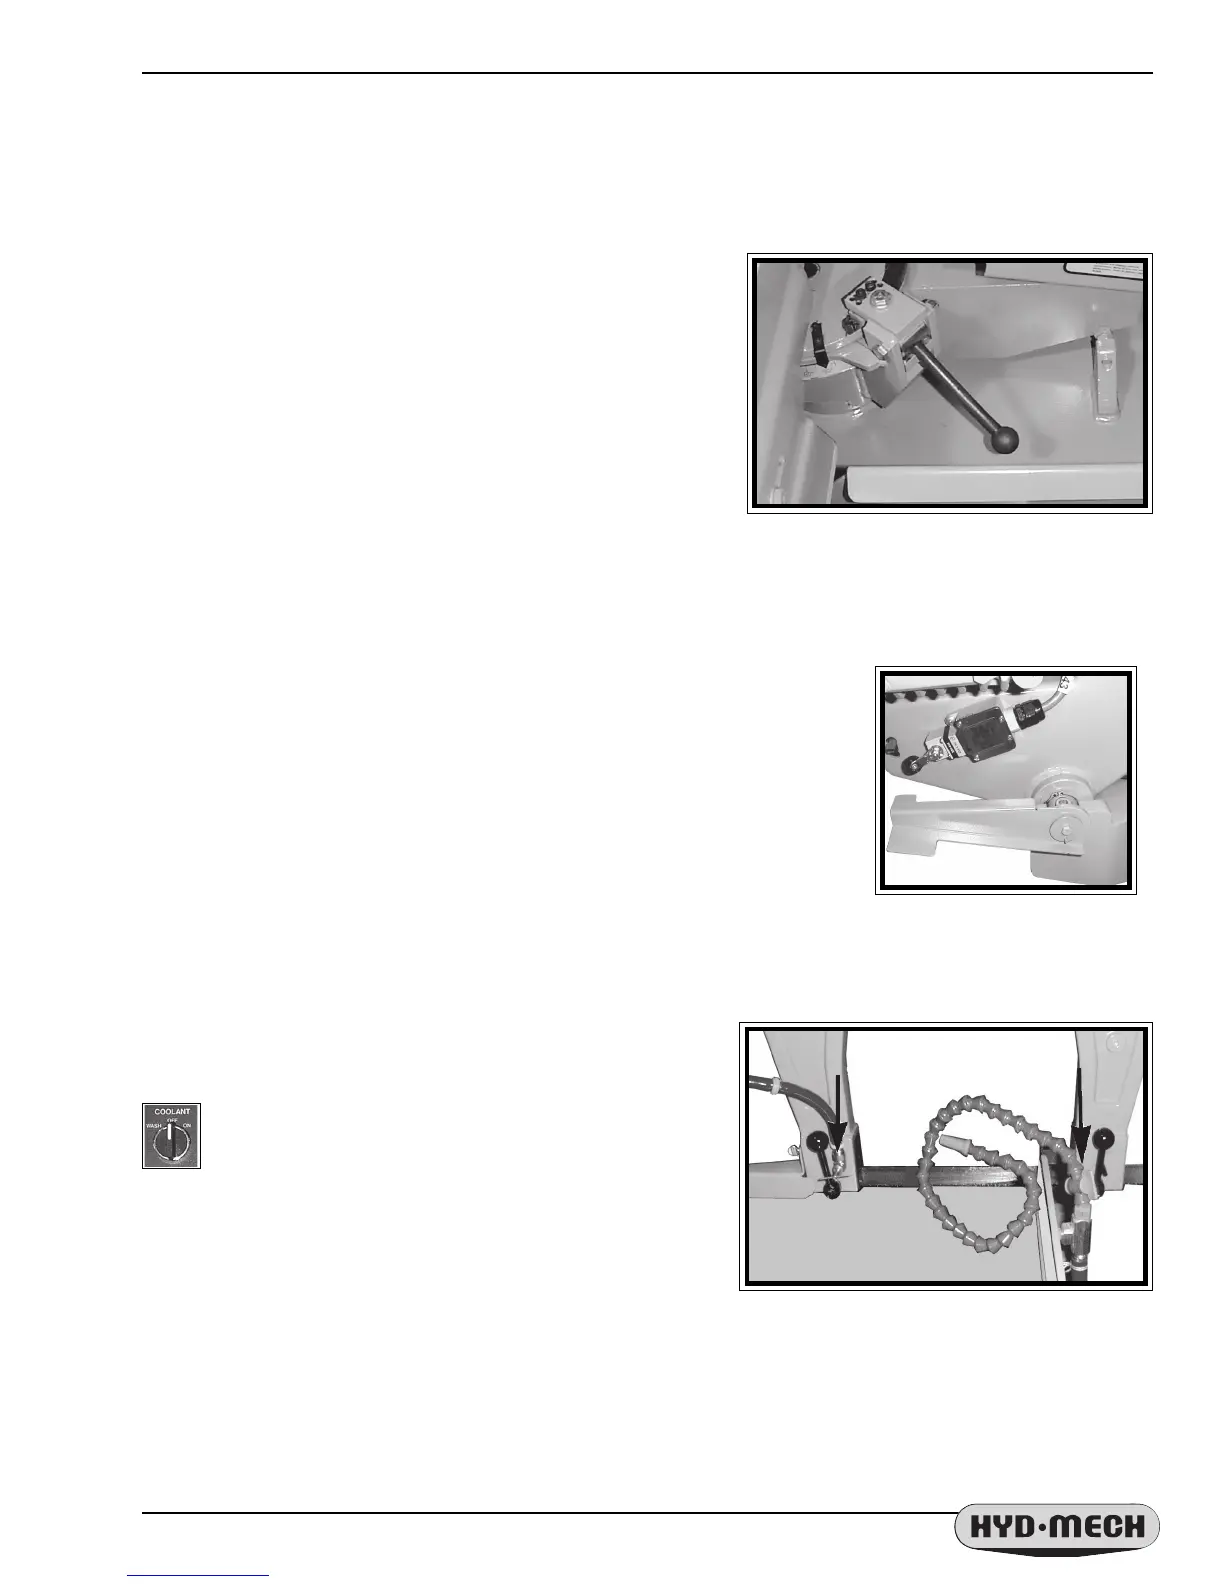
The Angle Brake lever is then locked in position by pushing it
into the down position. Note that the angle brake should be locked
into position whenever cutting with the saw. The following
photograph illustrates the Angle Brake in the locked position at
88
O
. To set the saw to the 90
O
position, set the Head in the fully
down position and is moved until the frame meets the 90
O
stop
bolt which is located on the vise post.
HEAD UP LIMIT SETTING
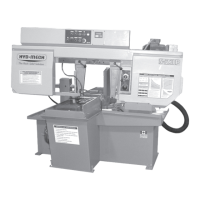
The Head Up limit setting allows the operator to set the height that the Head
will ascend to after a cut is completed. By adjusting this limit the operator can
reduce cycle time as the Head does not need to fully ascend between cuts. The
Head Up adjustment lever is located on the rear side of the head below the gear
box as shown below. Raising the lever will shorten the distance the head will
move. Lowering the lever all the way down will allow the head to travel to it's full
height.
Head Swing Scale and Angle Brake
(Locked)
COOLANT FLOW
The main coolant control is found on the control panel.
WASH: Coolant flows any time the machine is under power,
permitting wash down with spray nozzle without running
machine.
OFF: No coolant flow.
ON: The coolant flows only when the blade is running
OR when the blade is running and the head is
descending. This is selectable via the PLC parameters.
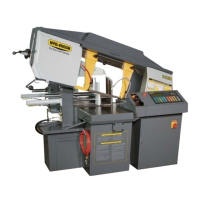
The S-23A bandsaw is equipped with two independently
controlled coolant spouts that are capable of supplying a
generous flow of coolant to the blade.
The left guide arm supplies a flow of coolant that should flood
the blade as it moves through the carbide pads into the material to be cut. The adjustable spout on the left guide
arm should be set with the blade speed to provide the flood of coolant necessary.
The right guide arm provides a coolant flow through the flexible hose that can be pointed directly where
necessary. This flexible hose should be used when cutting solid bars, bundles, or wide structurals. Set the flow of
coolant directly into the opening in the material where the blade is cutting.
NOTE: When cutting materials that do not need constant coolant, such as Cast Iron, some coolant flow is
required for blade lubrication to prevent blade scoring by the carbide pads as the blade moves through them.
Coolant Valve on Guide
Arm and on the Fence.
Head Up Limit Setting Lever



 To Next Page