300/400TS and 300/400S 4 OPERATOR CONTROLS
4 – 2
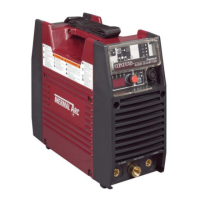
3. Positive Terminal: Welding current flows from
the Power Source via heavy duty Dinse type
terminal (50 mm). It is essential, however,
that the male plug is inserted and turned
securely to achieve a sound electrical connec-
tion.
4. Negative Terminal: Welding current flows
from the Power Source via heavy duty Dinse
type terminal (50 mm). It is essential, how-
ever, that the male plug is inserted and turned
securely to achieve a sound electrical connec-
tion.
CAUTION
Loose welding terminal connections can cause
overheating and result in the male plug being fused
in the bayonet terminal.
5. Gas Outlet: The Gas Outlet is a 5/8 18 UNF
female gas fitting. (300/400TS only)
6. ON/OFF Switch: This switch connects the Pri-
mary supply voltage to the inverter when in the
ON position. This enables the Power Supply.
WARNING
When the welder is connected to the Primary sup-
ply voltage, the internal electrical components
maybe at 240V potential with respect to earth.
7. Input Cable: The input cable connects the Pri-
mary supply voltage to the equipment.
8. SMART Logic Switch: Manual slide switch
mounted on the back panel selects the pr
oper
i
nput voltage. If this slide is not set to the posi-
tion that matches the input voltage from the
electrical source the Smart Logic circuit will
inhibit welding power source output. The digi-
tal meter will show primary input error code.
9. Gas Inlet: The Gas Inlet is a 5/8 18 UNF
female gas fitting. (300/400TS only)
2
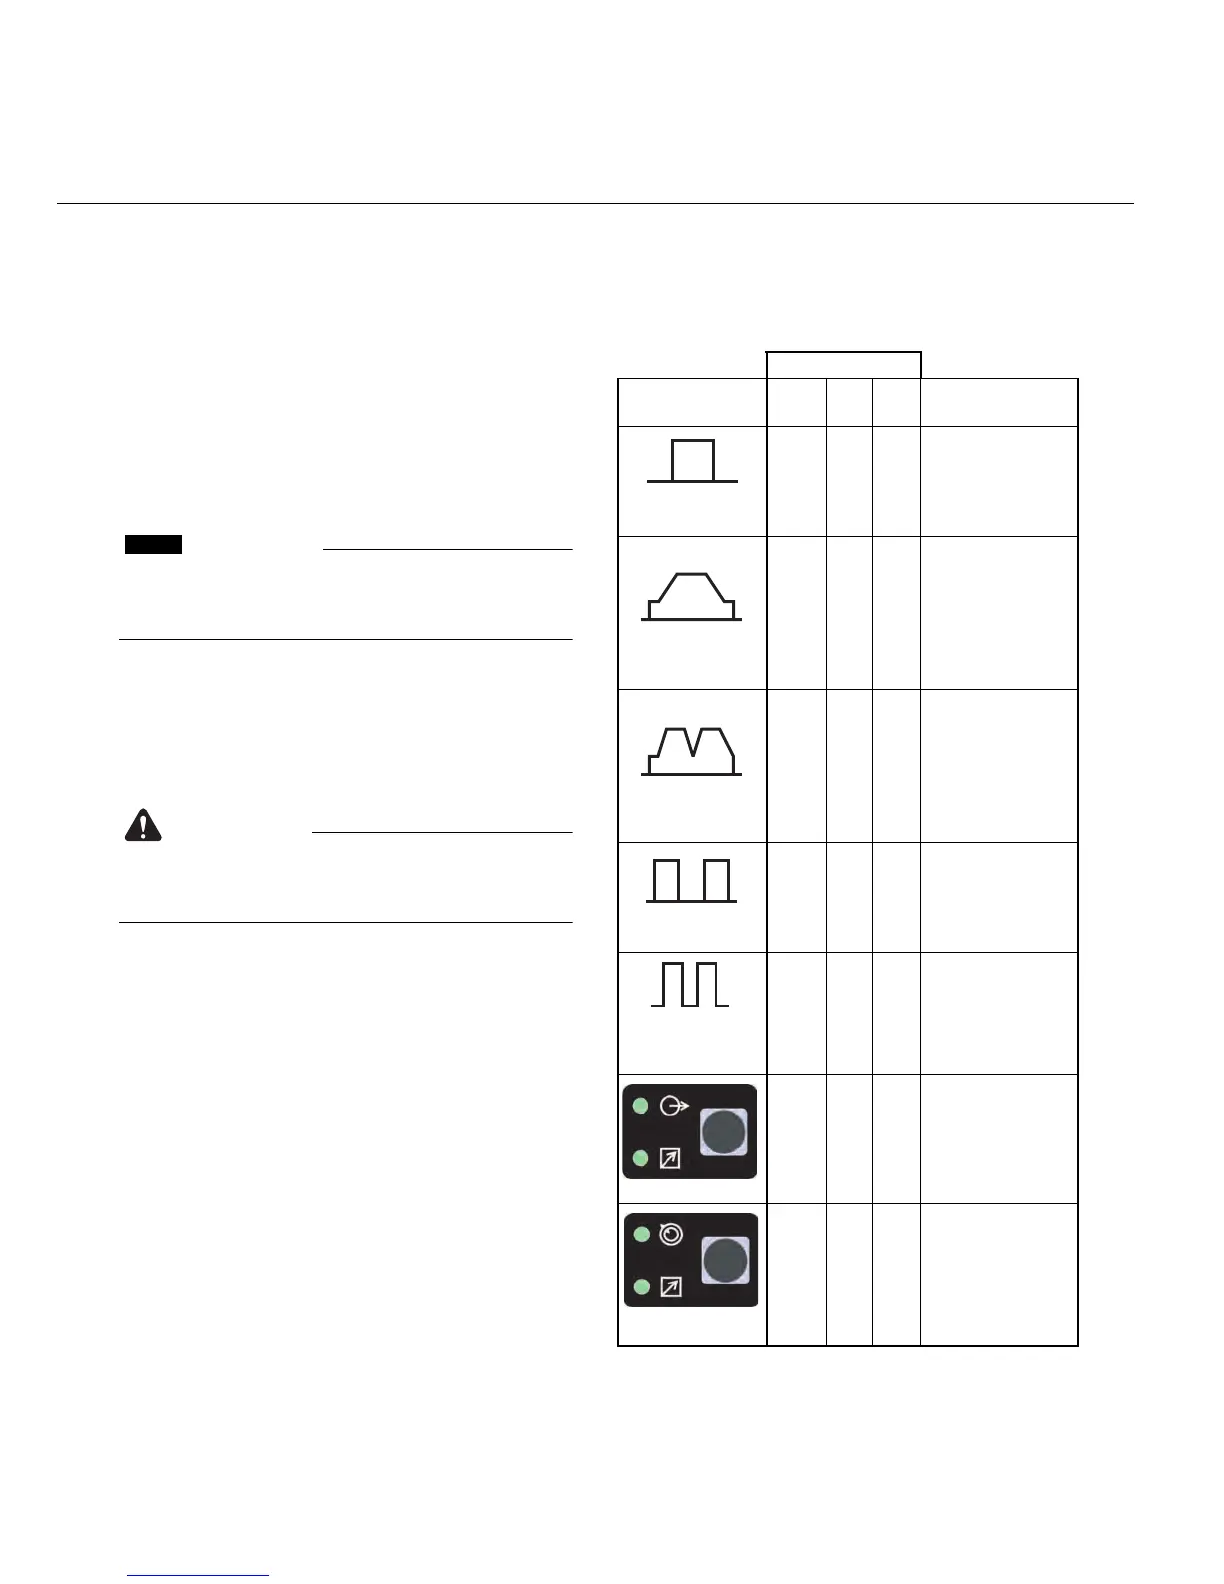
Weld Process selection for
ARC MASTER 300/400TS
and 300/400S
Table4-2:
Weld Process selection verses Weld Mode for
ARC MASTER 300/400TS and 300/400S
Weld Mode
Weld Process
Selection
STICK
HF
TIG
LIFT
TIG
Description
Yes Yes Yes
2T operation in
TIG Modes using
remote devices to
control contactor
& current.
No Yes Yes
4T operation in
TIG Modes with
crater fill using a
remote contactor
device to control
sequence.
(300/400TS only)
No Yes Yes
4T operation in
TIG Modes with
repeat operation
and crater fill
using a remote
contactor device.
(300/400TS only)
No Yes No
2T operation spot
welding in HF TIG
using a remote
contactor device.
(300/400TS only)
No Yes Yes
Pulse operation
in TIG Modes.
(300/400TS only)
Yes No Yes
Contactor
operation in Stick
Mode
Yes Yes Yes
Selects mode of
operation: Panel
or Remote
STD
SLOPE
REPEAT
SPOT
PULSE
ON/OFF
Contactor ON/OFF
Operation
PANEL/ REMOTE


 To Next Page