5 SET-UP FOR SMAW (STICK) AND GTAW (TIG)
5 – 1
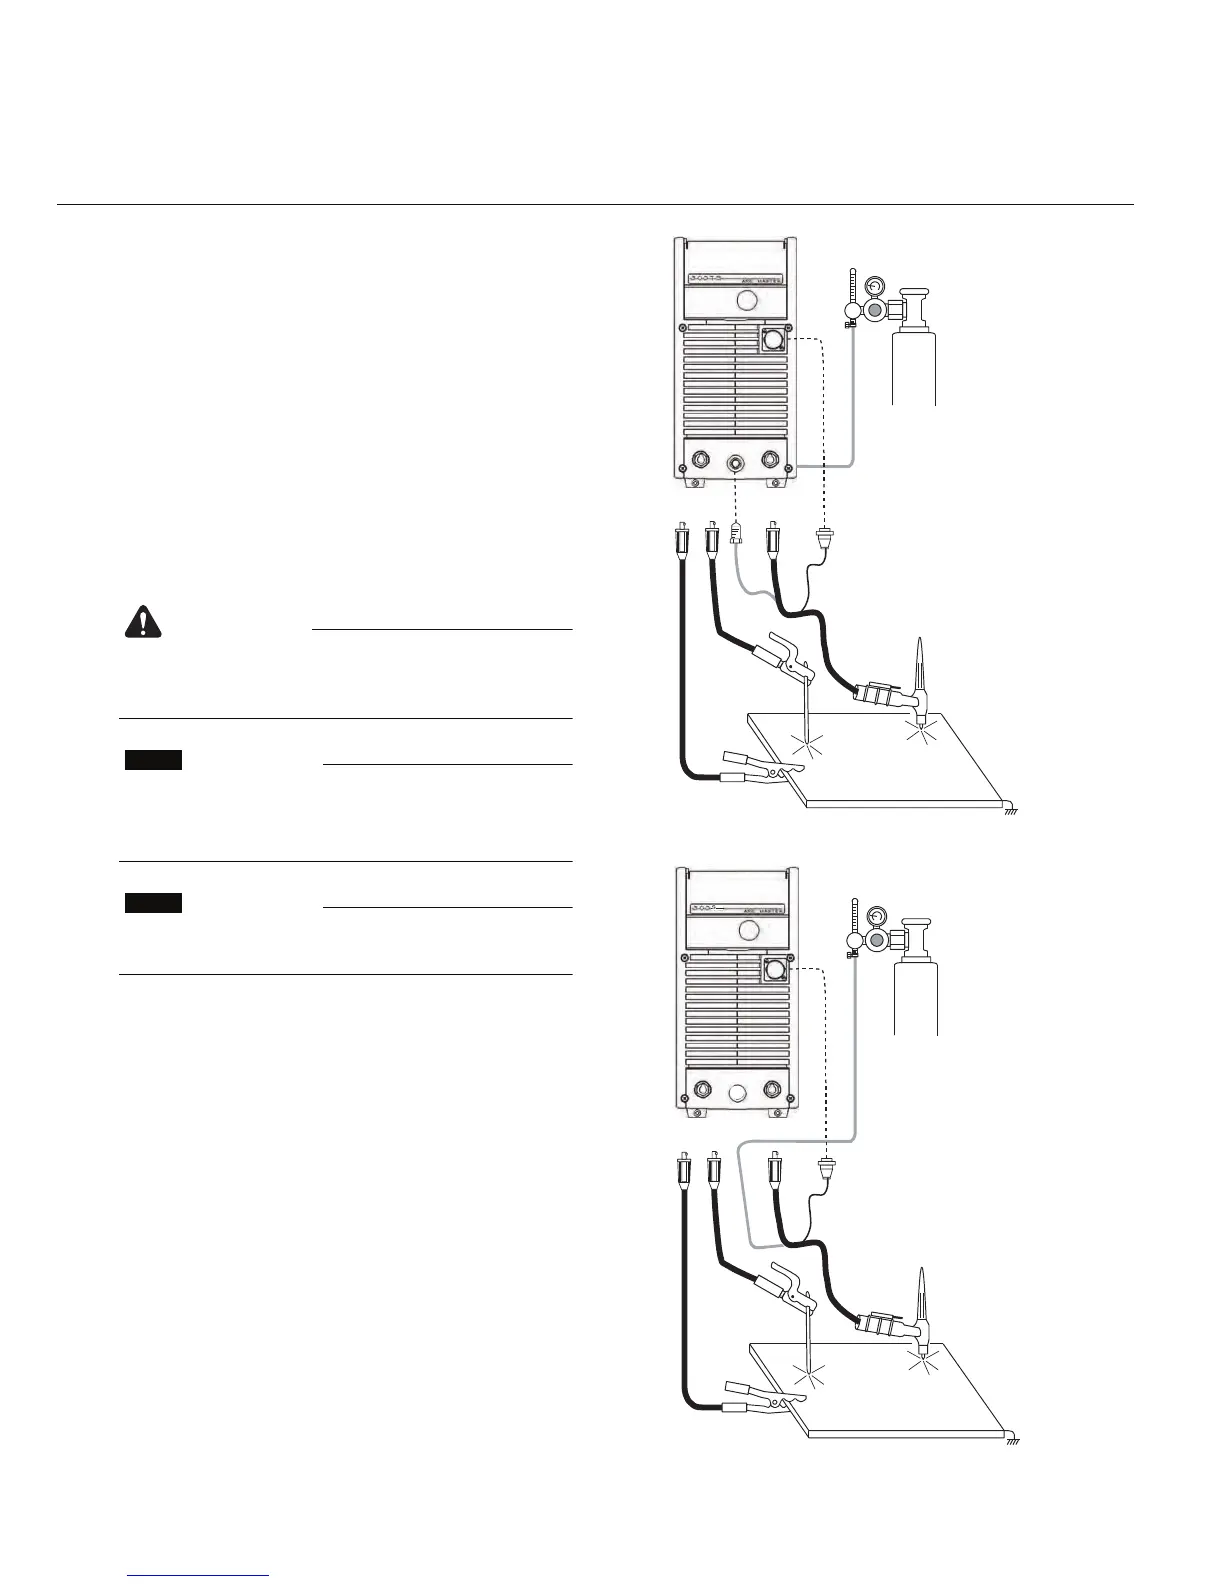
Conventional operating procedures apply when
using the Welding Power Source, i.e. connect work
lead directly to work piece and electrode lead is
used to hold electrode. Wide safety margins pro-
vided by the coil design ensure that the Welding
Power Source will withstand short-term overload
without adverse effects. Current delivered to the arc
is dependent on the welding arc voltage, and as
welding arc voltage varies between different classes
of electrodes, welding current at any one setting
would vary according to the type of electrode in use.
The operator should use the welding current range
values as a guide, then finally adjust the current
setting to suit the application.
WARNING
Before connecting the work clamp to the work and
inserting the electrode in the electrode holder make
sure the Primary power supply is switched off.
CAUTION
Remove any packaging material prior to use.
Do not block the air vents at the front or rear or
sides of the Welding Power Source.
CAUTION
DO NOT change the Weld Mode or Weld Process
Mode until after POST-FLOW time has finished.
Figure5-1: 300/400TS Set-up
Figure5-2: 300/400S Set-up


 To Next Page