300/400TS and 300/400S 8 BASIC TROUBLESHOOTING
8 – 4
Table 8-2-c: STICK Welding Problems (continued)
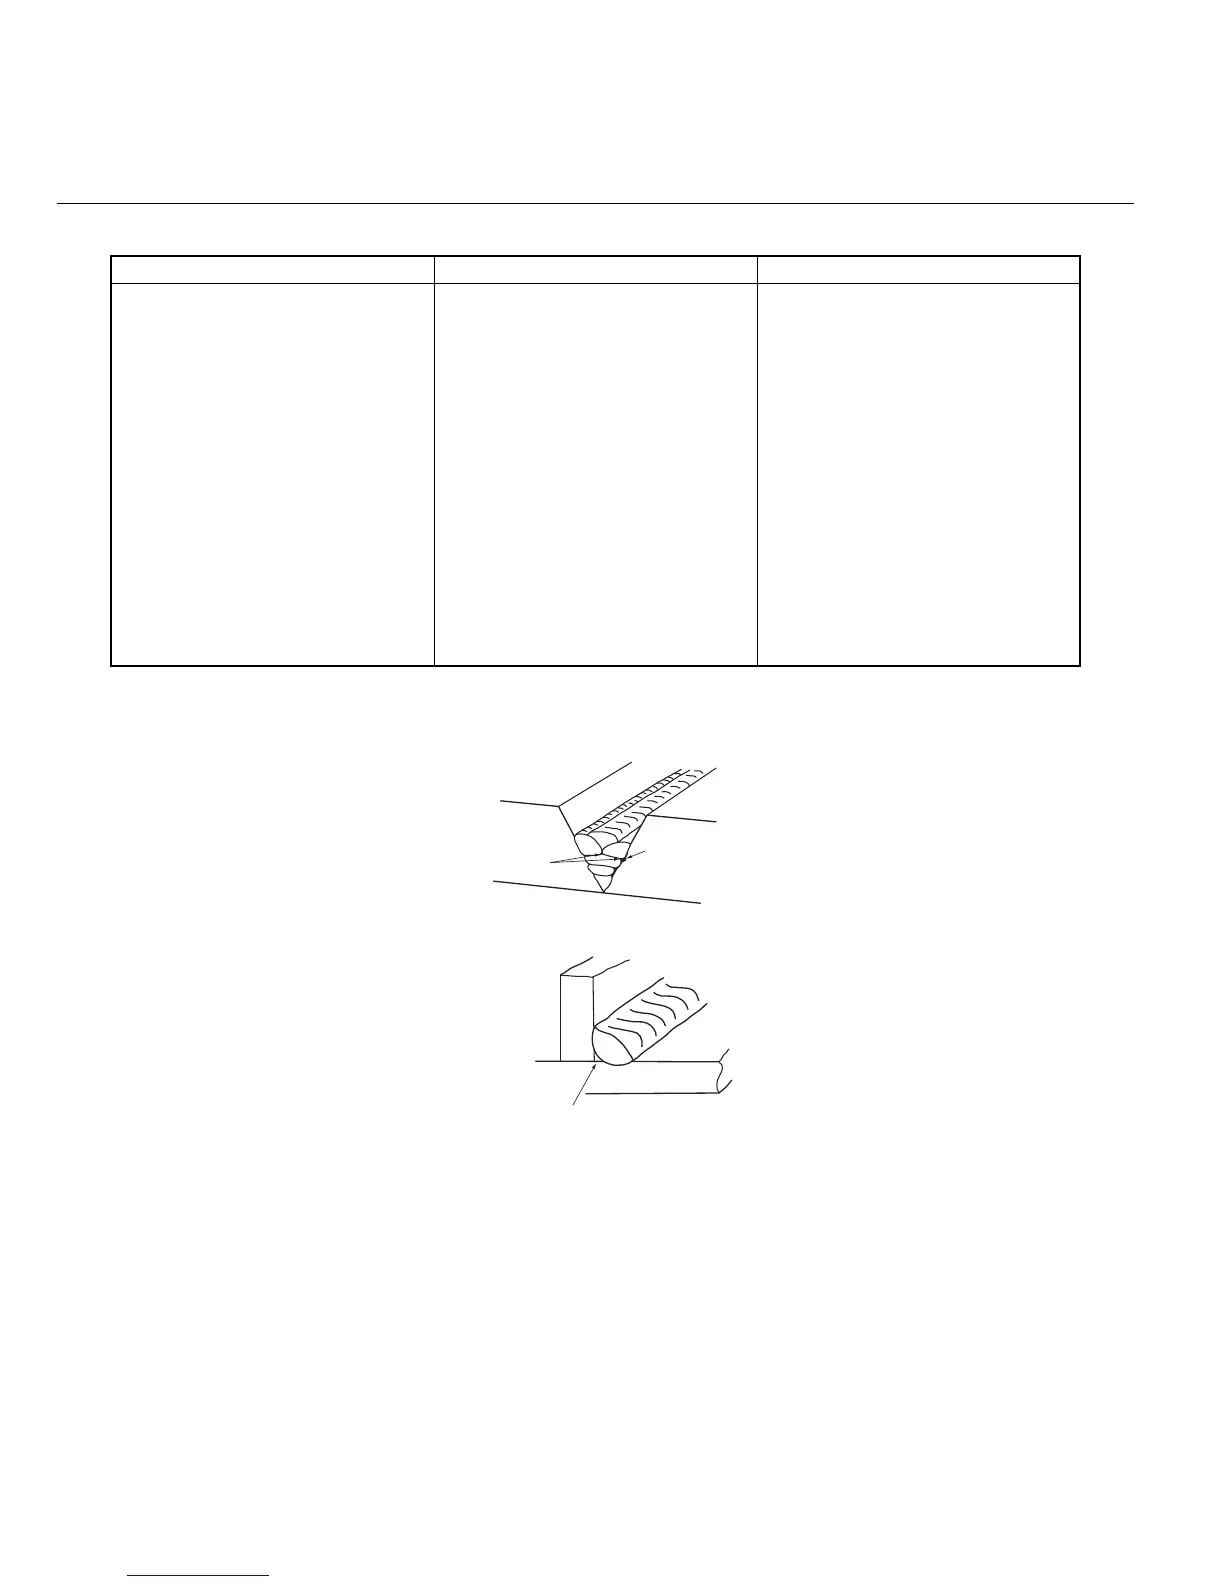
Figure8-3: Examples of slag inclusion
Description Possible Cause Remedy
5. Non-metallic particles are trapped
in the weld metal (slag inclusion).
A. Non-metallic particles may be
trapped in undercut from previous
run.
B. Joint preparation too restricted.
C. Irregular deposits allow slag to be
trapped.
D. Lack of penetration with slag
trapped beneath weld bead.
E. Rust or mill scale is preventing full
fusion.
F. Wrong electrode for position in
which welding is done.
A. If bad undercut is present, clean
slag out and cover with a run from a
smaller diameter electrode.
B. Allow for adequate penetration and
room for cleaning out the slag.
C. If very bad, chip or grind out
irregularities.
D. Use smaller electrode with
sufficient current to give adequate
penetration. Use suitable tools to
remove all slag from corners.
E. Clean joint before welding.
F. Use electrodes designed for
position in which welding is done,
otherwise proper control of slag is
difficult.
Not cleaned, or
incorrect electrode
Slag trapped in
undercut
Slag trapped in root


 To Next Page