Chapter 4 Control Function of Additional Axis
123
I Programming
1. Rapid traverse (Positioning): G90/91 G00 X_ Y_ Z_ A_;
2. Cutting feed: G90/91 G01 X_ Y_ Z_ A_ F_;
3. Skip function: G90/91 G31 X_ Y_ Z_ A_ F_;
4. Reference position return: G28/29/30 X_ Y_ Z_ A_ F_;
5. G92 coordinate setting: G92 X_ Y_ Z_ A_ ;
6. Manual/Step/MPG feed, Manual machine zero return.
Note: When there is no special explanation in the subsequent narration, the axis names of additional linear axes are
expressed with “A”.
z Explanations
1. When the additional linear axis rapidly moves or performs, it can be simultaneously specified
with any axes of X, Y and Z. Each axis may rapidly move at its customized speed.
2. When the additional linear axis is performed the cutting feed (G01) or used a skip function (G31),
it can be simultaneously specified with any axes of X, Y and Z. in this case, the linear axis does not has
an individual feedrate F but depend on each axis specified at a same time, which it is started or ended
together with the specified each axis; namely, the additional axis is shared with the basis three-axis
linkage.
3. The additional linear axis can not performed a circular arc cutting (G02/03), otherwise, the P/S
alarm may occur.
4. The pitch error of additional linear axis and the compensation function of inverse interval are
same as the basis three-axis.
4.6 Rotation Axis of The Additional Axis
z Input unit
Pulse equivalent of 980MDc’s rotary axis is set by No.187, maximum output pulse frequency is 2M.
When the selection is output based on the direction of pulse adding, it can be inputted a maximum
speed n=60*f/36000=833.33 (r./min.)
z Rotation axis speed
The feedrate of rotation axis is regarded the degree/min. as a unit. When the linear axis X, Y and Z is
performed a linear interpolation with the rotation axis, the speed specified with F (mm/min) is the compound
feedrate both X, Y and Z and the rotation axis.
Feedrate calculation: Calculate the required time when the feedrate is performed to the end; then, the
feedrate unit of rotation axis is changed into deg/min..
For example: G91 G01 X20.0 C40.0 F300.0;
The unit of C axis is switched into 40mm from the 40.0 degree. The required time to the end is:
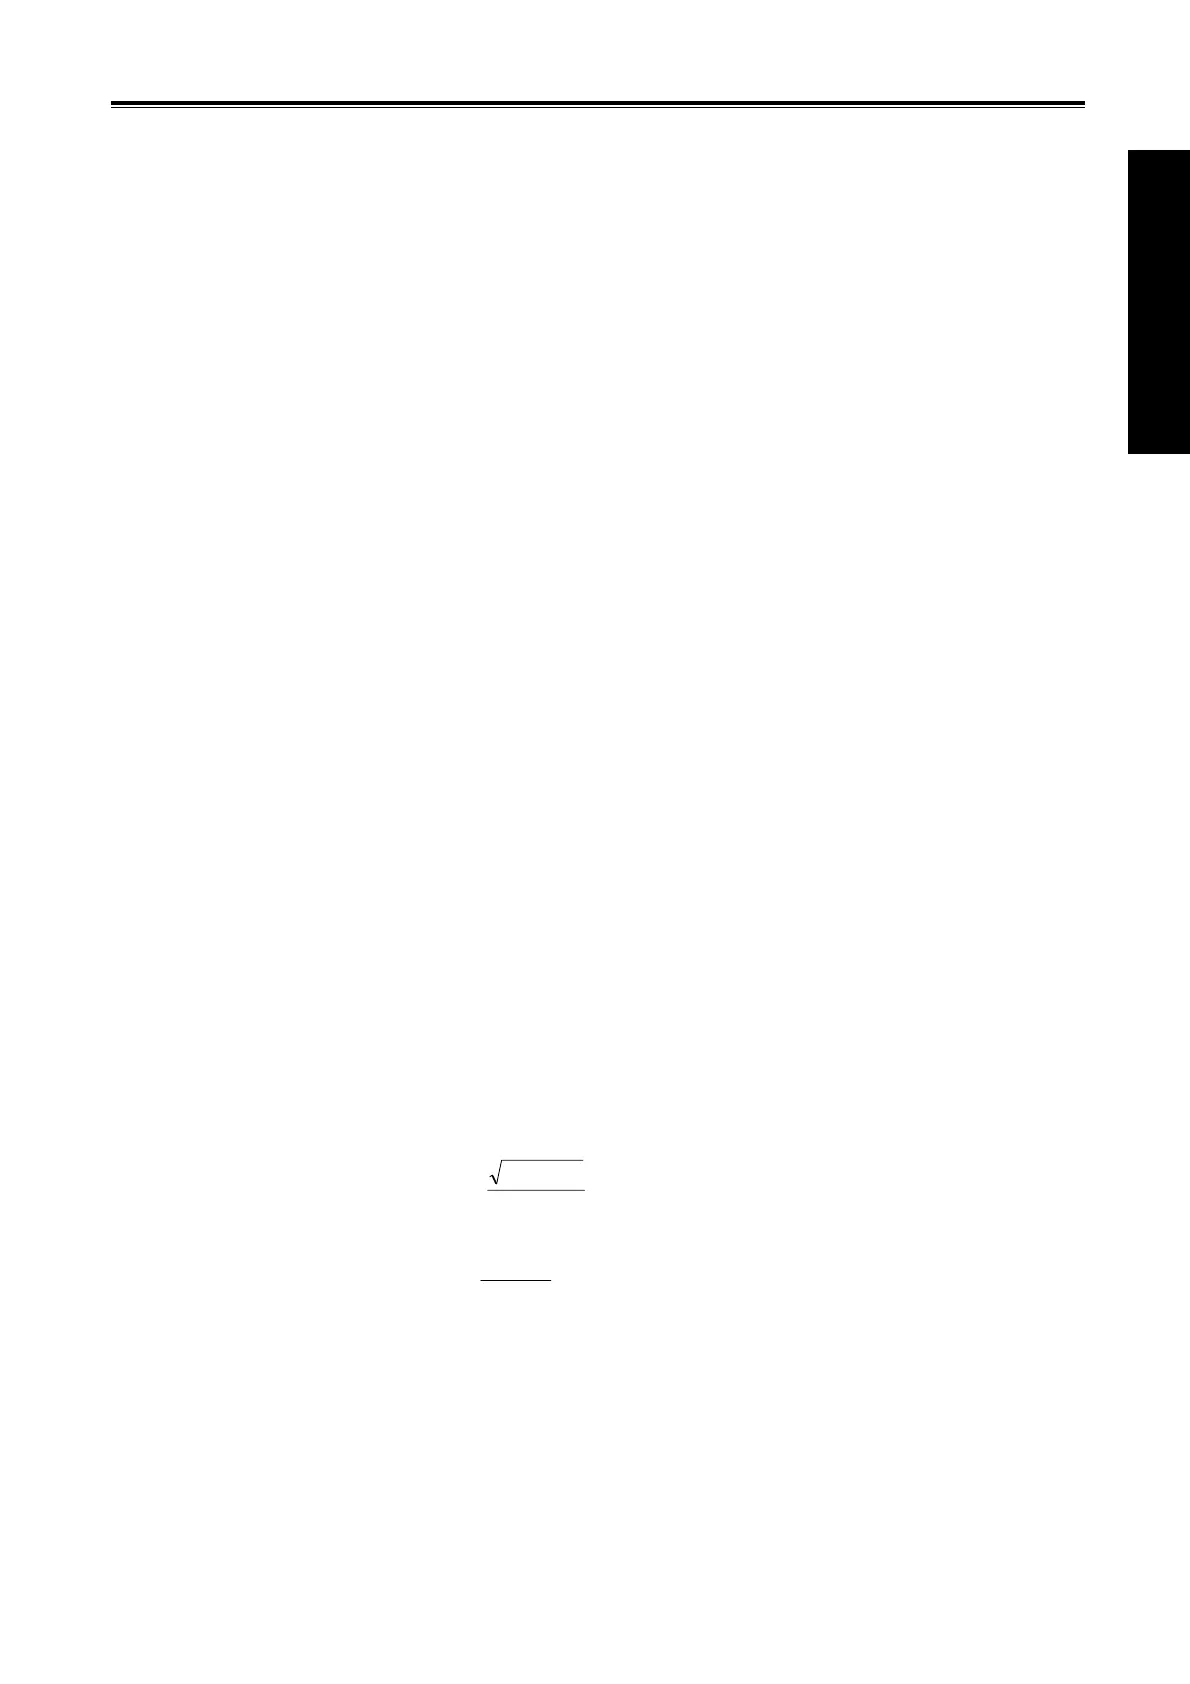
14907.0
300
4020
22
=
+
(min)
The speed of C axis is:
3.0268
14907.0
40
=
(deg/min)
Note: When there is no special explanation in the subsequent narration, the axis names of additional rotation axes
are expressed with “C”.
z The cycle function of rotation axis
The coordinate cycle function of the additional rotation axis setting is enabled, which can be
avoided the coordinate value is overflowed from the rotation axis; the coordinate value will be cycled
based on the setting value of data parameter No.1260 (the movement amount of each axis for the
rotation axis).
When the coordinate cycle function of the additional rotation axis setting is disabled, the


 To Next Page