GSK980MDc Milling CNC System User Manual
48
I Programming
G29 Y Only Y axis performs the command returning from the reference point
G29 Z Only Z axis performs the command returning from the reference point
G29 X Z Only X and Z axes perform the command returning from the reference point
G29 X Y Only X and Y axes perform the command returning from the reference point
G29 Y Z Only Y and Z axes perform the command returning from the reference point
G29 X Y Z
X, Y and Z perform the command returning from the reference point
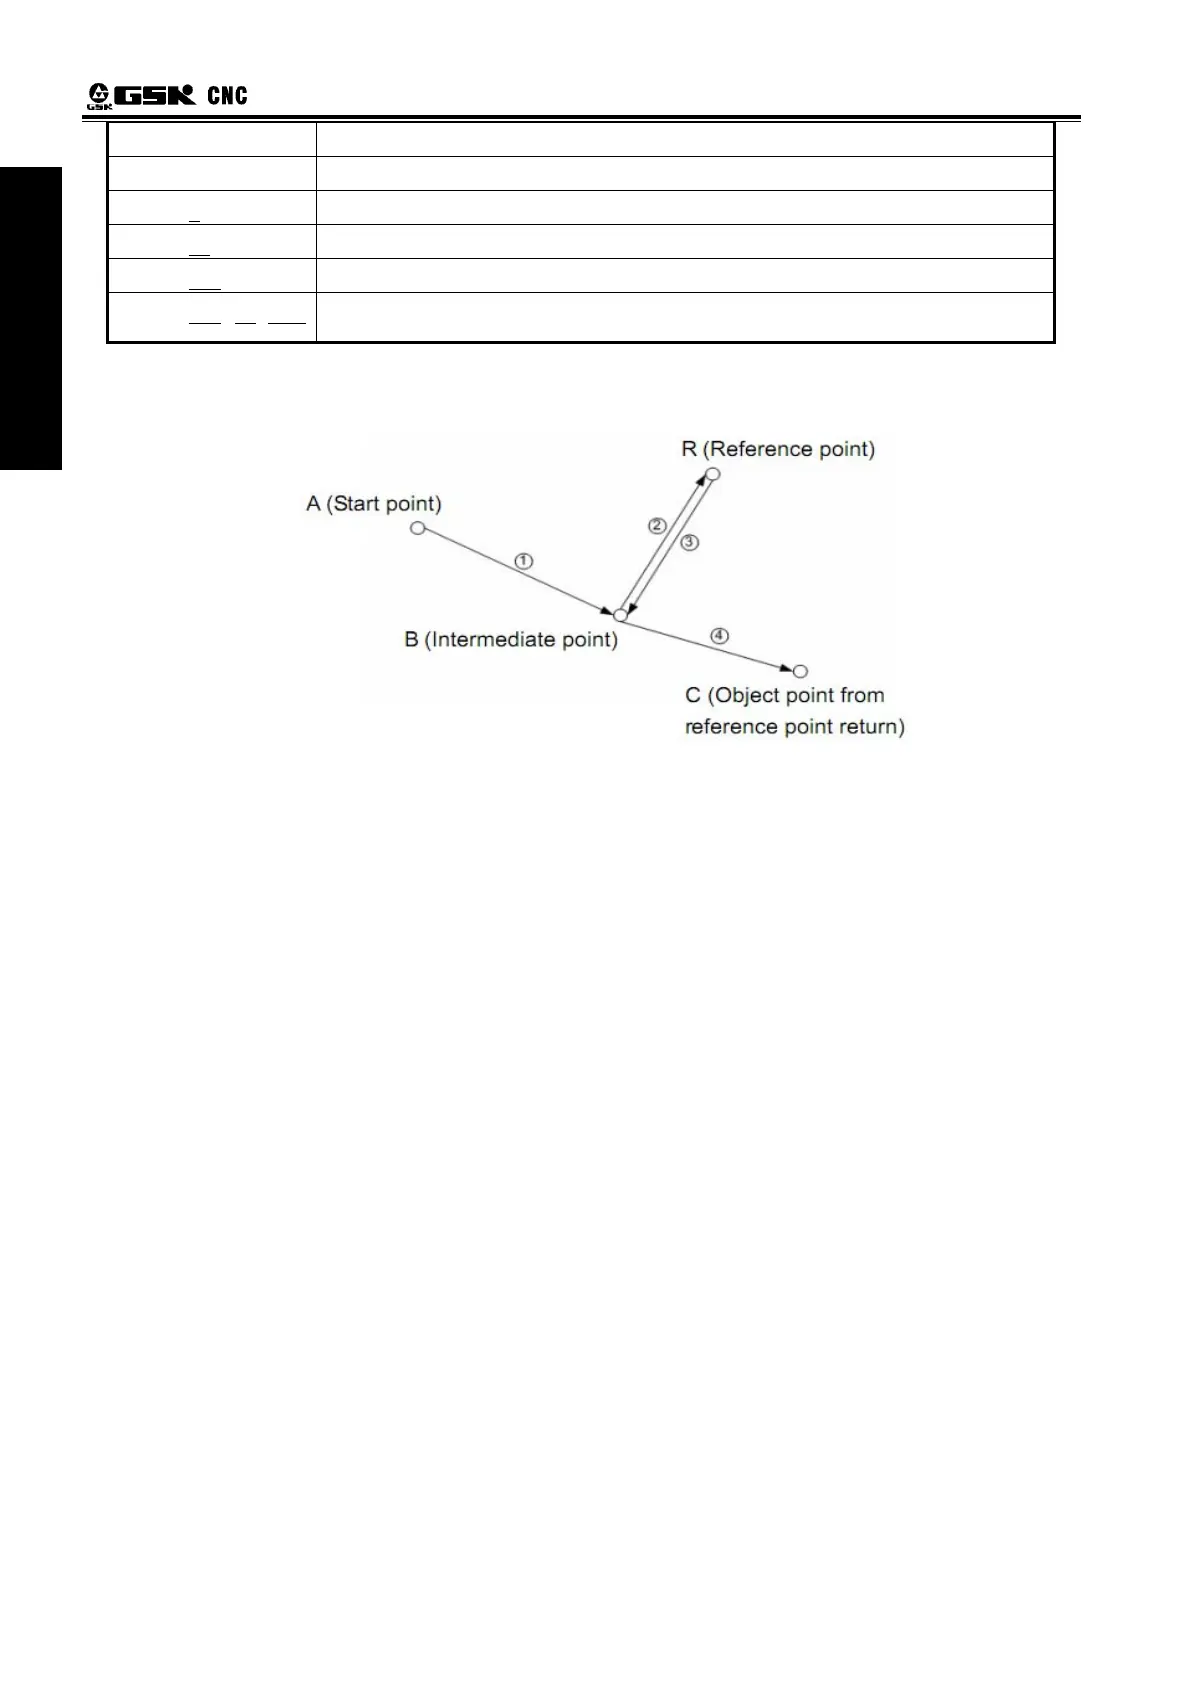
Process for command action:
(1) The command axis direction performs positioning at the intermediate point specified by G28 (from
point R
to B), the action is
①
→
.
②
(2) The positioning is performed from intermediate point to specified point (from point B to C), moving
to the intermediate and command point at a rapid feedrate, the action is ③→④.
Note 1:G29 is specified after G28, if an intermediate point is not specified by any of axes, the system alarm will be
generated.
Note 2: It is incremental distance against the intermediate point in G91 coordinate programming.
3.13 The 2nd, 3rd and 4th Reference Point Return G30
Reference point is a fixed point on the machine. By parameters (No.1240~No.1243) it can set four
reference points in the machine coordinate system.


 To Next Page