Chapter 3 G Command
31
I Programming
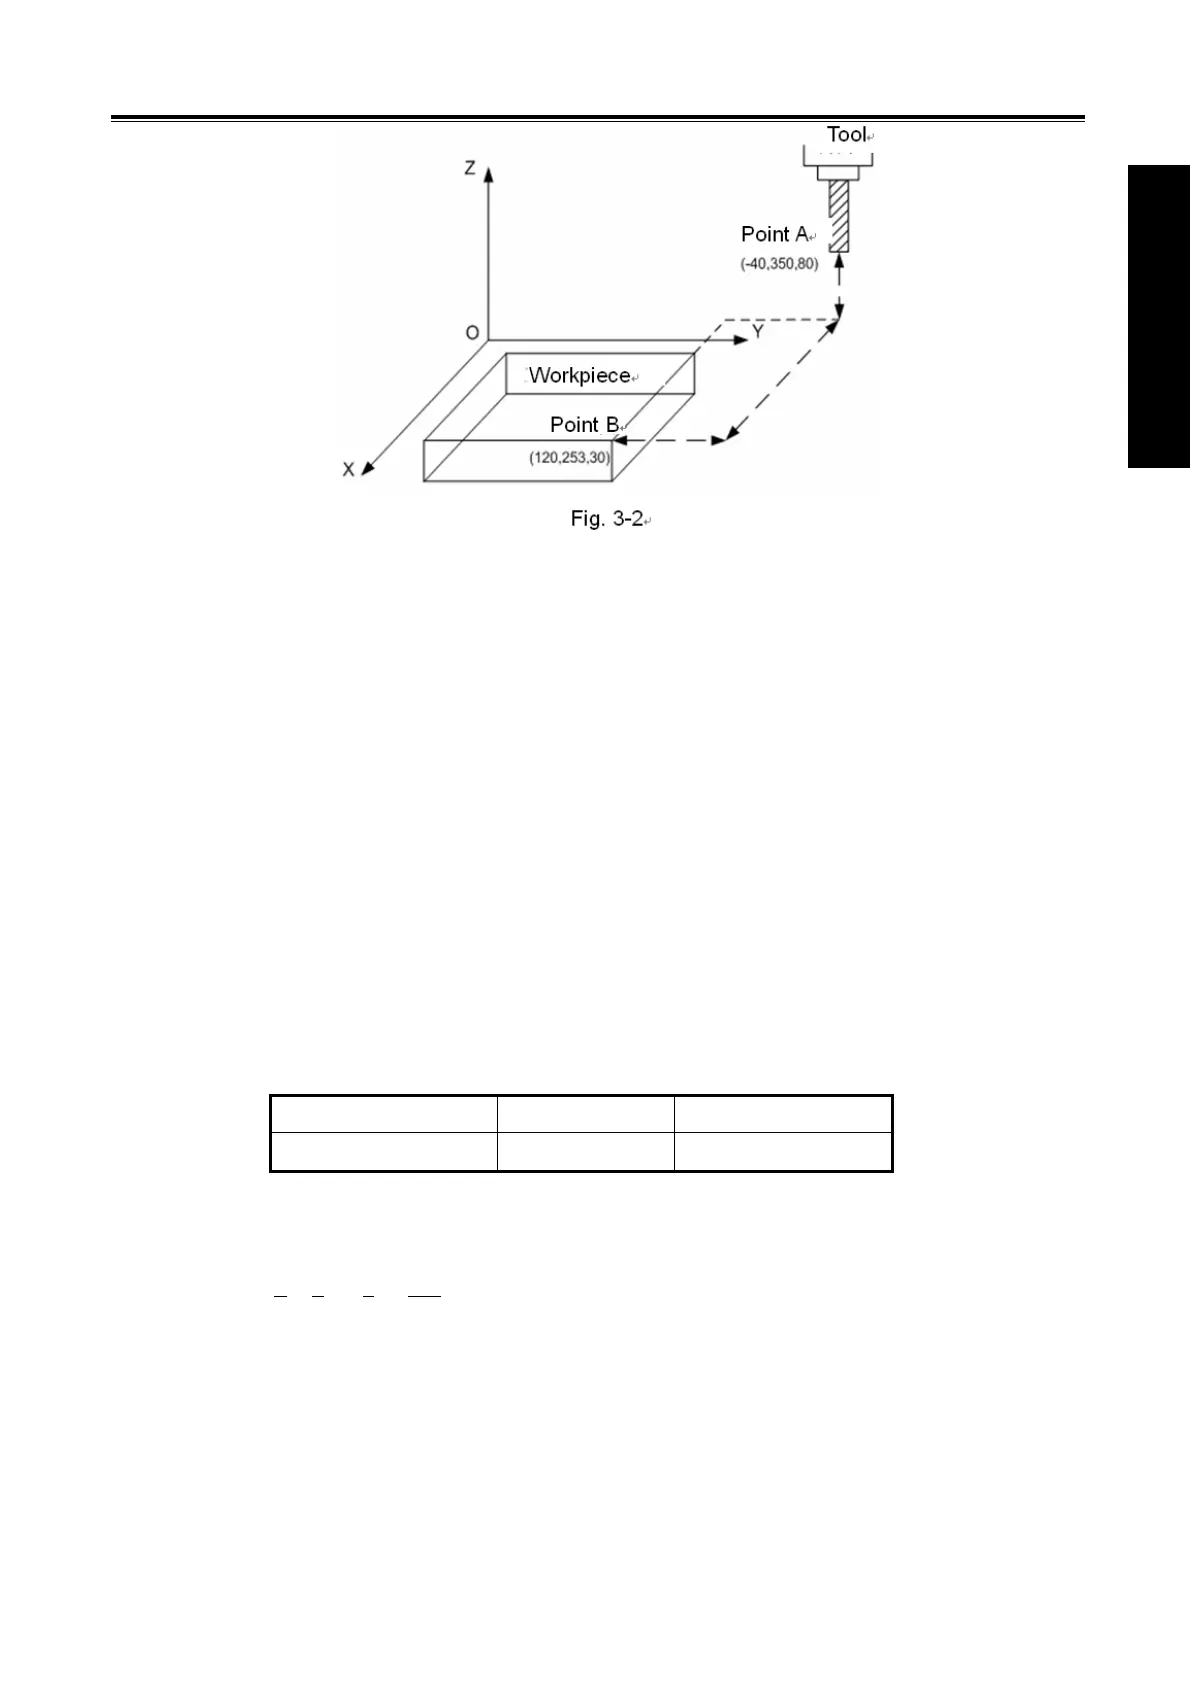
G90 G0 X120 Y253 Z30;
(absolute coordinate programming)
G91 G0 X160 Y-97 Z-50; (relative coordinate programming)
3.3 Linear Interpolation G01
Format: G01 X_Y_Z_F_;
Function: Movement path is a straight line from start to end points.
Explanation: G01, which is modal G command;
X, Y, Z:-99999999~99999999×least input increment;
X, Y and Z axes which one of them can be omitted or all of them can be omitted. When one
of them is omitted, it means that the coordinate value of start and end points are consistent.
The start and end points share the same position when they are omitted at the same time.
F command value is vector resultant speed of instantaneous rates in X, Y and Z axes
directions, the actual feedrate is the product of override and F command value;
F command value is invariable after it is performed till the new one is executed. The
following G command with F command word uses the same function.
The value range is indicated as follows:
Command function
G94 (mm/min) G95 (mm/rev)
Value range
1~15000 0~500
Command path figure:
The linear interpolation is performed from point O to point A:
G01 X α
Y β Z γ F f ;


 To Next Page