GSK980MDc Milling CNC System User Manual
30
I Programming
G111, G116, G117, G132, G133, G134
and G135
negative number
Delay time in G04 (s)
-99999999~99999999×least input
increment, absolute value of
negative number
Round-off
X
X axis coordinate value
-99999999~99999999×least input
increment
Round-off
Y
Y axis coordinate value
-99999999~99999999×least input
increment
Round-off
Z
Z axis coordinate value
-99999999~99999999×least input
increment
Round-off
3.2 Rapid Positioning G00
Format: G00 X Y Z ;
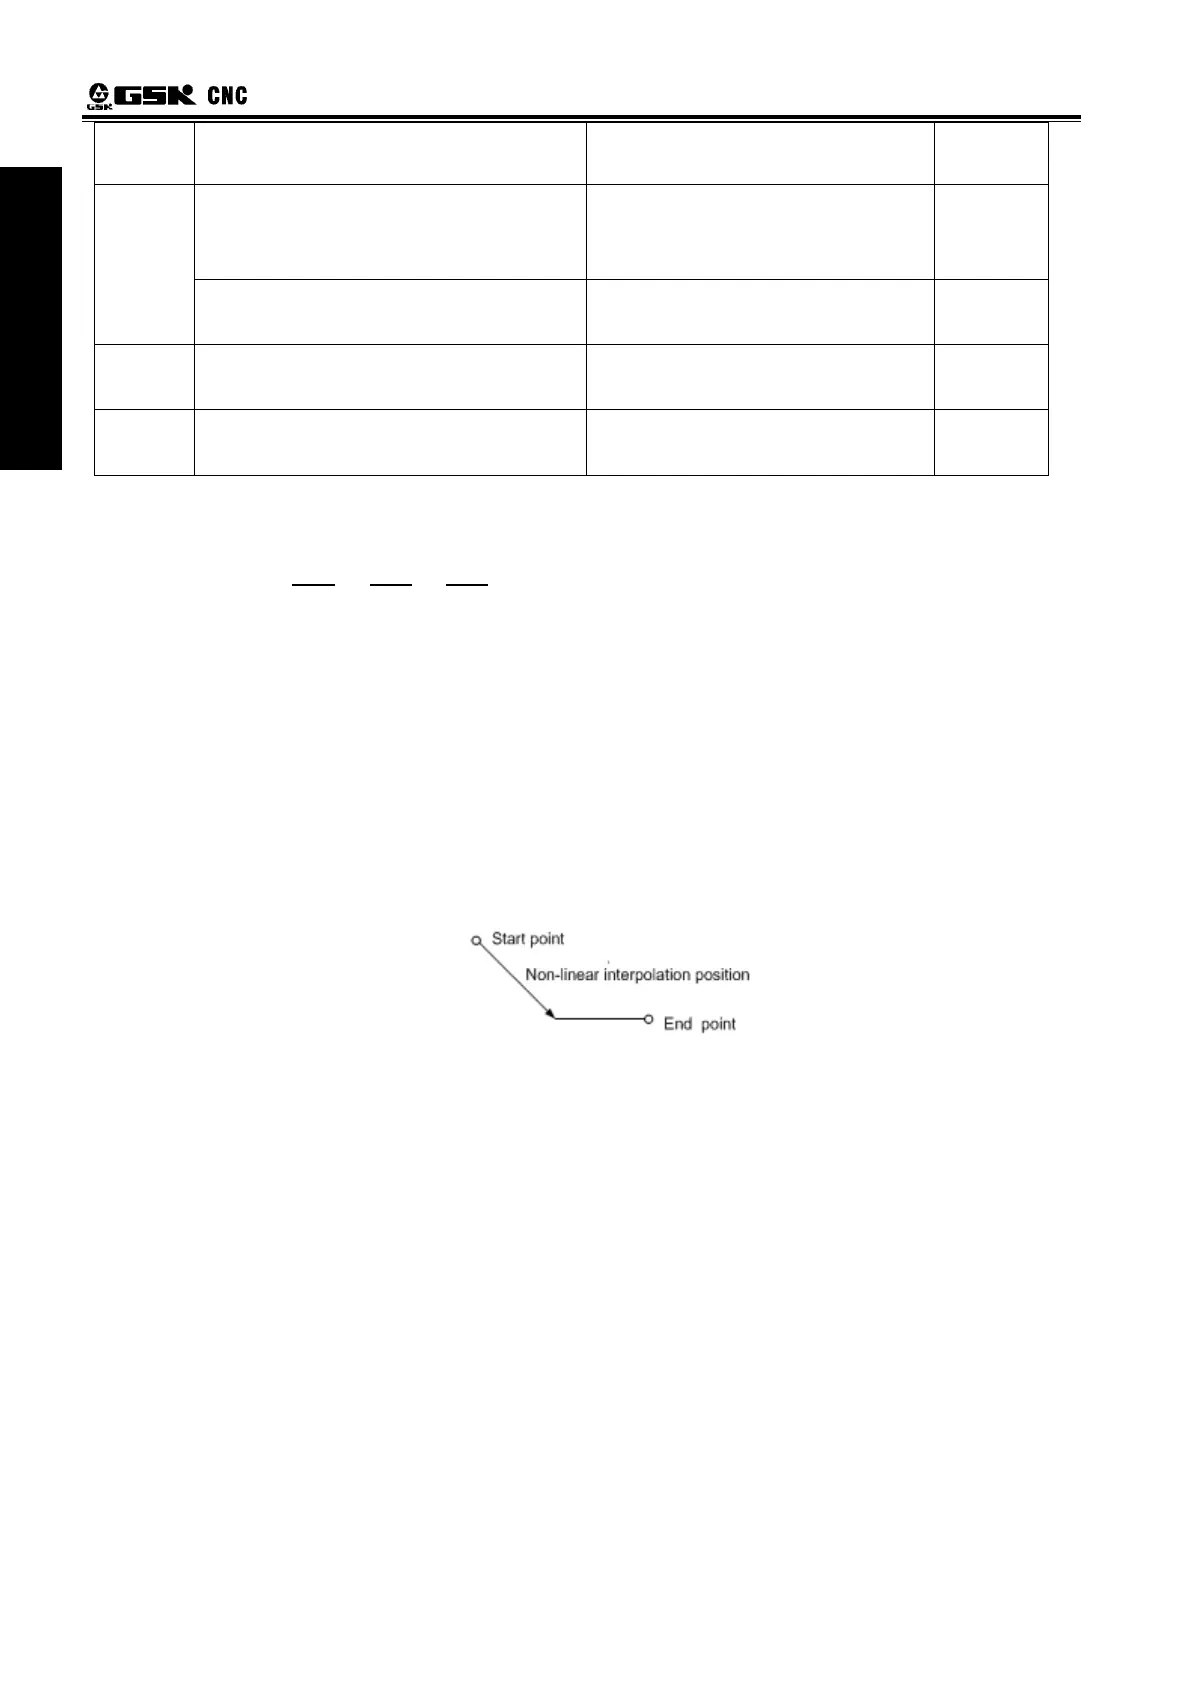
Function: X, Y and Z axes simultaneously move to end points from start at their rapid traverse rates.
See Fig.3-1. Two axes move at their respective speeds, the short axis arrives at the end firstly, the
long axis moves the rest of distance independently, and their resultant paths are possibly not linear.
Explanation: G00, which is initial G command;
X, Y, Z:-99999999~99999999×least input increment;
X, Y and Z axes, one of them can be omitted or all of them can be omitted. When one of
them is omitted, it means that the coordinate value of start and end points are same. The
start and end points share the same position when they are omitted at the same time.
Command path figure:
Tool positions at the rapid traverse rate independently for each axis. Usually, the tool path is not linear.
Fig. 3-1
X, Y and Z axes are separately set by the system data parameter No. 022 at their
rapid traverse rate, the actual traverse rate can be modified by the rapid override keys on the machine
panel.
Speed in dry run mode is limited by values set each axis’s max. rapid traverse speed parameter
(No.022).
The rapid traverse acceleration or deceleration time constant of X, Y and Z axes are set by the system
data parameter No. 023.
Example: tool traverses from point A to point B. See Fig.3-2.


 To Next Page