Chapter 3 G Command
63
I Programming
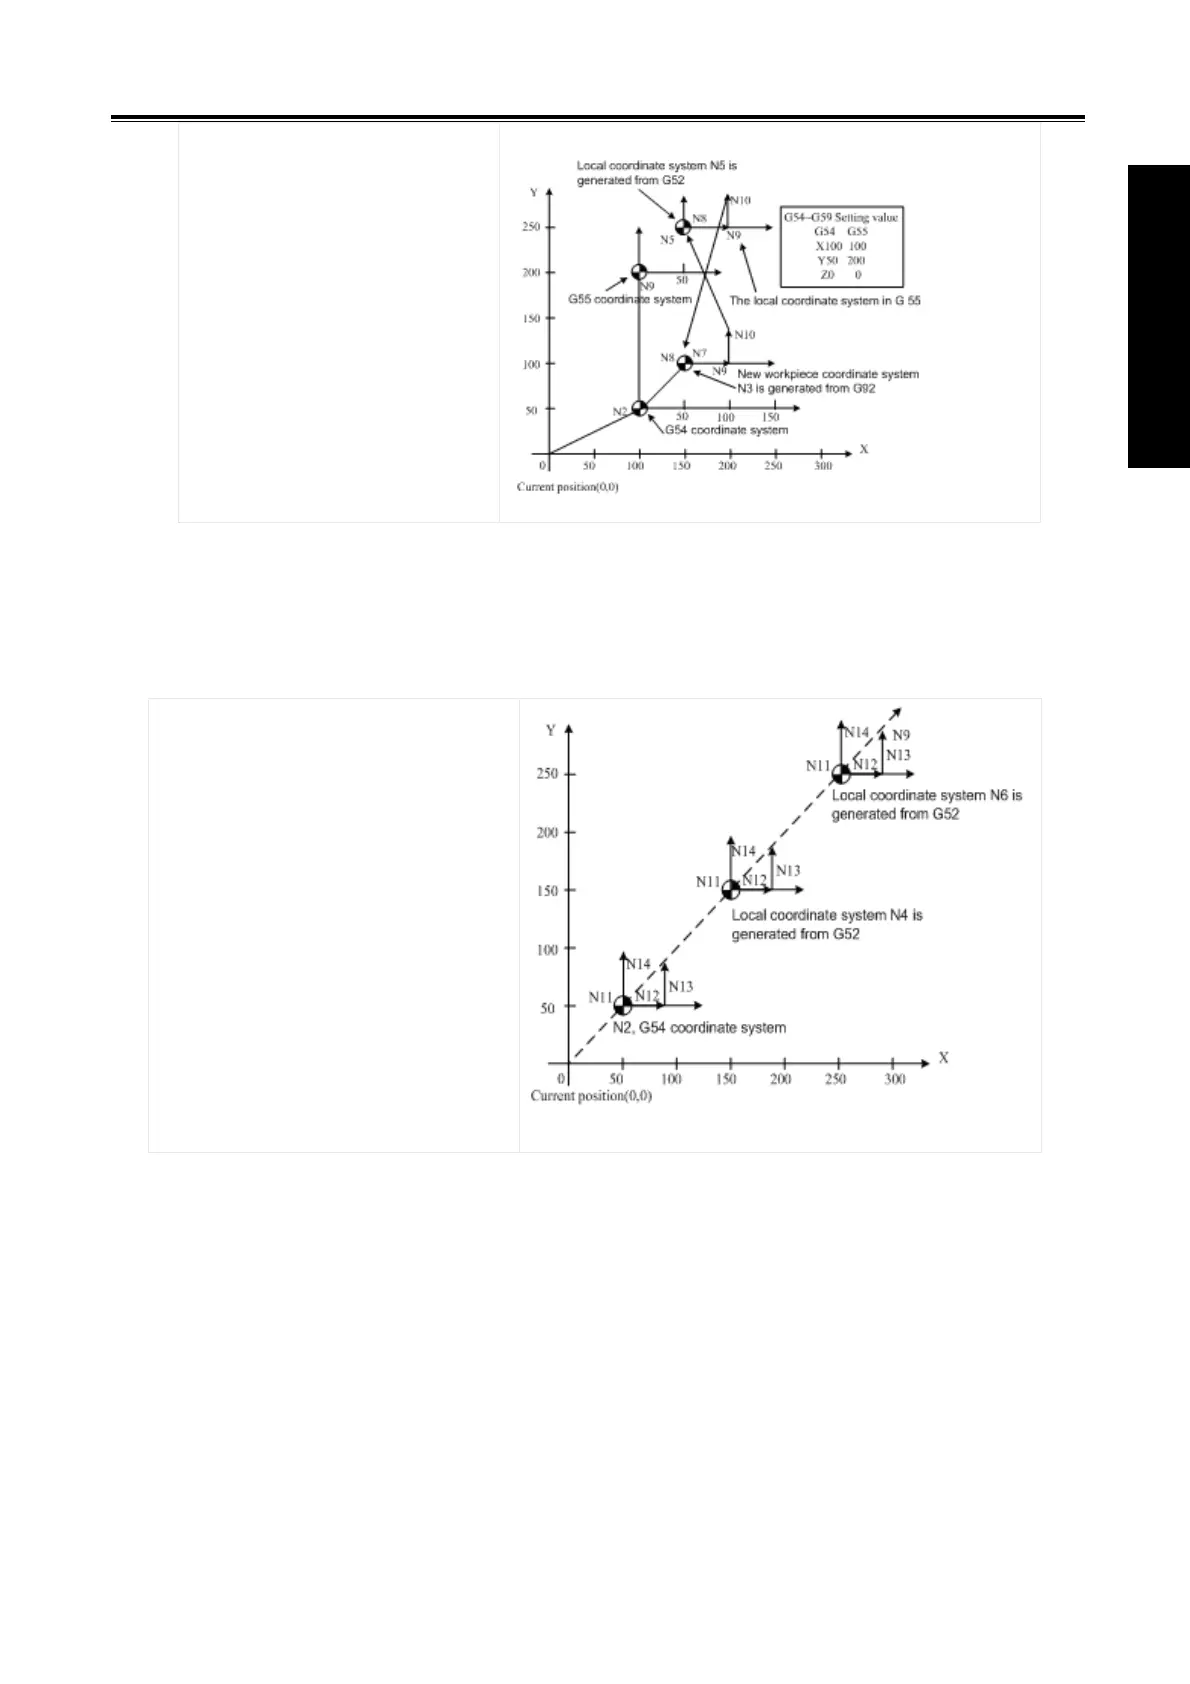
N1 G28 X0 Y0 Z0;
N2 G90 G54 G00 X0 Y0;
N3 G52 X50 Y50;
N4 M98 P1234;
N5 G90 G55 G00 X0 Y0;
N6 M98 P1234;
N7 G90 G54 G00 X0 Y0;
O1234 (Subprogram)
N8 G00 X0 Y0;
N9 G01 X50;
N10 Y50 M99;
Multiple local coordinate systems in the workpiece coordinate system
The local coordinate system generated from the N8 block in the brackets is consistent with the
workpiece coordinate G54, which is the same with the result after (N8 block) is cancelled in the local
coordinate system.
Notes
z When the parameter No.542 ZCL is set to 1, the local coordinate system of the axis is cancelled in the
process of reference return.
G52 a0;(a is the axis return to the reference point)
z The workpiece coordinate system and the machine coordinate system are not changed by setting the
local coordinate system.
z Parameter setting determines whether cancel the local coordinate system after reset. When the
parameter No.542 RLC is set to 1, all local coordinate systems of the workpiece coordinate system are
cancelled.
z When the workpiece coordinate system is set by specifying command G92, the local coordinate
N1 G28 X0 Y0 Z0;
N2 G90 G54 G00 X0 Y0;
N3 M98 P1234;
N4 G52 X100 Y100;
N5 M98 P1234;
N6 G52 X200 Y200;
N7 M98 P1234;
N8 G52 X0 Y0;
(N8 G91 G52 X-200 Y-200;)
O1234 (Subprogram)
N11 G00 X0 Y0;
N12 G01 X50;
N13 Y50;
N14 X0 Y0 M99;


 To Next Page