5238-E P-262
SECTION 11 PROGRAMMING FOR SIMULTANEOUS 4-AXIS CUTS (2S Model)
4. Programming Example
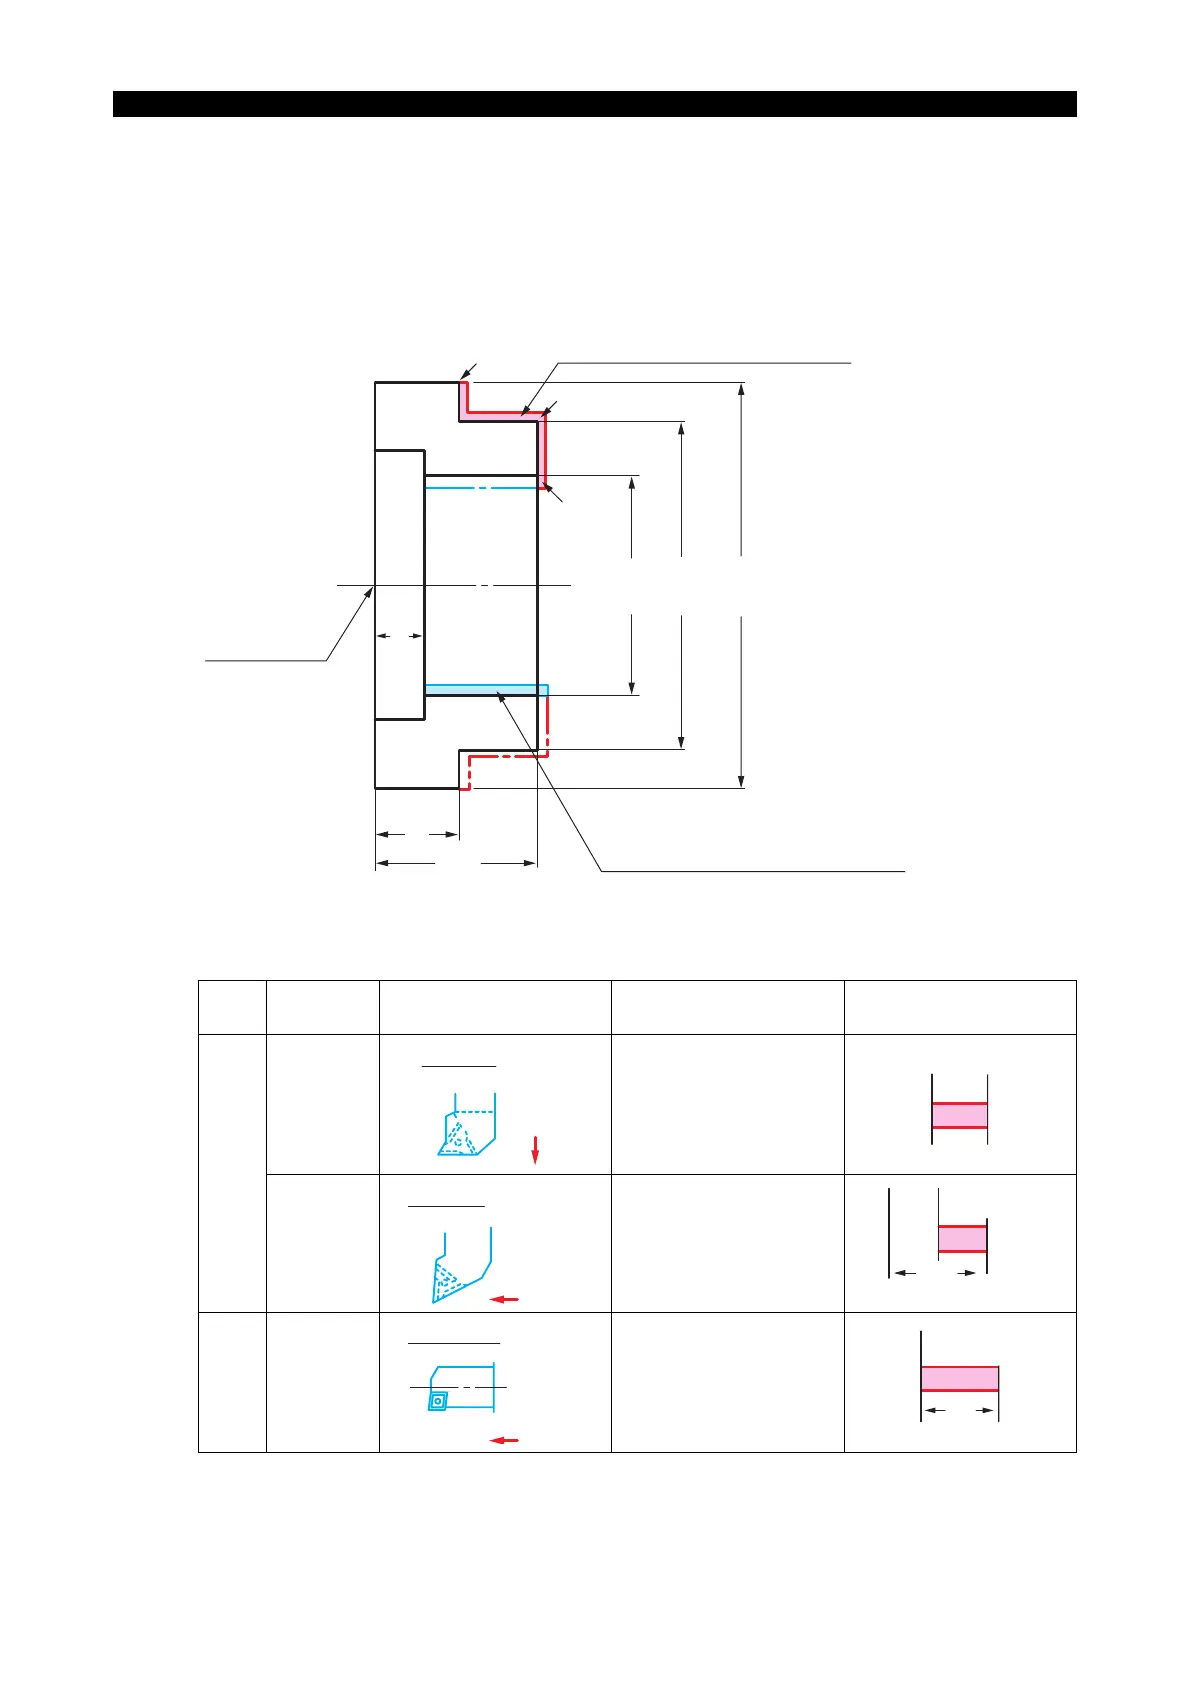
<Workpiece Dimensions>
LE33013R0301300070001
<Tooling and Cutting Conditions>
Material : S45C (JIS, carbon steel)
Stock : 3mm (in radius)
Turre
t
Tool No. Cutting Tool Cutting Conditions Cutting Time
A
T0101
Cutting speed:
120 to 65 m/min.
Depth of cut: 3 mm
Feedrate: 0.35 mm/rev.
T0202
Cutting speed: 95 m/min.
Depth of cut: 3 mm
Feedrate: 0.4 mm/rev.
B T0101
Cutting speed: 65 m/min.
Depth of cut: 3 mm
Feedrate: 0.25 mm/rev.
1C
1C
1C
20
30
60
Part to be cut with tools on rear turret
Program zero
Part to be cut with tools on front turret
80 φ
120 φ
150 φ
Facing
Upset tool
40
seconds
OD turning
Upset tool
68
seconds
28 seconds
ID turning
Normal tool
63
seconds


 To Next Page