ENGINE
L3301, L3901, L4701, WSM
1-S65
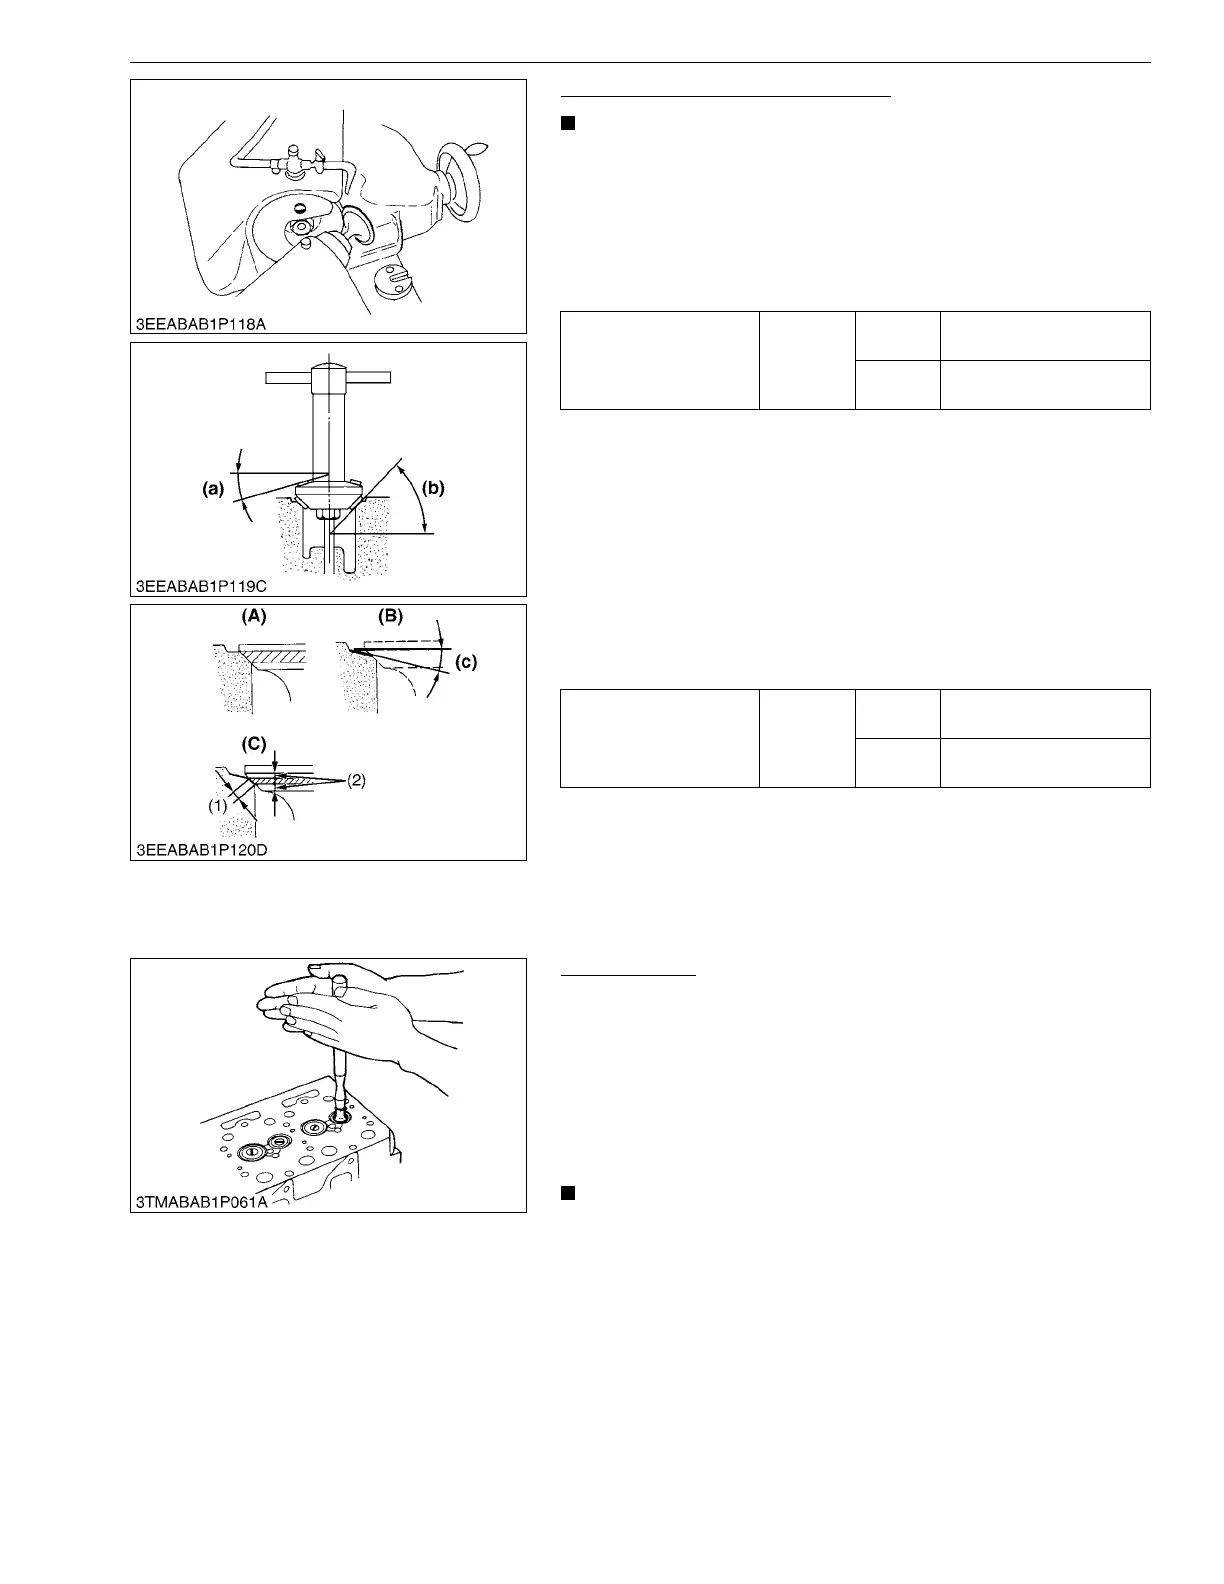
Correction of Valve and Valve Seat
• Before you correct the valve and seat, check the valve stem
and measure the I.D. of the valve guide section. Repair
them if necessary.
• After you correct the valve seat, be sure to check the valve
recessing.
1) Correction of valve
1. Correct the valve with a valve refacer.
2) Correction of valve seat
1. Slightly correct the seat surface with a 1.0 rad (60 °) or 0.79 rad
(45 °) valve seat cutter.
2. Correct the seat surface with a 0.52 rad (30 °) or 0.26 rad (15 °)
valve seat cutter. The width must be near the specified valve
seat width (2.12 mm, 0.0835 in.).
3. After you correct the seat, check that the valve seating is flat.
Apply a thin layer of compound between the valve face and
valve seat, and lap them with a valve lapping tool.
4. Check the valve seating with Prussian Blue. The valve seating
surface must show good contact on all sides.
9Y1211012ENS0077US0
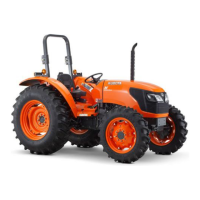
Valve Lapping
1. Apply the compound equally to the valve lapping surface.
2. Put the valve into the valve guide. Lap the valve on its seat with
a valve lapping tool.
3. After you lap the valve, clean away the compound and apply oil,
then lap the valve again with oil.
4. Apply Prussian Blue to the contact surface to measure the
seated rate.
5. If the seated rate is less than 70 %, lap the valve again.
• After you complete the valve lapping and assemble the
valve, check the valve recessing and adjust the valve
clearance.
9Y1211012ENS0078US0
Valve face angle
Factory
specifica-
tion
Intake
0.79 rad
45 °
Exhaust
0.79 rad
45 °
Valve seat angle
Factory
specifica-
tion
Intake
0.79 rad
45 °
Exhaust
0.79 rad
45 °
(1) Valve Seat Width
(2) Identical Dimensions
(A) Check the Contact
(B) Correct Seat Width
(C) Check the Contact
(a) 0.26 rad (15 °) or 0.52 rad (30 °)
(b) 0.79 rad (45 °) or 1.0 rad (60 °)
(c) 0.52 rad (30 °) or 0.26 rad (15 °)



 To Next Page