The input signal may be applied to I1, for example, and the output signal is chosen as output 1. The motor velocity
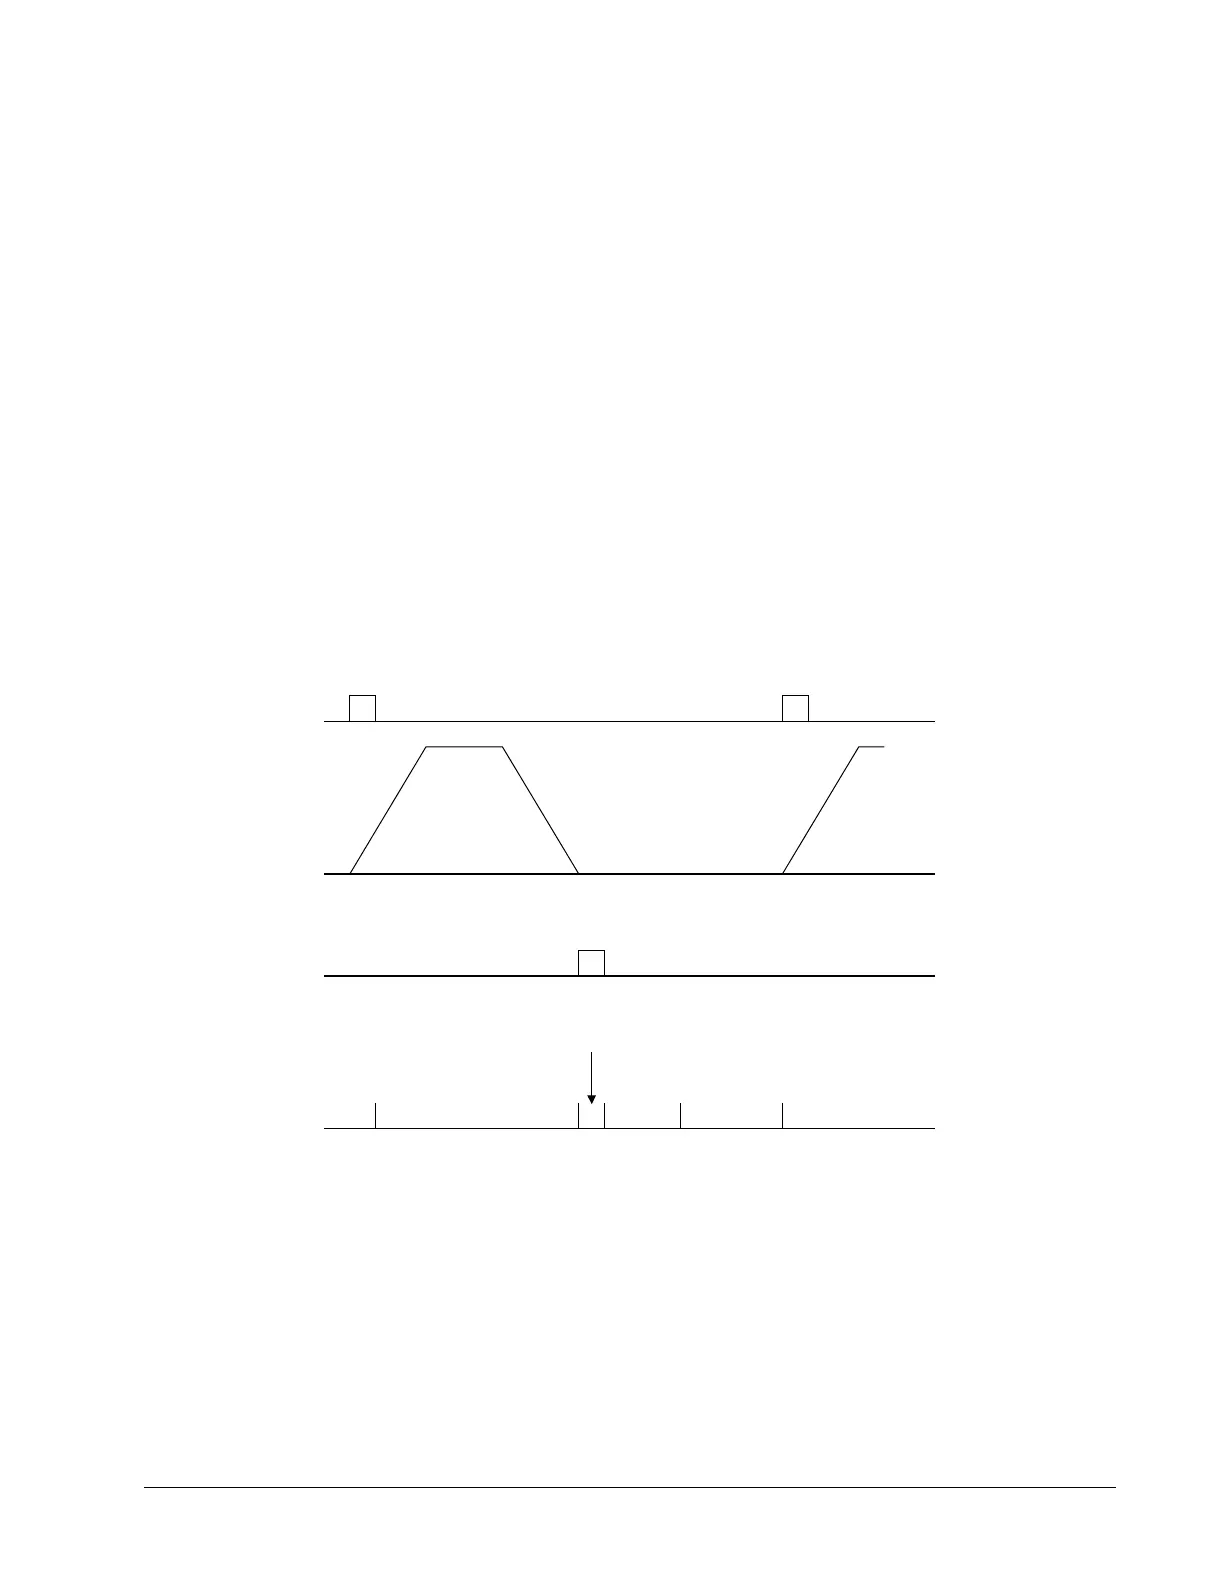
profile and the related input and output signals are shown in Fig. 7.1.
The program starts at a state that we define as #A. Here the controller waits for the input pulse on I1. As soon as
the pulse is given, the controller starts the forward motion.
Upon completion of the forward move, the controller outputs a pulse for 20 ms and then waits an additional 80 ms
before returning to #A for a new cycle.
INSTRUCTION FUNCTION
#A Label
AI1 Wait for input 1
PR 6370 Distance
SP 3185 Speed
BGX Start Motion
AMX After motion is complete
SB1 Set output bit 1
WT 20 Wait 20 ms
CB1 Clear output bit 1
WT 80 Wait 80 ms
JP #A Repeat the process
START PULSE I1
MOTOR VELOCITY
OUTPUT PULSE
TIME INTERVALS
move
output
wait ready move
Figure 7.1 - Motor Velocity and the Associated Input/Output signals
X-Y Table Controller
An X-Y-Z system must cut the pattern shown in Fig. 7.2. The X-Y table moves the plate while the Z-axis raises and
lowers the cutting tool.
The solid curves in Fig. 7.2 indicate sections where cutting takes place. Those must be performed at a feed rate of 1
inch per second. The dashed line corresponds to non-cutting moves and should be performed at 5 inch per second.
The acceleration rate is 0.1 g.
DMC-40x0 User Manual Chapter 7 Application Programming • 170


 To Next Page