4. Commands
133
ML-2050A/2051A/2150A
Chapter 5 Laser Welding by External Communication Control (RS-485 CONTROL)
Introduction Part
Installation and
Preparation Part
Operating Part Maintenance Part Appendixes
m5 Unused (xed to □)
ACK or NAK
Valid only at external communication control. If there is any setting that
cannot be changed, all are invalidated and [NAK] is returned.
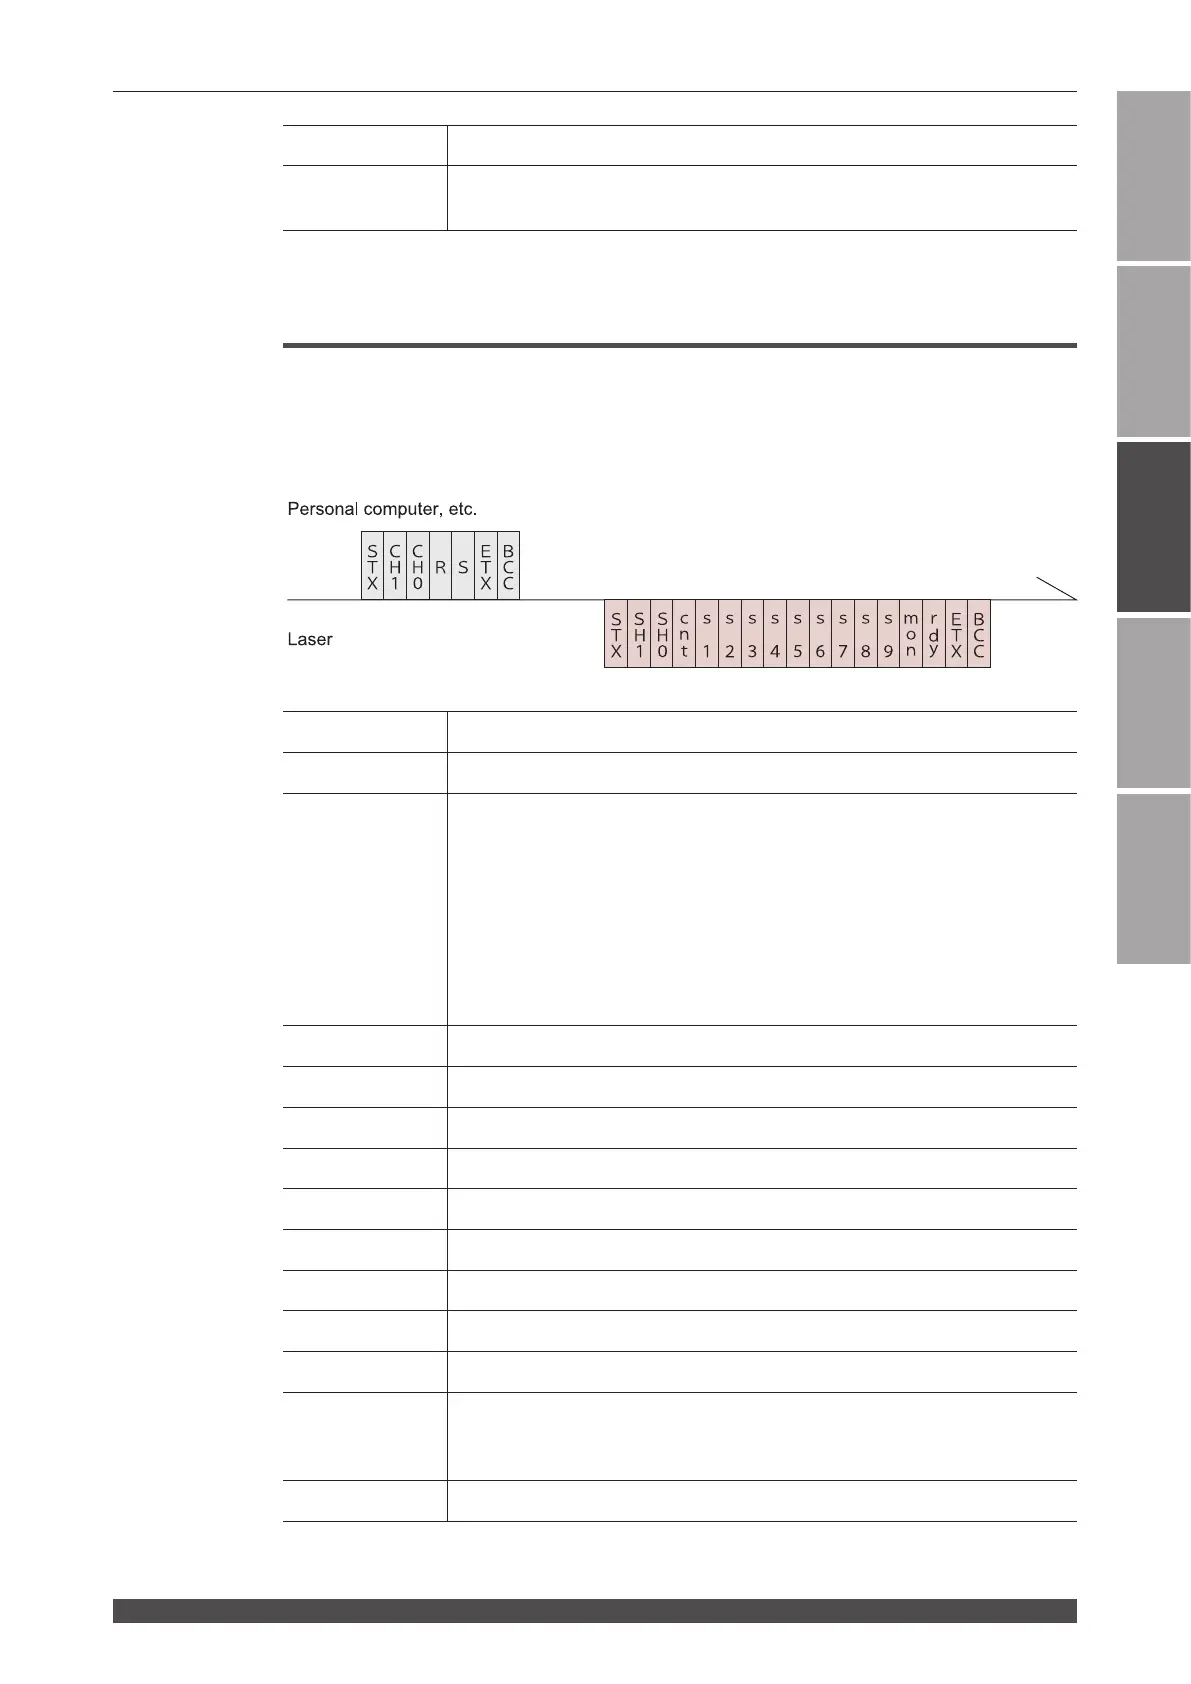
Reading the Control Method, SCHEDULE No., Branch Shutter, etc.
The command (code: RS) to read the control method, SCHEDULE No., branch
shutter, high voltage ON/OFF status, guide light ON/OFF status, automatic laser
power value transmission ON/OFF status, etc. is explained below.
CH1/CH0 Equipment No. (CH1 = tens digit, CH0 = units digit)
SH1/SH0 Schedule No. (SH1 = tens digit, SH0 = units digit)
cnt
Control method
0: Control by control panel
1: Control by external input/output signals (Output schedules are set on
the control panel.)
2: Control by external communication control
3: Maintenance mode
4: (Missing number)
5: Control by external input/output signals (Output schedules are set on
the personal computer.)
s1 HV (0: OFF 1: ON)
s2 LD (0: OFF 1: ON)
s3 Unused (xed to 0)
s4 Branch shutter 1 (0: OFF 1: ON)
s5 Branch shutter 2 (0: OFF 1: ON)
s6 Branch shutter 3 (0: OFF 1: ON)
s7 Unused (xed to 0)
s8 Unused (xed to 0)
s9 Unused (xed to 0)
mon
Automatic laser power monitor value transmission (0: OFF 1: ON)
Each time the ashlamp comes on, "00 Laser Power Monitor-Energy, number
of waveform data, etc." on page 130 is sent.
rdy READY status (0: Laser start disabled 1: Laser start enabled)


 To Next Page