116
Welding processes
Process Function
Rapid Pulse Weld
(modified
Vari Weld)
This is a modified "Vari Weld" welding process.
The special control generates a very focused stable
arc with a very high arc pressure, strengthened
by the pulsed arc phases. In the Rapid Pulse Weld
process, the penetration shape and depth can be
influenced with the dynamic setting.
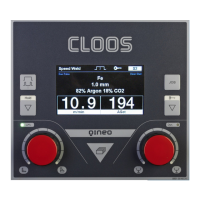
Rapid Pulse Weld processes are available for the fol-
lowing material-gas-wire combinations (date 09/18):
• Fe, 92 % Ar, 8 % CO
2
, wire 1.0 mm
• Fe, 92 % Ar, 8 % CO
2
, wire 1.2 mm
• Fe, 82 % Ar, 18 % CO
2
, wire 1.2 mm
Speed Weld
(U/I pulse)
The Speed Weld process is a U/I-controlled pulsed
arc.
The MIG/MAG welding process "Speed Weld" is es-
pecially suitable for high welding speeds and is ideal
for joining sheet metal parts from 0.1 … 5 mm.
The welding current depends on the distance be-
tween torch and workpiece. Arc seam tracking is pos-
sible in connection with the QIROX robot controller.
This process is suitable for sheet thicknesses of more
than 2…3 mm.
Cold Weld
The processes named Cold Weld are welding process-
es in connection with AC technology.
Due to the directionally stable and powerful pulsed
arc, the Cold Weld process is particularly suitable for
high welding speeds. The welding current depends
on the distance between torch and workpiece. In
connection with the QIROX robot controller, arc seam
tracking is possible to a limited extent.
This enables MIG/MAG pulse welding of thin sheets
in the range of approx. 0.5 mm…3.0 mm.
Variant Variant of characteristic curve.
Version Version number of characteristic curve.


 To Next Page