43
4.9 Rapid Pulse Weld
This is a modified "Vari Weld" welding process.
The special control generates a very focused stable arc with a very high arc
pressure, strengthened by the pulsed arc phases. In the Rapid Pulse Weld
process, the penetration shape and depth can be influenced with the dy-
namic setting.
4.10 MoTion Weld
The following welding characteristics are provided by this process:
• Best gap bridging ability
• Lowest spatter formation
• Lowest heat input
With the wire speed as a basis, all parameters are automatically adapted to
the selected power according to the synergy principle. The process can be
individually adapted with the setting parameters Fine adjustment Dynam-
ics and Fine adjustment Arc length. CleanStart is always active.
5. MAIN - Function
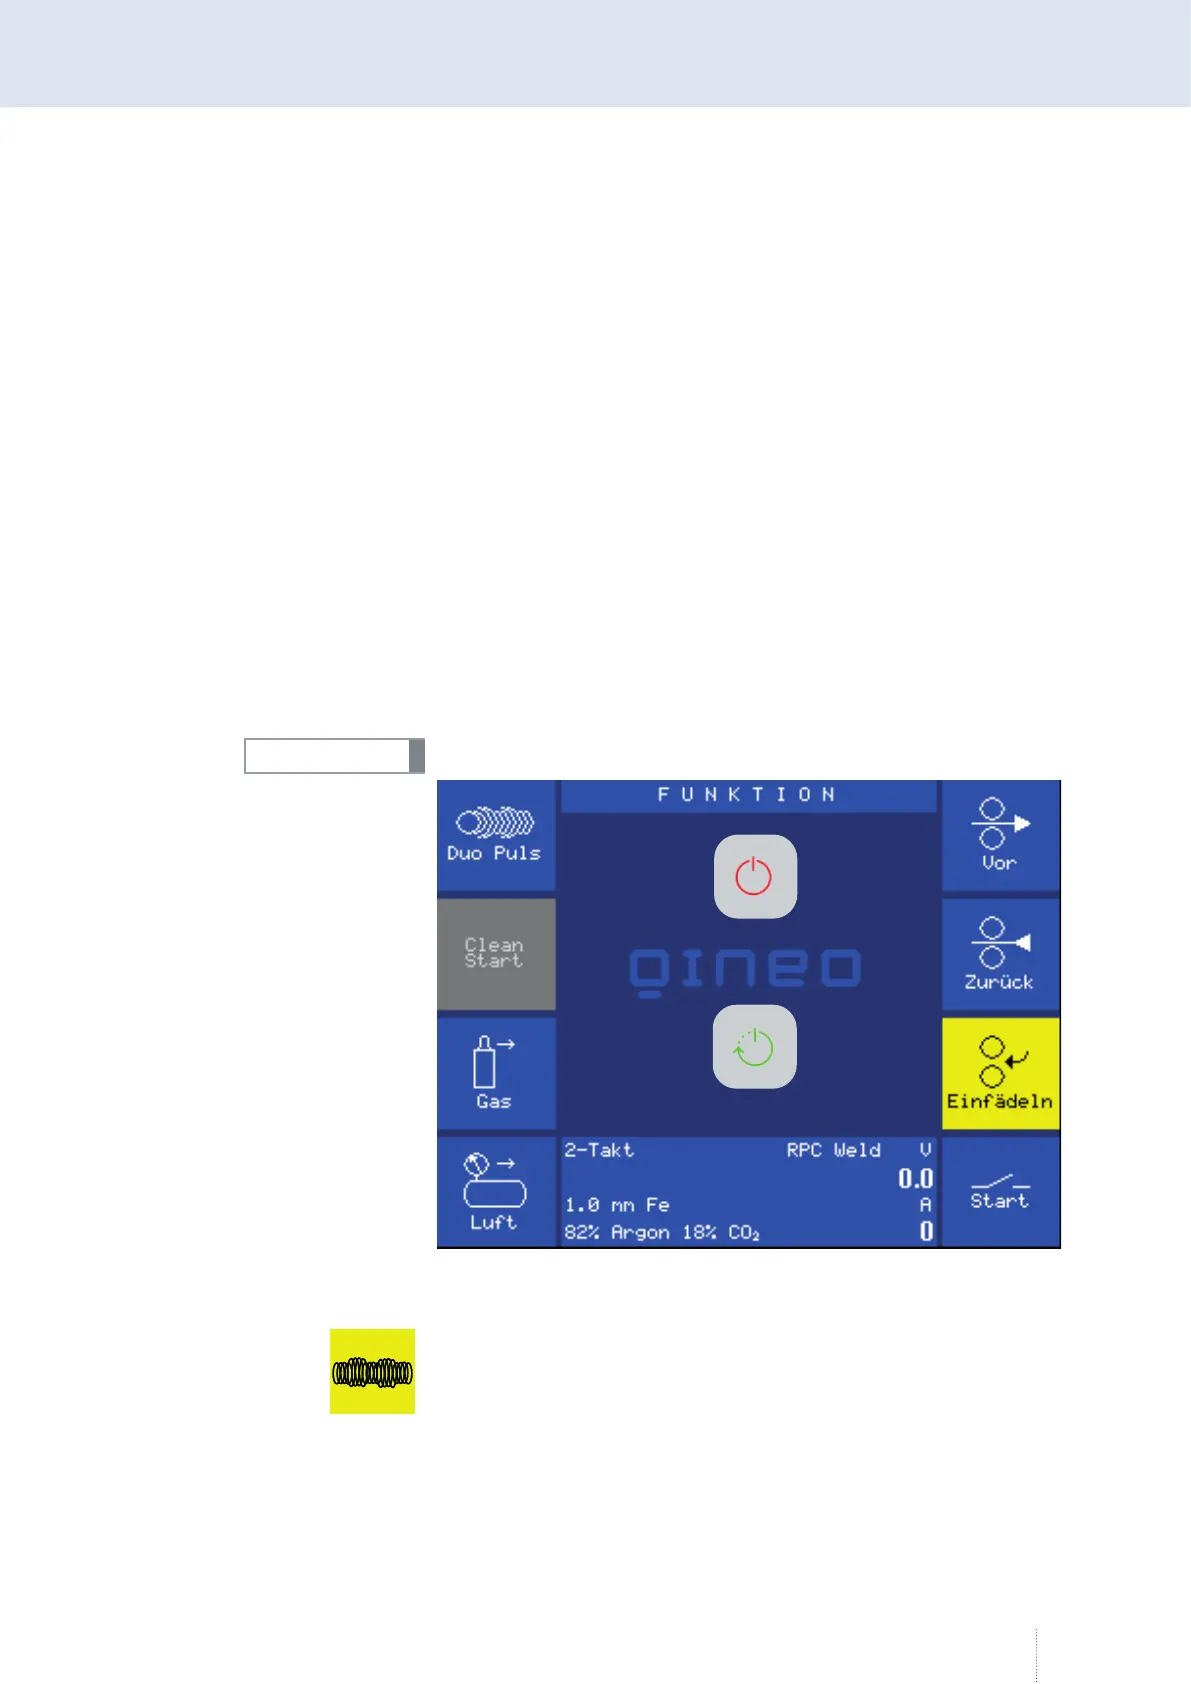
The display field is highlighted yellow if one function is active.
5.1 DuoPulse
If the function is active, a second welding parameter is generated from the
set basic value, which is higher or lower than the basic value.
By means of a defined frequency there is a switch-over between the two
parameter sets. The appearance of the weld seam surface can be formed by
the defined change of parameters. During root welding, defined cool-down
times can be reached depending on the setting. The "DuoPulse" function is
available for all gas/material combinations. If the "Expert Mode" function is
active, further parameters are available there, see "6.7 MAIN - Programming
- Expert Mode" on page 52.
INFO!
Figure 10. "Functions" menu
Re-start
Off
F U N K T I O N E N
Puls 4 -Takt
V
0
A
1.2 mm Fe
82% Argon 18% Co
2
0.0
Clean
Start
Air
F U N K T I O N E N
Puls 4 -Takt
V
0
A
1.2 mm Fe
82% Argon 18% Co
2
0.0
Clean
Start
AirAir


 To Next Page