115
2.5 Electrode Welding
All common stick electrodes can be welded with the Electrode process.
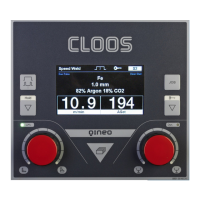
If you selected the Electrode process, the right display shows "Aset". The
displays for wire diameter and material thickness are masked out. You can
now select the required welding current by means of the left rotary knob.
By pressing the left rotary knob the open circuit voltage is switched on. The
status display is lit blue. By pressing the left rotary knob again, the open
circuit voltage is switched off.
2.6 Description of processes in MIG/MAG process
The following MIG/MAG welding processes can be selected at the welding
power source:
Process Function
Synergy Off
This MAG normal welding process is synergy-inde-
pendent. The parameters for wire speed and welding
voltage must be set individually using the rotary
knob.
Control Weld
(MAG normal)
This is a pulse-free MIG/MAG welding process with
synergy function. It offers a stable metal transfer
from short arc to spray arc.
Rapid Weld
(modified
Control Weld)
This is a modified "Control Weld" welding process. A
very concentrated arc, ensuring a very deep penetra-
tion, is generated.
In the Rapid Weld process, the penetration shape and
depth can be influenced with the dynamic setting.
Rapid Weld processes are available for the following
material-gas-wire combinations (date 09/18):
• Fe, 92 % Ar, 8 % CO
2
, wire 1.0 mm
• Fe, 82 % Ar, 18 % CO
2
, wire 1.0 mm
• Fe, 82 % Ar, 18 % CO
2
, wire 1.2 mm
Vari Weld
(I/I pulse)
The Vari Weld process is an I/I-controlled pulsed arc.
The welding settings are selected for the MIG/MAG
welding process "Vari Weld" so an extremely low
spatter pulsed arc is created without further fine
adjustment (arc length and dynamics).
The welding current does not depend on the dis-
tance between torch and workpiece. In connection
with the QIROX robot controller, arc seam tracking
is possible depending on the material. This pulse
process is suitable for sheet thicknesses of more
than 1 mm.


 To Next Page