16-37
dummyheaddummyhead
GEAR CASE
PINION GEAR SHIM
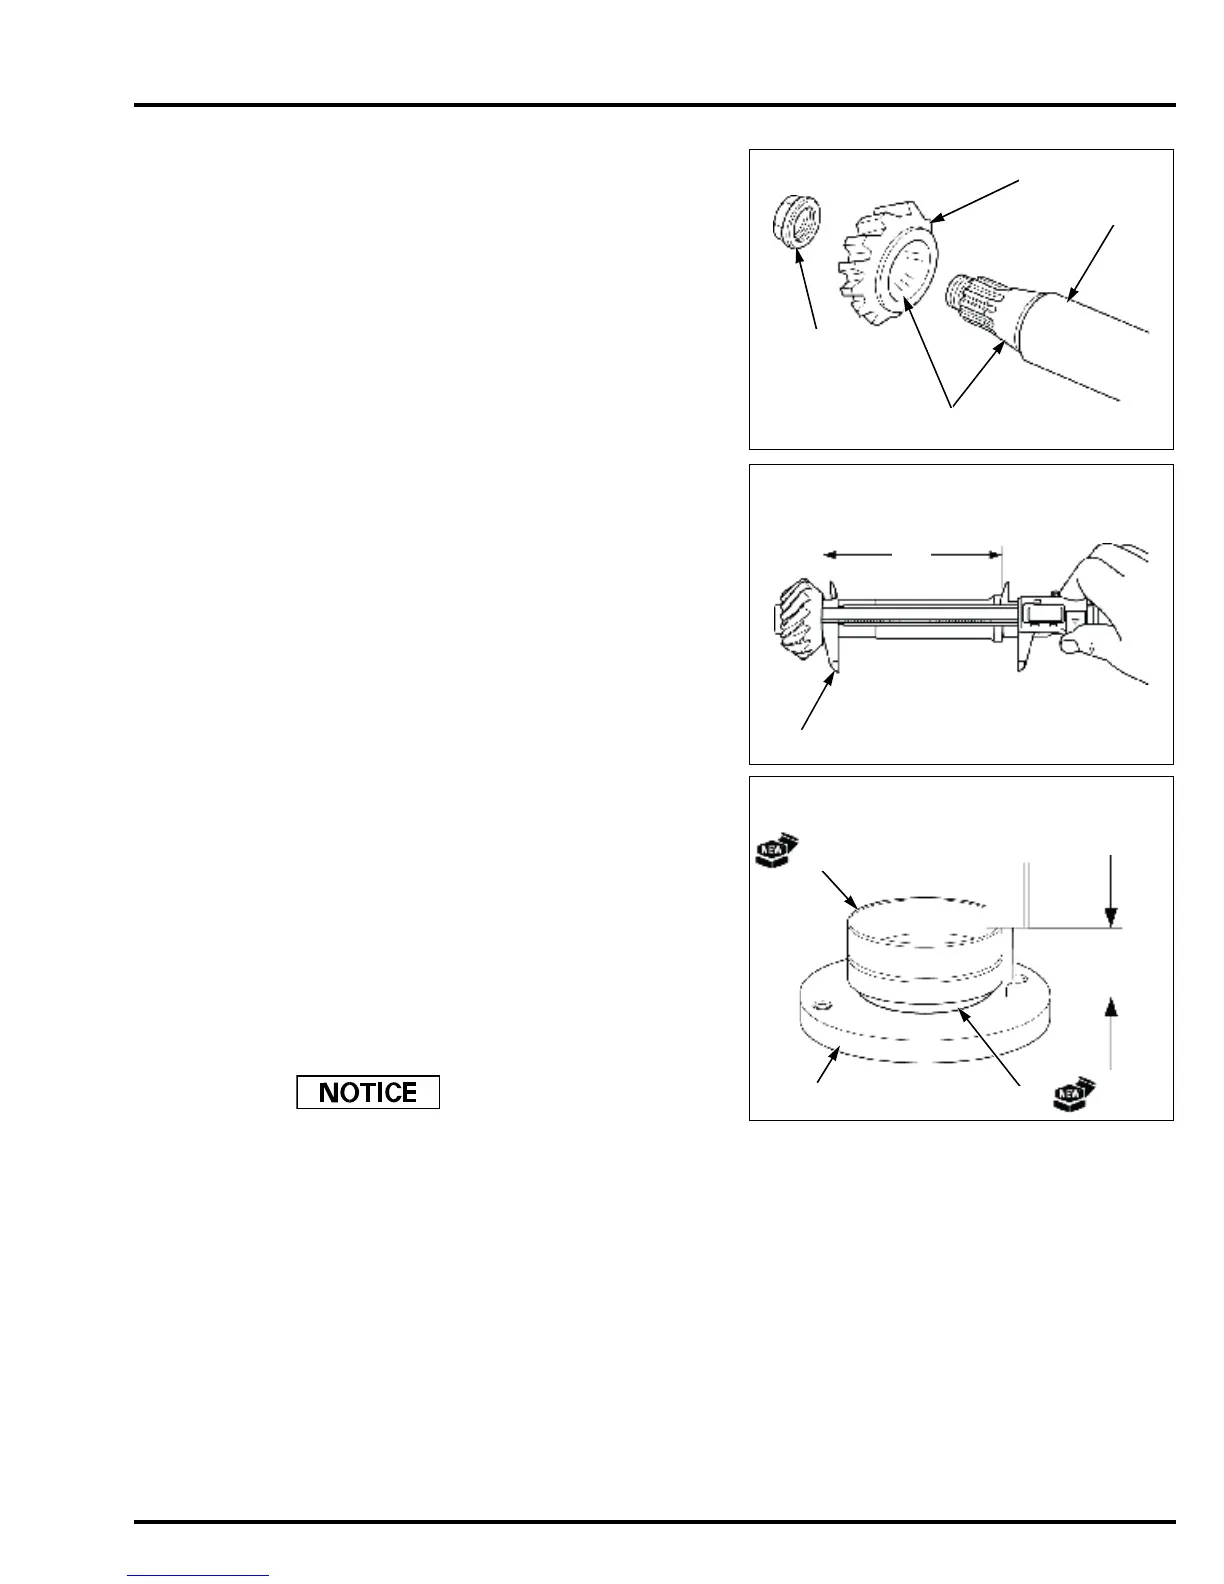
Remove the taper roller bearing (30 x 62 x 40 mm) if it
is mounted on the vertical shaft [1] (page 16-33).
Clean the tapered surface [2] of the vertical shaft and
the tapered surface of the pinion gear [3] thoroughly
using a shop towel and degreasing cleaning agent.
Install the pinion gear on the vertical shaft.
Tighten the pinion gear nut [4] to the specified torque
using the special tool (vertical shaft holder) (page 16-
29).
Use a vernier caliper [1] to measure distance (C) [2]
from the end of the pinion gear to the end of the collar of
the vertical shaft as shown. Record this measurement.
If you have a gauge adapter special tool, place the disc
that is included with that tool on a flat surface.
Make sure the side marked with the tool number is on
the bottom so the smooth side is up.
If you do not have a gauge adapter special tool, use any
flat, hard surface for this procedure.
Place one new pinion gear inner race [2] on the smooth
side of the gauge adapter special tool (or flat, hard
surface).
Press a new outer race [3] down over the inner race
and turn it several times to seat the rollers.
There are differences in the way bearings fit together.
Keep the inner race you are measuring in the same
relationship to the outer race you are measuring. Install
the assembled bearing with the race you measure next
to the pinion gear.
Measure the height of the assembled outer race/inner
race (Distance D’) [4] and record it.
TOOL:
Vertical shaft holder 07SPB-ZW10200
TORQUE: 103 N·m (10.5 kgf·m, 76 lbf·ft)
TOOL:
Gauge adapter, 100 mm [1] 070PJ-ZY30100


 To Next Page