U511 User’s Manual Programming Commands
Version 1.1 Aerotech, Inc. 5-31
5.5.18. Cutter Compensation Commands
Cutter compensation offsets programmed moves to compensate for the size of the cutting
tool. The UNIDEX 511 implements cutter compensation with the following G code
commands:
G40 - cutter comp. off
G41 - cutter comp. on, LEFT
G42 - cutter comp. on, RIGHT
G43 - define cutter radius
G44 - define compensated axes.
Cutter compensation operates only on contoured motions, G1, G2, and G3. It modifies the
endpoint of a move based on the next move. Therefore, a move will not begin executing
until the next move has been commanded. Commands that occur between contours are
stored until the next contoured motion is sent. No more than 5 commands should be
placed between contours.
Contoured moves are modified either by making the move shorter or by adding a circle
with the same radius as the cutter, between the moves.
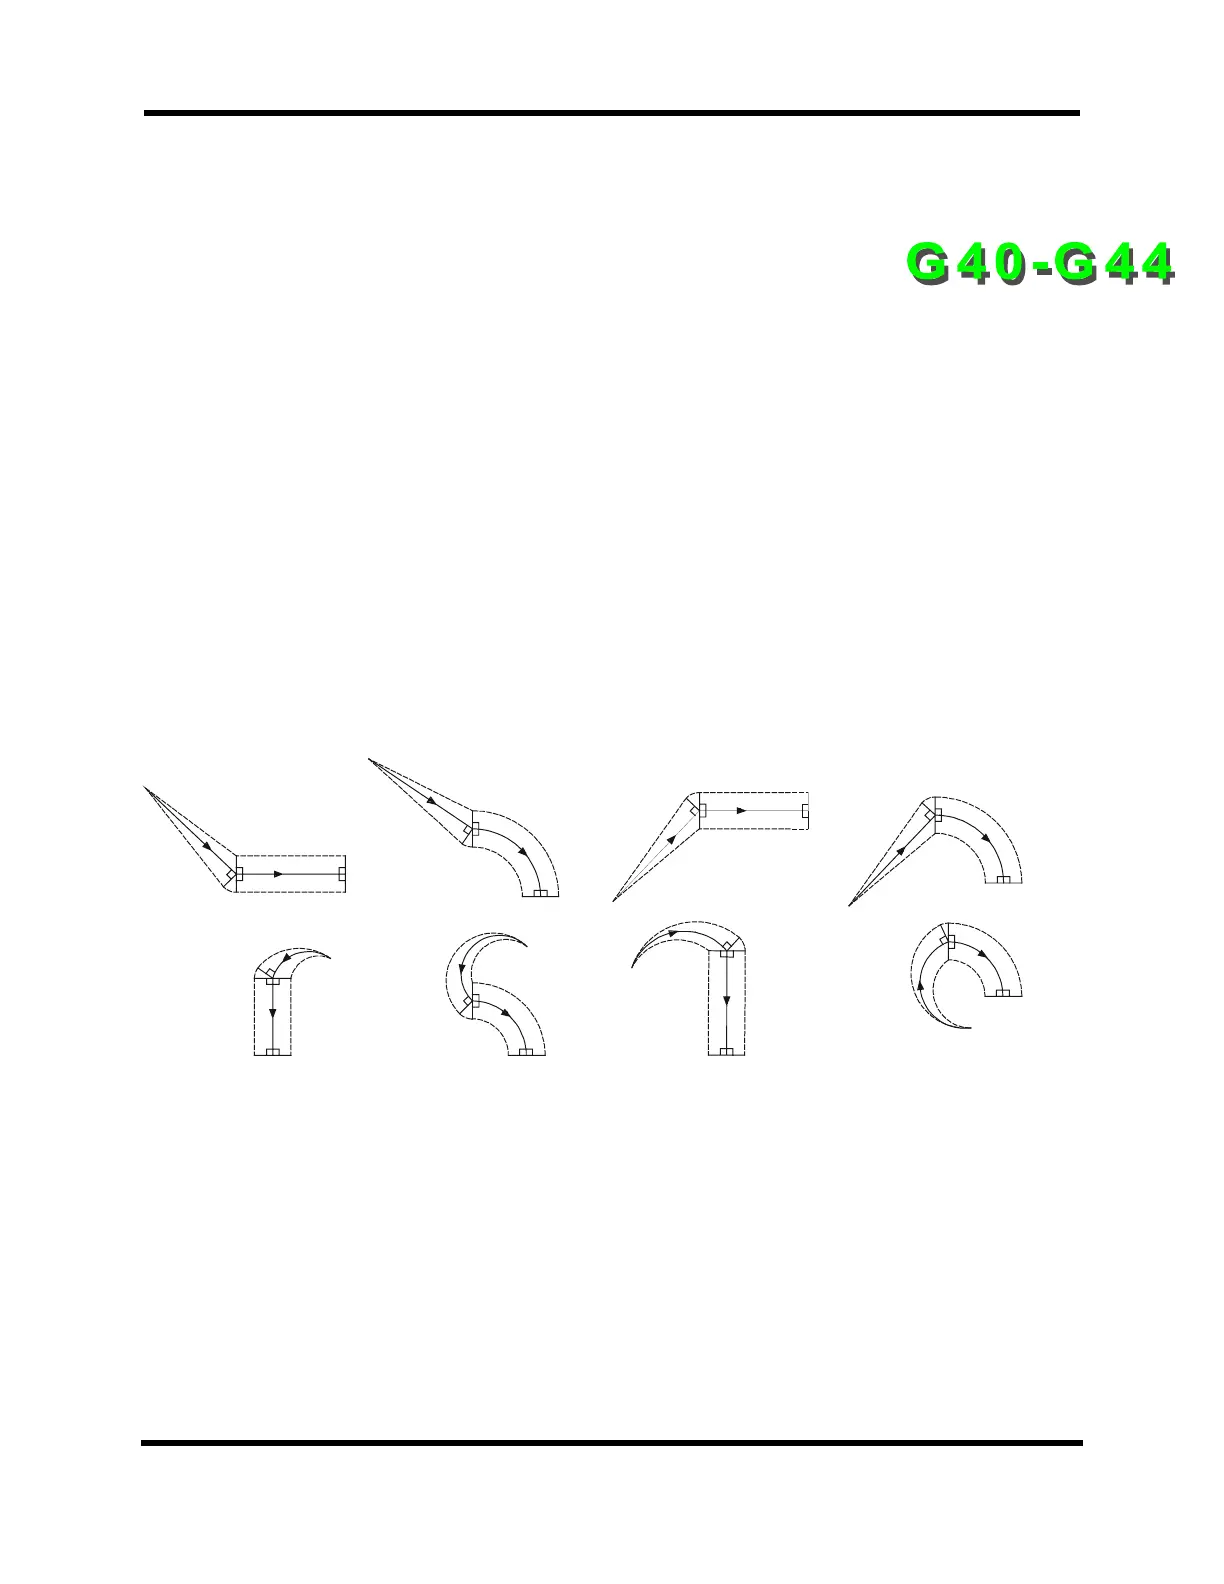
The first move is assumed to be a move on to the part. This move is the first move after a
G41 or G42 command and can be linear or circular. The end point of this move is
adjusted so that it is normal to the second move’s starting point, offset by the tool radius.
Refer to Figure 5-1.
Figure 5-1. Startup Moves
The last move is assumed to be a move off of the part. This contour occurs after the G40
command. The end point of the move preceding the G40 command (last move on work
piece) is adjusted to be normal to the move’s programmed endpoint. Refer to Figure 5-2.
r
r
r
r
r
G42
G41
r
rr
rr
G42
G41
r
r
r
rr
G42
G41
r
r
r
G42
G41
rr
r
r
r
G42
G41
r
r
rr
r
G42
G41
r
r
r
r
r
G42
G41
rr
r
r
r
G42
G41
r
r
Artisan Technology Group - Quality Instrumentation ... Guaranteed | (888) 88-SOURCE | www.artisantg.com


 To Next Page