Program steps and cycles | Thread cycles
8
8.7 Thread cycles
Threading steps are used for machining a thread along a straight or
tapered surface using a threading tool.
Thread (straight)
Cutting an inside or outside straight thread is possible with the
Thread step.
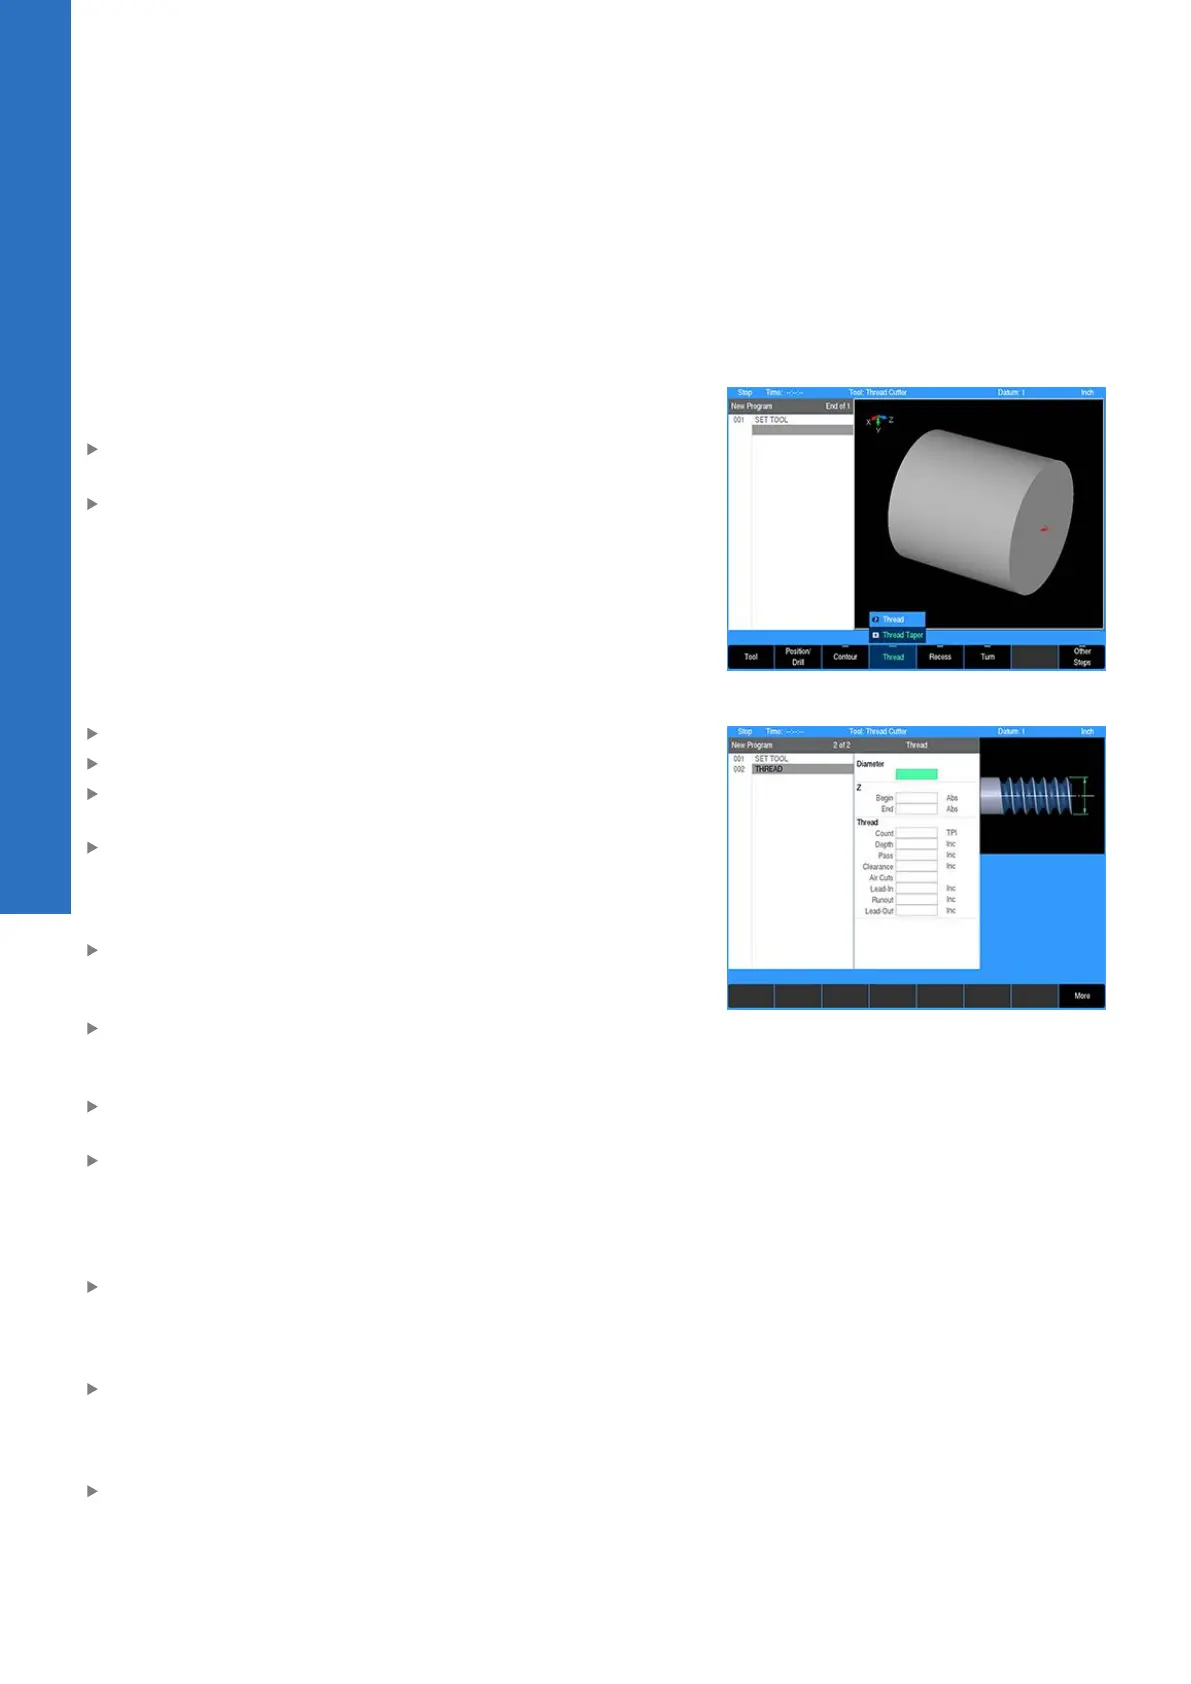
From the PGM screen, press the THREAD key to access the
Thread popup menu
Select Thread from the popup menu
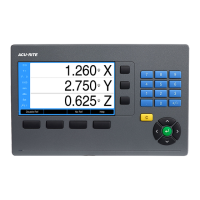
Entering data:
Enter the outside or inside Diameter of the thread
Enter the Z axis Begin and End locations of the thread
For English threads, enter the number of threads per inch (TPI).
For metric threads, enter the pitch of the thread (mm).
Enter the Depth of the thread as measured from the
programmed diameter. If a value is not entered, Depth will
default to the standard value based on the thread pitch. If
calculated, the value is shown in blue text.
Enter the maximum depth per machining Pass. When multiple
passes are needed, the depth of each subsequent pass is
reduced to maintain a constant load on the tool.
Enter the Clearance distance. This is the distance the tool is
moved away from the material before moving to the start of the
next pass.
Enter the number of follow-up passes, or Air Cuts, made after
completing the final machining pass. The valid range is 0 to 10.
Enter the Lead-In distance. This is the distance before the start
of the thread at which the tool begins Z axis cutting motion.
This distance allows the Z axis to accelerate to speed and
synchronize with the spindle location before the start of the
thread.
Enter the Runout distance. This is the distance before the end
of the thread at which the tool begins pulling out of the material.
Enter 0 to machine to the programmed end of the thread before
retracting straight out of the material.
Enter the Lead-Out distance. This is the distance the tool
continues moving past the programmed end of thread. This
distance allows the tool to decelerate without affecting the main
section of the thread.
Enter the Start Angle of the thread. If cutting multiple threads,
each thread should start at the appropriate angle relative to each
other.
134
ACU-RITE | TURNPWR | User's Manual | 08/2020


 To Next Page