10.8 Valve Pin Finishing of Head
10.8.1 5500 Series
WARNING
Extreme heat. Avoid contact with heated surfaces.
Use appropriate protective clothing. Failure to do so can cause serious
injury.
1. Heat the Hot Runner system to the processing temperature.
2. Allow the pin to soak in the Hot Runner system for 10 minutes to achieve
the maximum heat expansion of the pin at processing temperature.
NOTE
Mold cooling should be running.
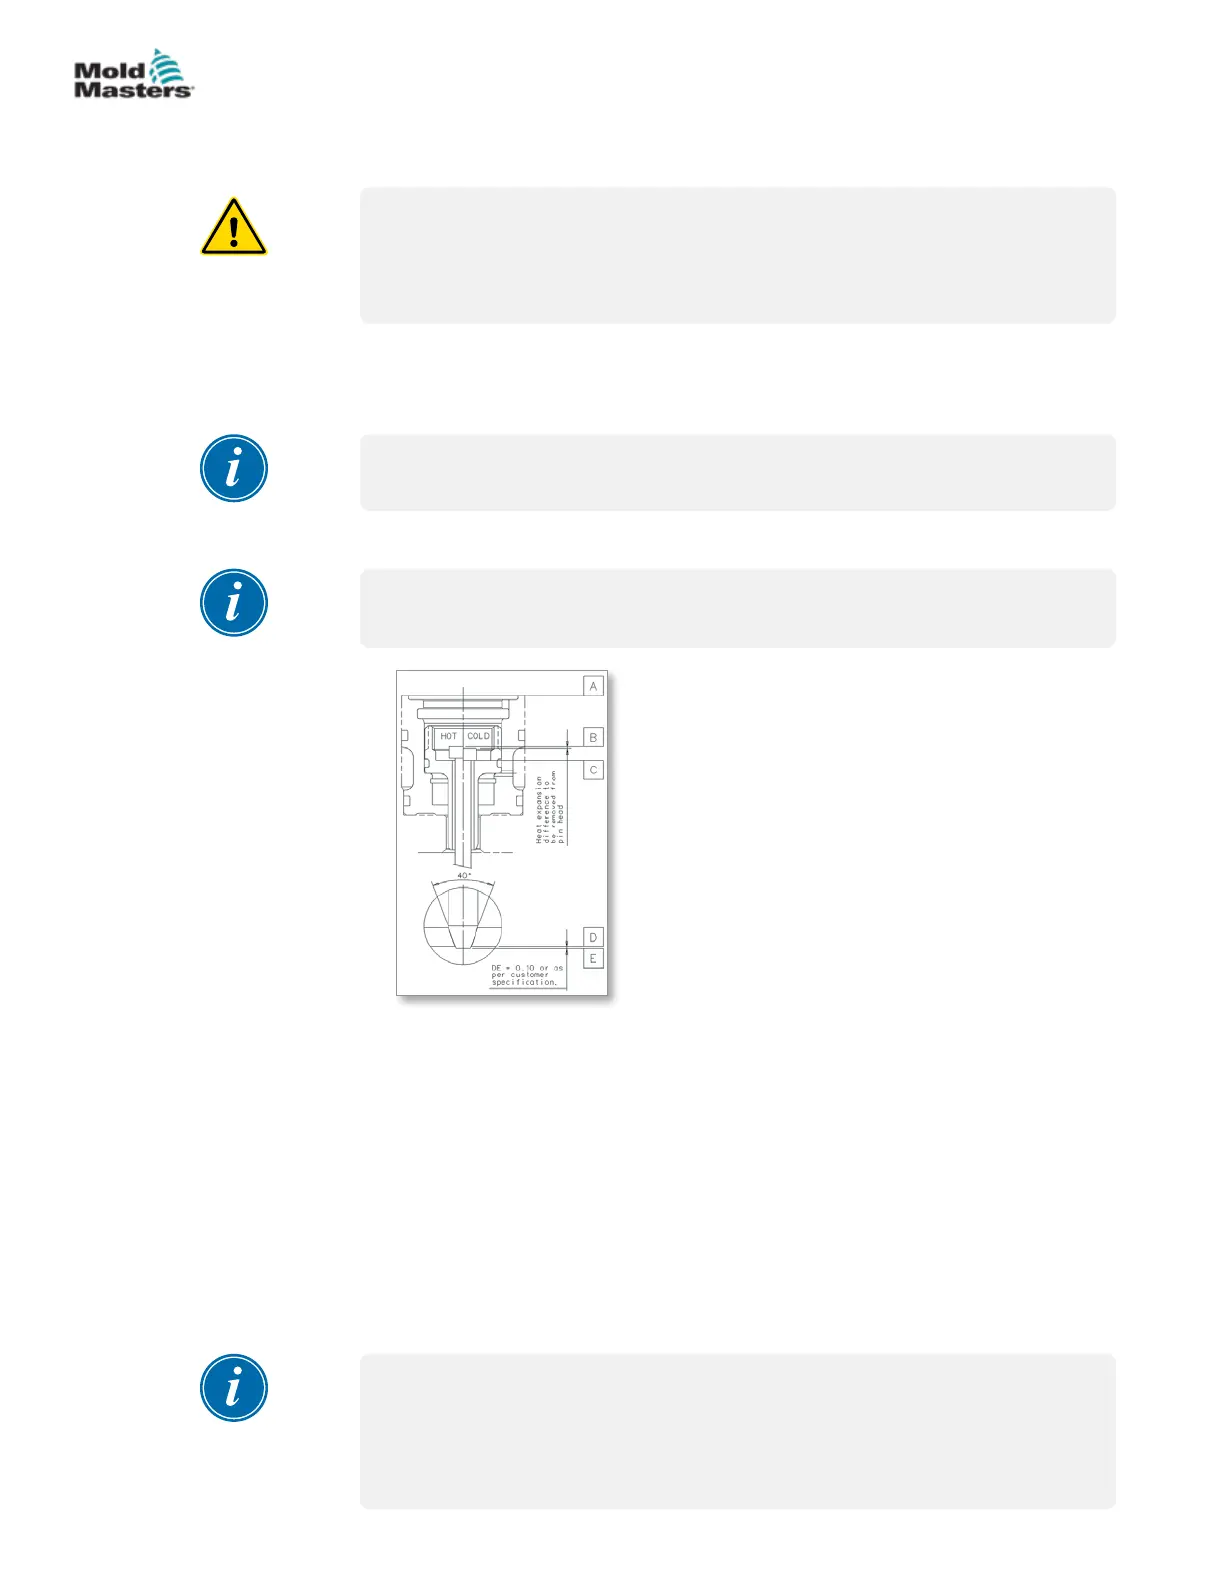
3. Measure the distance AB in heated condition.
NOTE
Heat expansion dierence to be removed from pin head.
Figure 10-15 5500 Series - Measure distance
4. Check that the tip of the pin is tted correctly into the land.
5. The heat expansion dierence between the mold and Hot Runner is
removed by grinding the back of the pinhead.
6. HED = AC - (AB + 3.05 (0.12)* + 0.02 (0.0008)** preload) mm (in.)
HED = heat expansion dierence
* 3.05 = head of pin
** 0.02 = pressure preload
7. Continue to re-assemble the actuator assembly. The maximum pin
preload in the land under full heat expansion must not exceed 0.02 mm
(0.0008 in.).
NOTE
The standard stroke of the HY550* A/E is 4.0 mm (0.16 in.). This can be
increased to maximum of 8.0mm by removing material from the piston top.
The stroke of the HY550* C/F is 8.0 mm (0.31 in.) and cannot be altered.
10-11HYDRAULIC / PNEUMATIC ACTUATORS
Hot Runner User Manual
© 2020 Mold-Masters (2007) Limited. All Rights Reserved.


 To Next Page