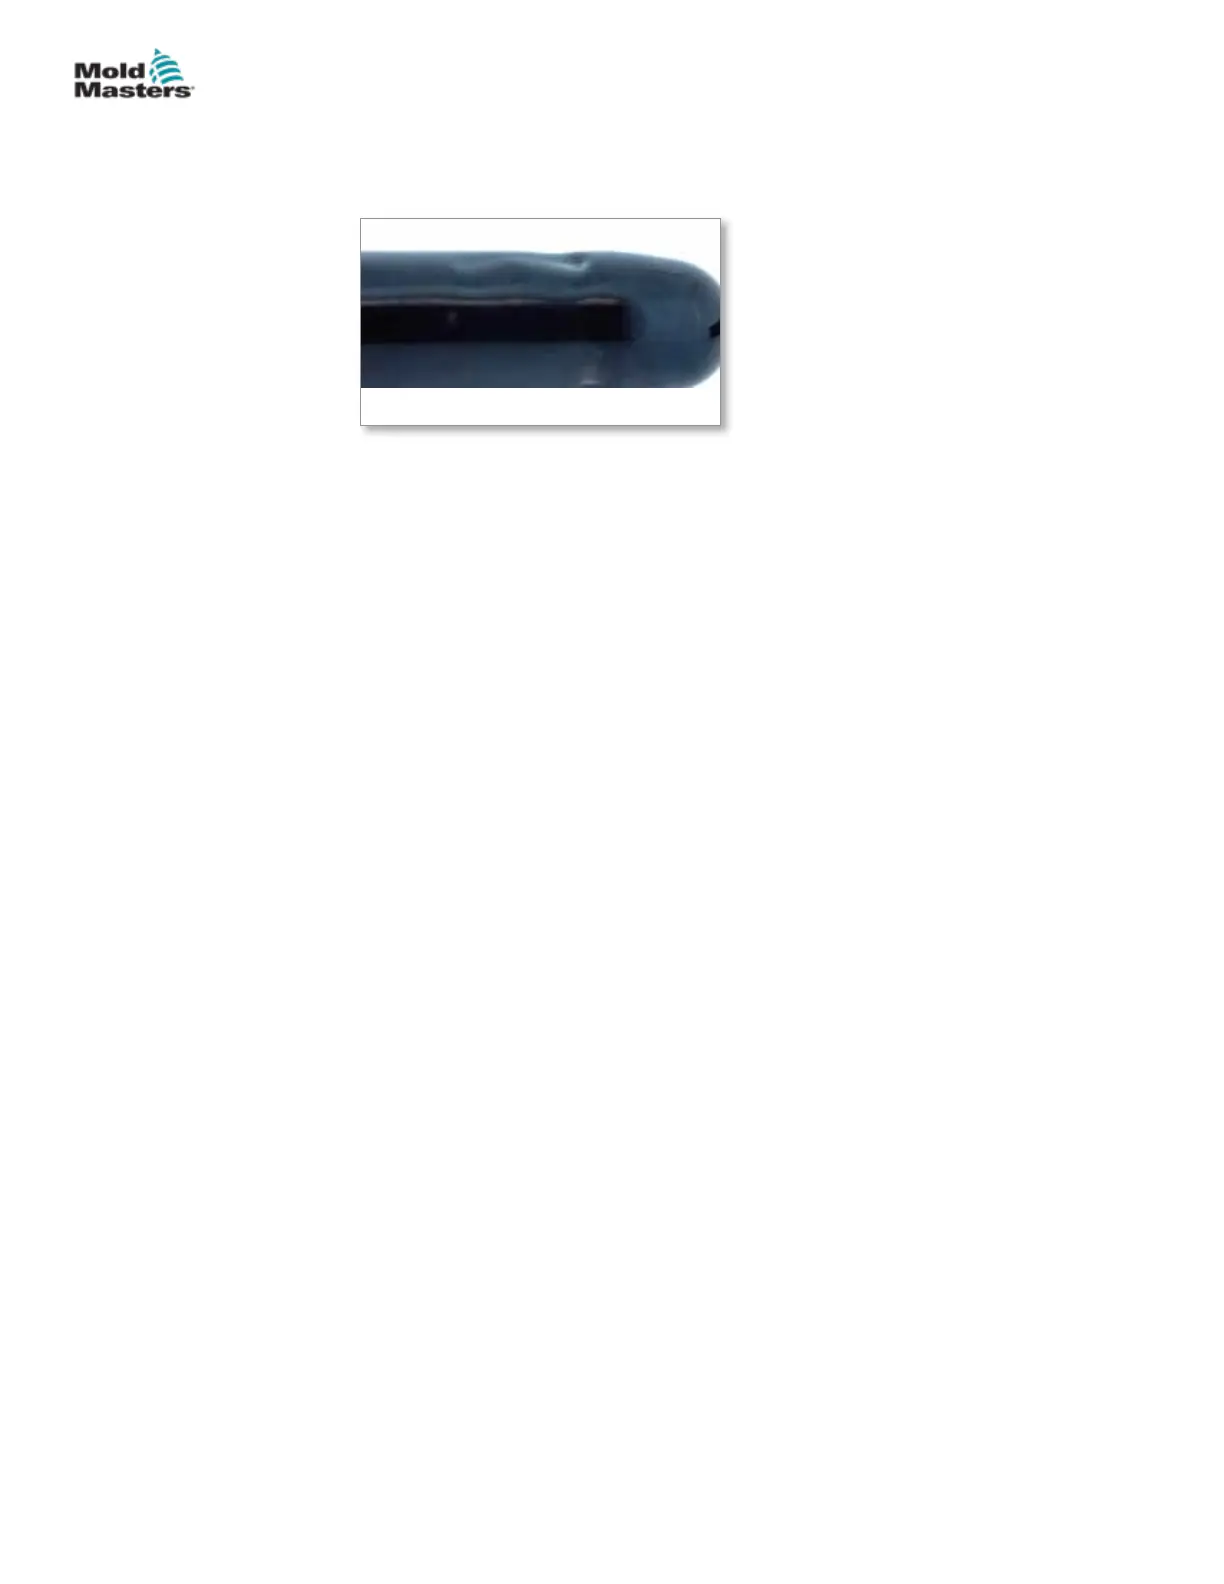
20.6.15 Sinks or Voids
The nished product has hollows and pockets in areas that do not cool
suciently, causing contraction.
Probable Cause:
1. Molding Machine
• Low injection pressure
• Short injection time
• Insucient material in cavity
• High injection speed
• Low back pressure
• Damaged backow valve / check ring
2. Mold
• Mold not at required temperature
• Small gate leading to early freezing
• Gate land length too long
• Incorrect rib / wall dimensions
• Material ow incorrect
• Thick wall part
3. Material
• Hot material
• Material wrong grade for application
Solution (in sequence):
1. Adjust injection speed
2. Increase injection hold time
3. Increase injection pressure
4. Adjust melt temperature
5. Adjust mold temperature
6. Inspect for hot spots
7. Enlarge and / or add vents to mold parting line
8. Increase sprue or runner size
9. Increase gate size / reduce gate land length
10. Relocate gate closer to heavy / thicker areas
11. If possible, core out heavy wall sections
20-19TROUBLESHOOTING
Hot Runner User Manual
© 2020 Mold-Masters (2007) Limited. All Rights Reserved.


 To Next Page