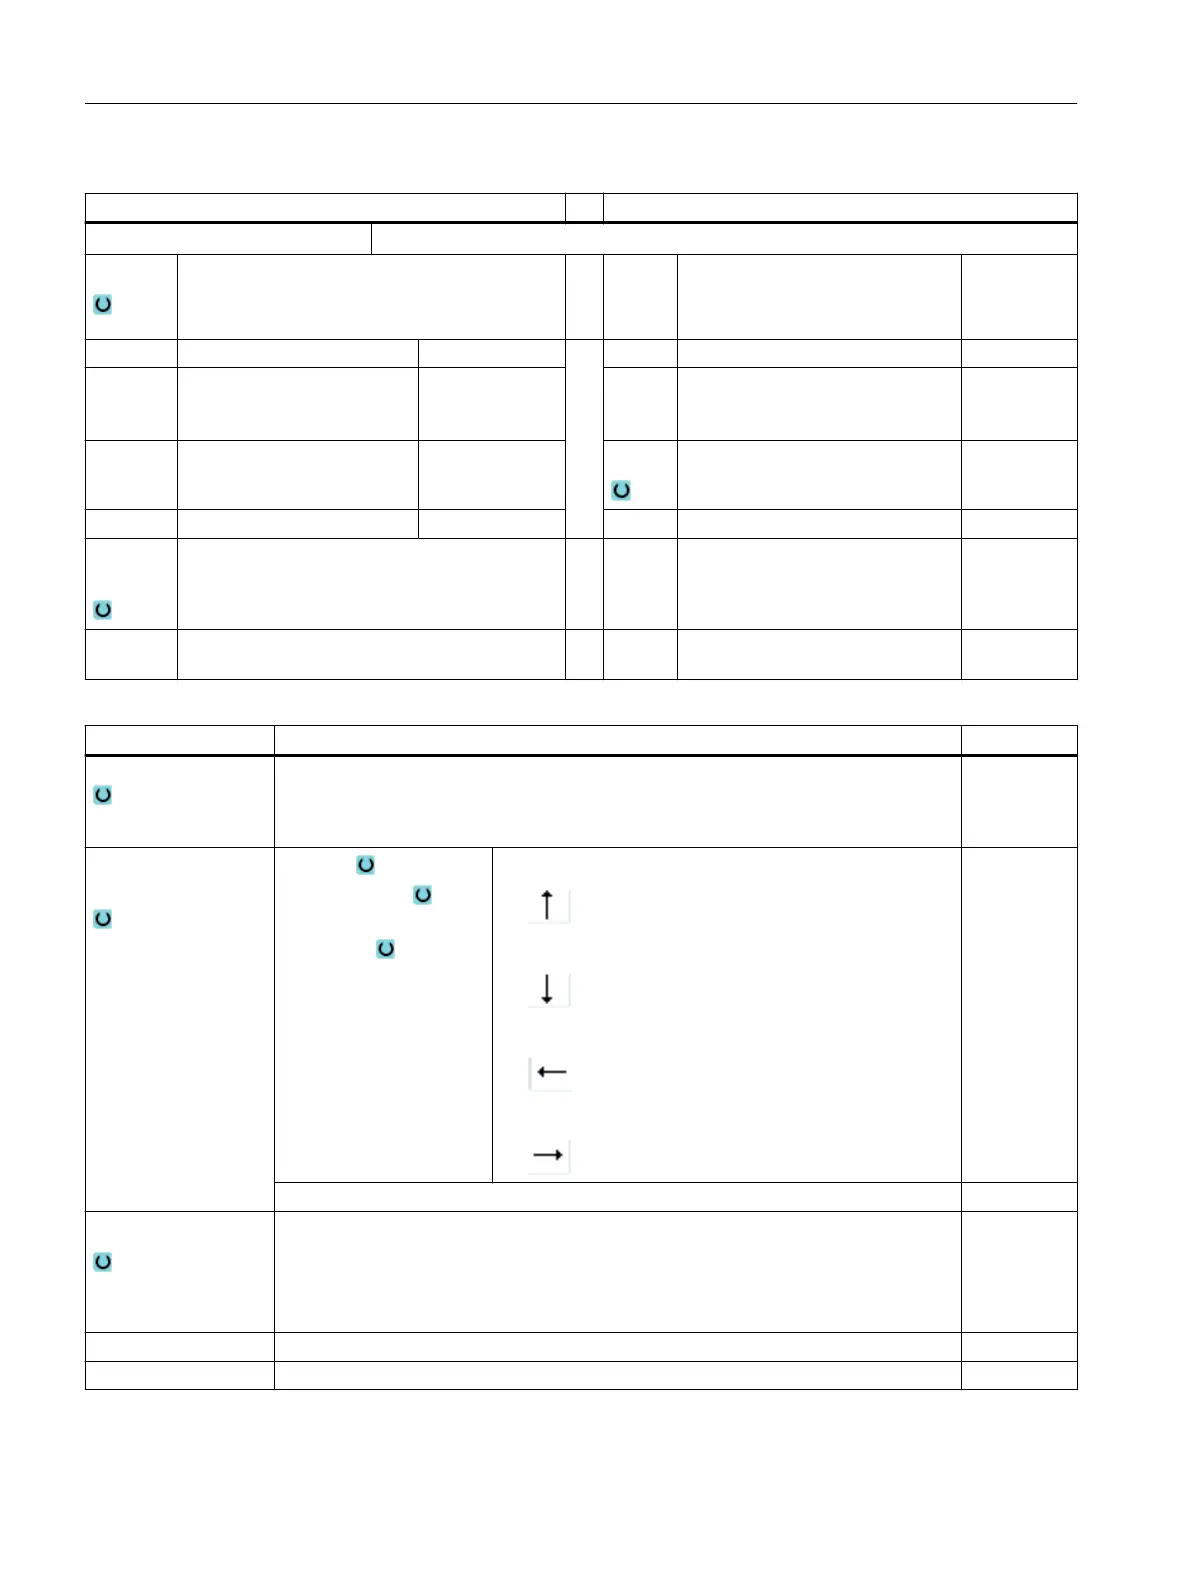
G code program parameters ShopTurn program parameters
Input
● Complete
PRG
● Name of the program to be generated
● Auto
Automatic generation of program names
T Tool name
PL Machining plane D Cutting edge number
RP Retraction plane – (only for
machining direction, longitu‐
dinal, inner)
mm F Feedrate mm/rev
SC Safety clearance mm S / V Spindle speed or constant cutting
rate
m/min
F Feedrate *
Residual
material
With subsequent residual material removal.
● Yes
● No
CONR Name to save the updated blank contour for re‐
sidual material removal
Parameter Description Unit
Machining
● ∇ (roughing)
● ∇∇∇ (finishing)
● ∇+∇∇∇ (complete machining)
Machining
direction
● Face
● Longitudinal
● Parallel to the
contour
● From inside to outside
● From outside to inside
● From end face to rear side
● From rear side to end face
The machining direction depends on the stock removal direction and choice of tool.
Position
● Front
● rear
● Internal
● external
D Maximum depth infeed - (only for ∇) mm
DX Maximum depth infeed - (only for parallel to the contour, as an alternative to D). mm
Programming technology functions (cycles)
10.3 Contour turning
Turning
460 Operating Manual, 06/2019, A5E44903486B AB



 To Next Page