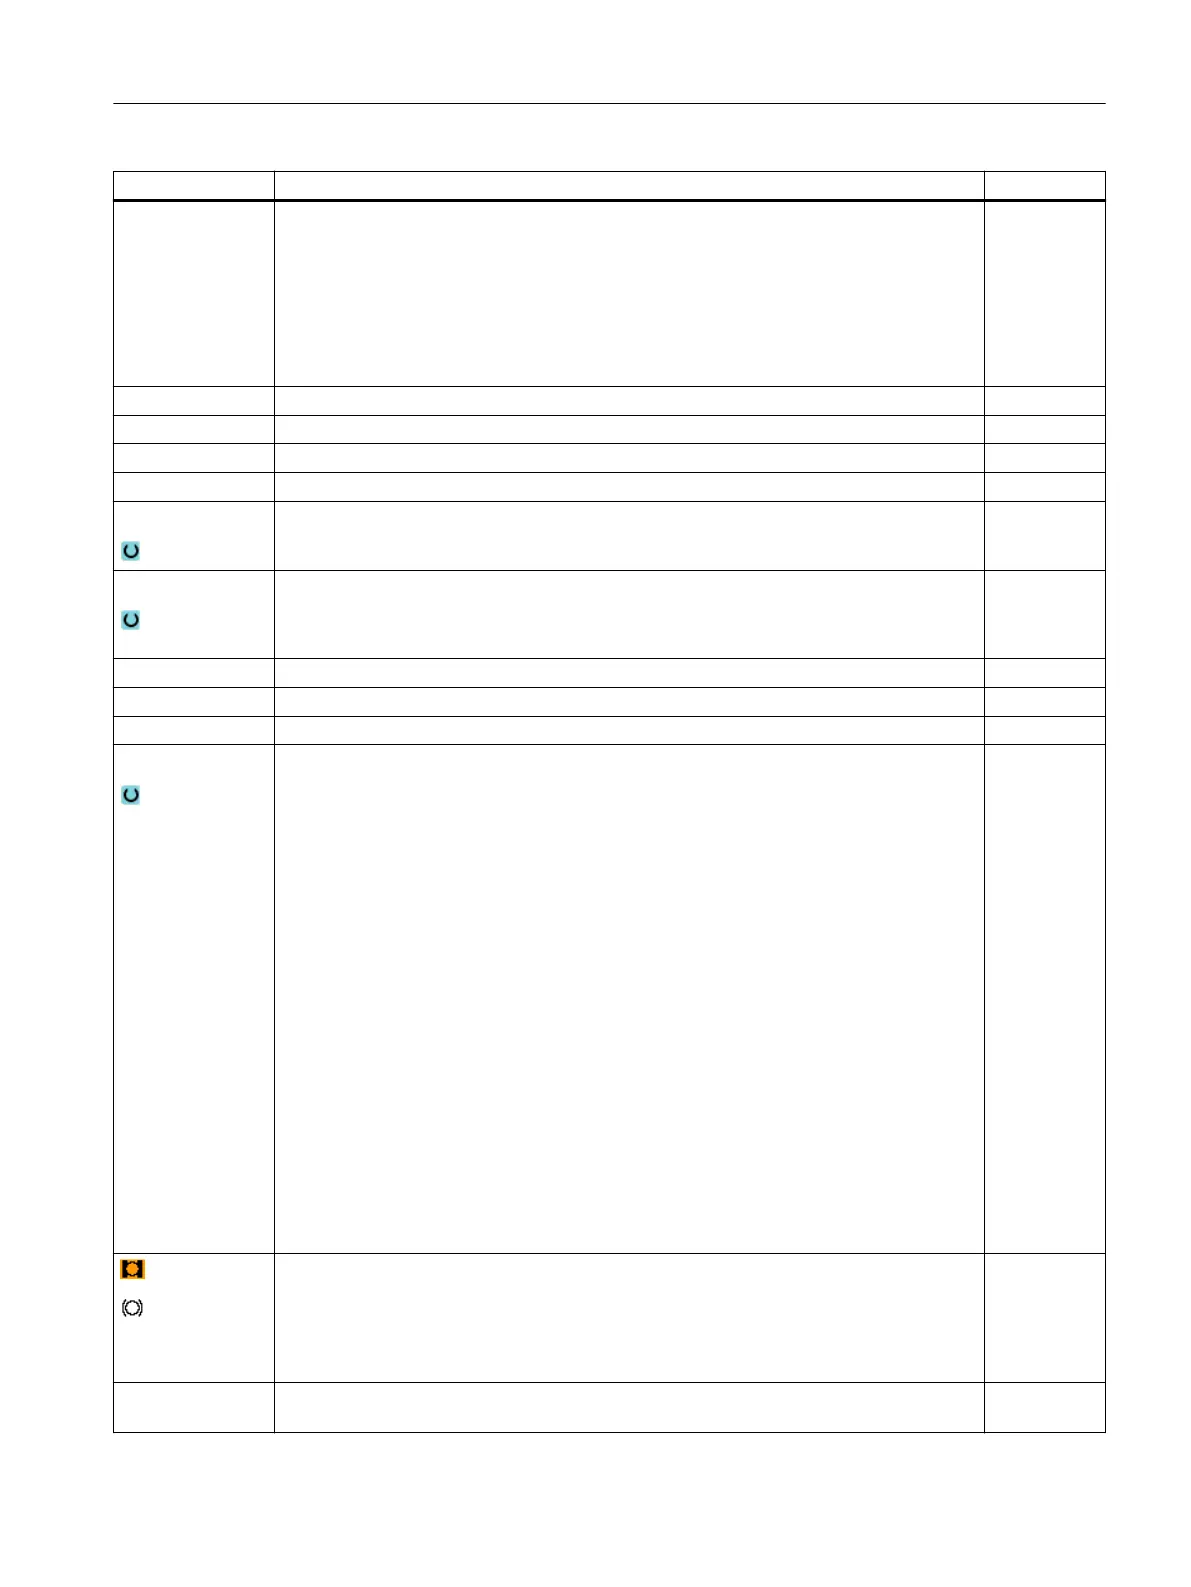
Parameter Description Unit
C0
Y0
Z0
X0
(only for Shop‐
Turn)
Peripheral surface Y: The positions refer to the reference point:
Positioning angle for machining surface – (only for single position)
Reference point Y – (only for single position)
Reference point Z – (only for single position)
Reference point X – (only for single position)
Degrees
mm
mm
mm
W Pocket width mm
L Pocket length mm
R Corner radius mm
α0 Angle of rotation Degrees
Z1 Pocket depth (abs) or depth relative to Z0 (inc) – (only for ∇, ∇∇∇ or ∇∇∇ edge) mm
DXY
● Maximum plane infeed
● Maximum plane infeed as a percentage of the milling cutter diameter
- (only for ∇ and ∇∇∇)
mm
%
DZ Maximum depth infeed – (only for ∇, ∇∇∇ or ∇∇∇ edge) mm
UXY Plane finishing allowance – (only for ∇, ∇∇∇ or ∇∇∇ edge) mm
UZ Depth finishing allowance – (only for ∇, ∇∇∇) mm
Insertion The following insertion modes can be selected – (only for ∇, ∇∇∇ or ∇∇∇ edge):
● Predrilled (only for G code)
With G0, the pocket center point is approached at the retraction plane level, and then,
from this position, also with G0, the axis travels to the reference point brought forward
by the safety clearance. The machining of the rectangular pocket is then performed
according to the selected insertion strategy, taking into account the programmed
blank dimensions.
● Vertical: Insert vertically at center of pocket
The tool executes the calculated actual depth infeed at the pocket center in a single
block. This setting can be used only if the cutter can cut across center or if the pocket
has been predrilled.
● Helical: Insert along helical path
The cutter center point traverses along the helical path determined by the radius and
depth per revolution (helical path). If the depth for one infeed has been reached, a full
circle motion is executed to eliminate the inclined insertion path.
● Oscillating: Insert with oscillation along center axis of rectangular pocket(only for G
code)
The cutter center point oscillates back and forth along a linear path until it reaches the
depth infeed. When the depth has been reached, the path is traversed again without
depth infeed in order to eliminate the inclined insertion path.
(only for Shop‐
Turn)
Clamp/release spindle (only for end face C/peripheral surface C, if inserted vertically)
The function must be set up by the machine manufacturer
FZ
(only for G code)
Depth infeed rate – (for vertical insertion only) *
Programming technology functions (cycles)
10.4 Milling
Turning
Operating Manual, 06/2019, A5E44903486B AB 493



 To Next Page