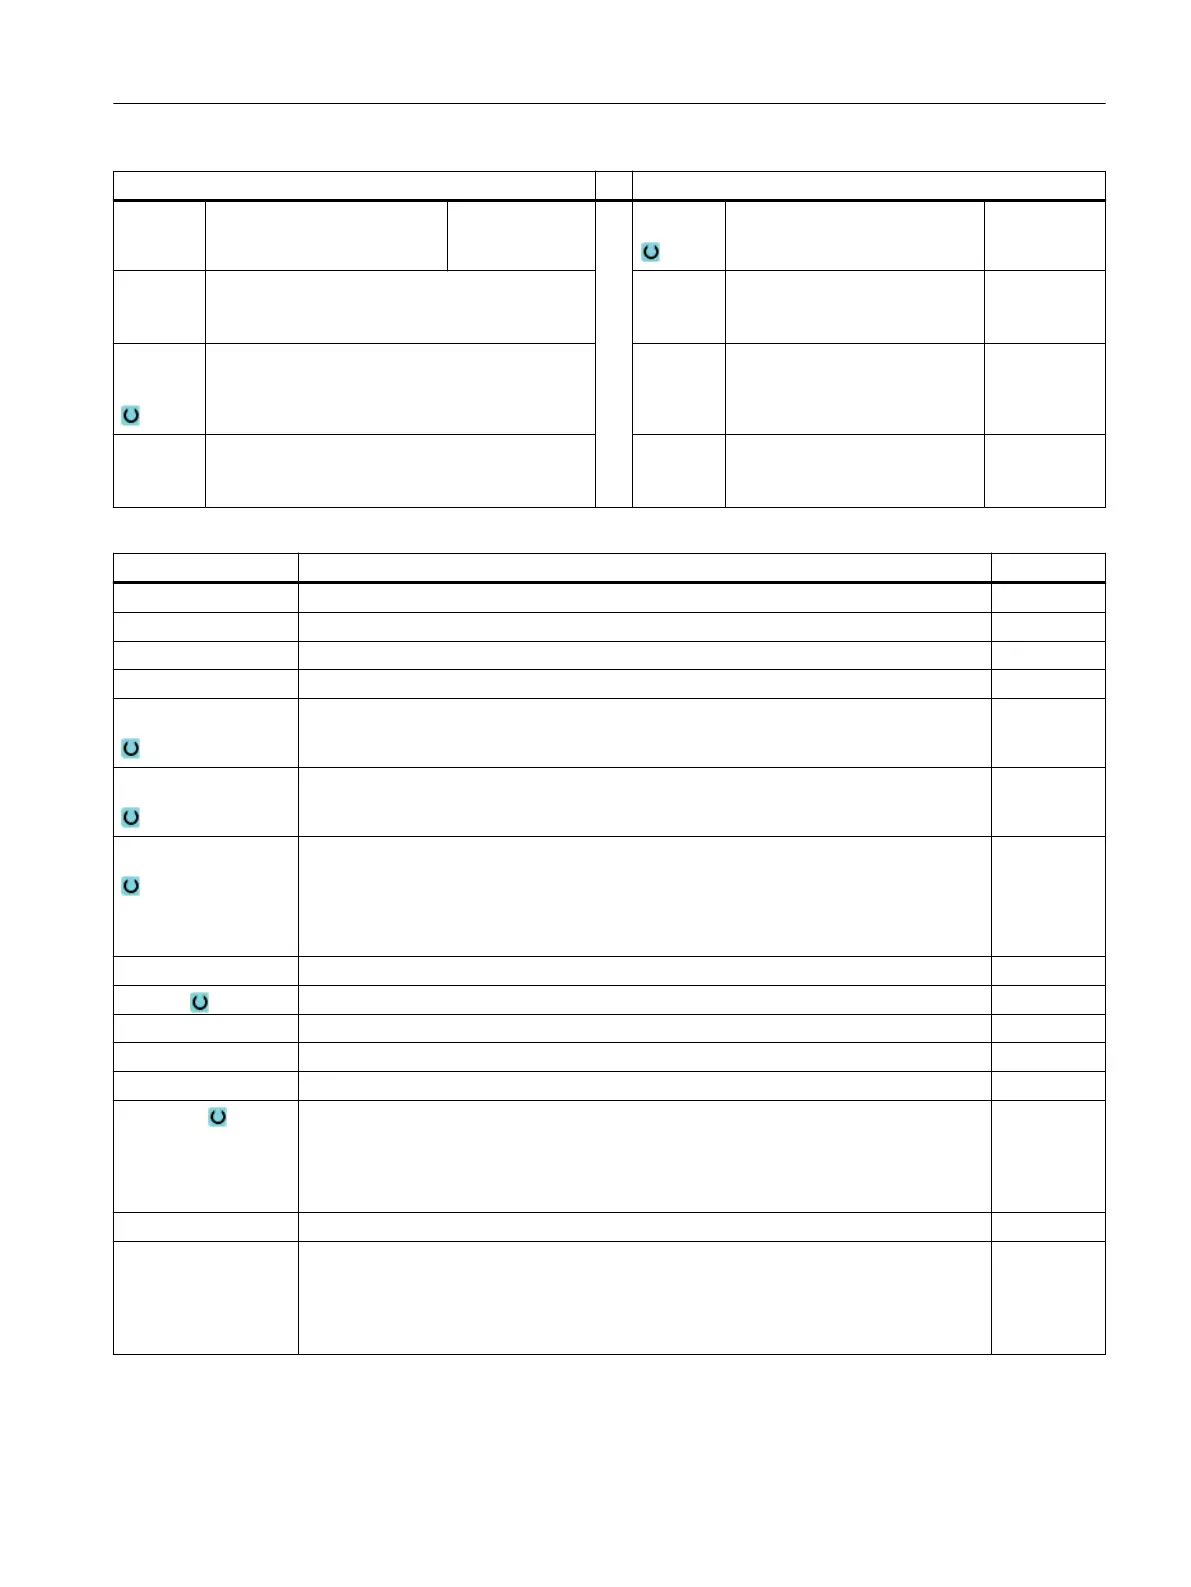
G code program parameters ShopTurn program parameters
SC Safety clearance mm S / V Spindle speed or constant cut‐
ting rate
rpm
m/min
CON Name of the updated blank contour for residual
material machining (without the attached char‐
acter "_C" and double-digit number)
Residual
material
With subsequent residual material removal
● Yes
● No
CONR Name to save the updated unmachined-part
contour for residual material removal - (only
"Yes" for residual material removal)
Parameter Description Unit
FX (only ShopTurn) Feedrate in X direction mm/rev
FZ (only ShopTurn) Feedrate in Z direction mm/rev
FX (only G Code) Feedrate in X direction *
FZ (only for G code) Feedrate in Z direction *
Machining
● ∇ (roughing)
● ∇∇∇ (finishing)
Machining direction
● Face
● Longitudinal
Position
● front
● rear
● Internal
● external
D Maximum depth infeed - (only for ∇) mm
UX or U Finishing allowance in X or finishing allowance in X and Z – (only for ∇) mm
UZ Finishing allowance in Z – (only for ∇) mm
XDA First grooving limit tool ∅ (abs) – (end face or rear face only) mm
XDB Second grooving limit tool ∅ (abs) – (end face or rear face only) mm
Allowance Allowance for prefinishing
● Yes
U1 contour allowance
● No
DI For zero: Continuous cut - (only for ∇) mm
U1 Compensation allowance in X and Z direction (inc) – (only for allowance)
● Positive value: Compensation allowance is retained
● Negative value: Compensation allowance is removed in addition to finishing
allowance
mm
Programming technology functions (cycles)
10.3 Contour turning
Turning
Operating Manual, 06/2019, A5E44903486B AB 483


 To Next Page