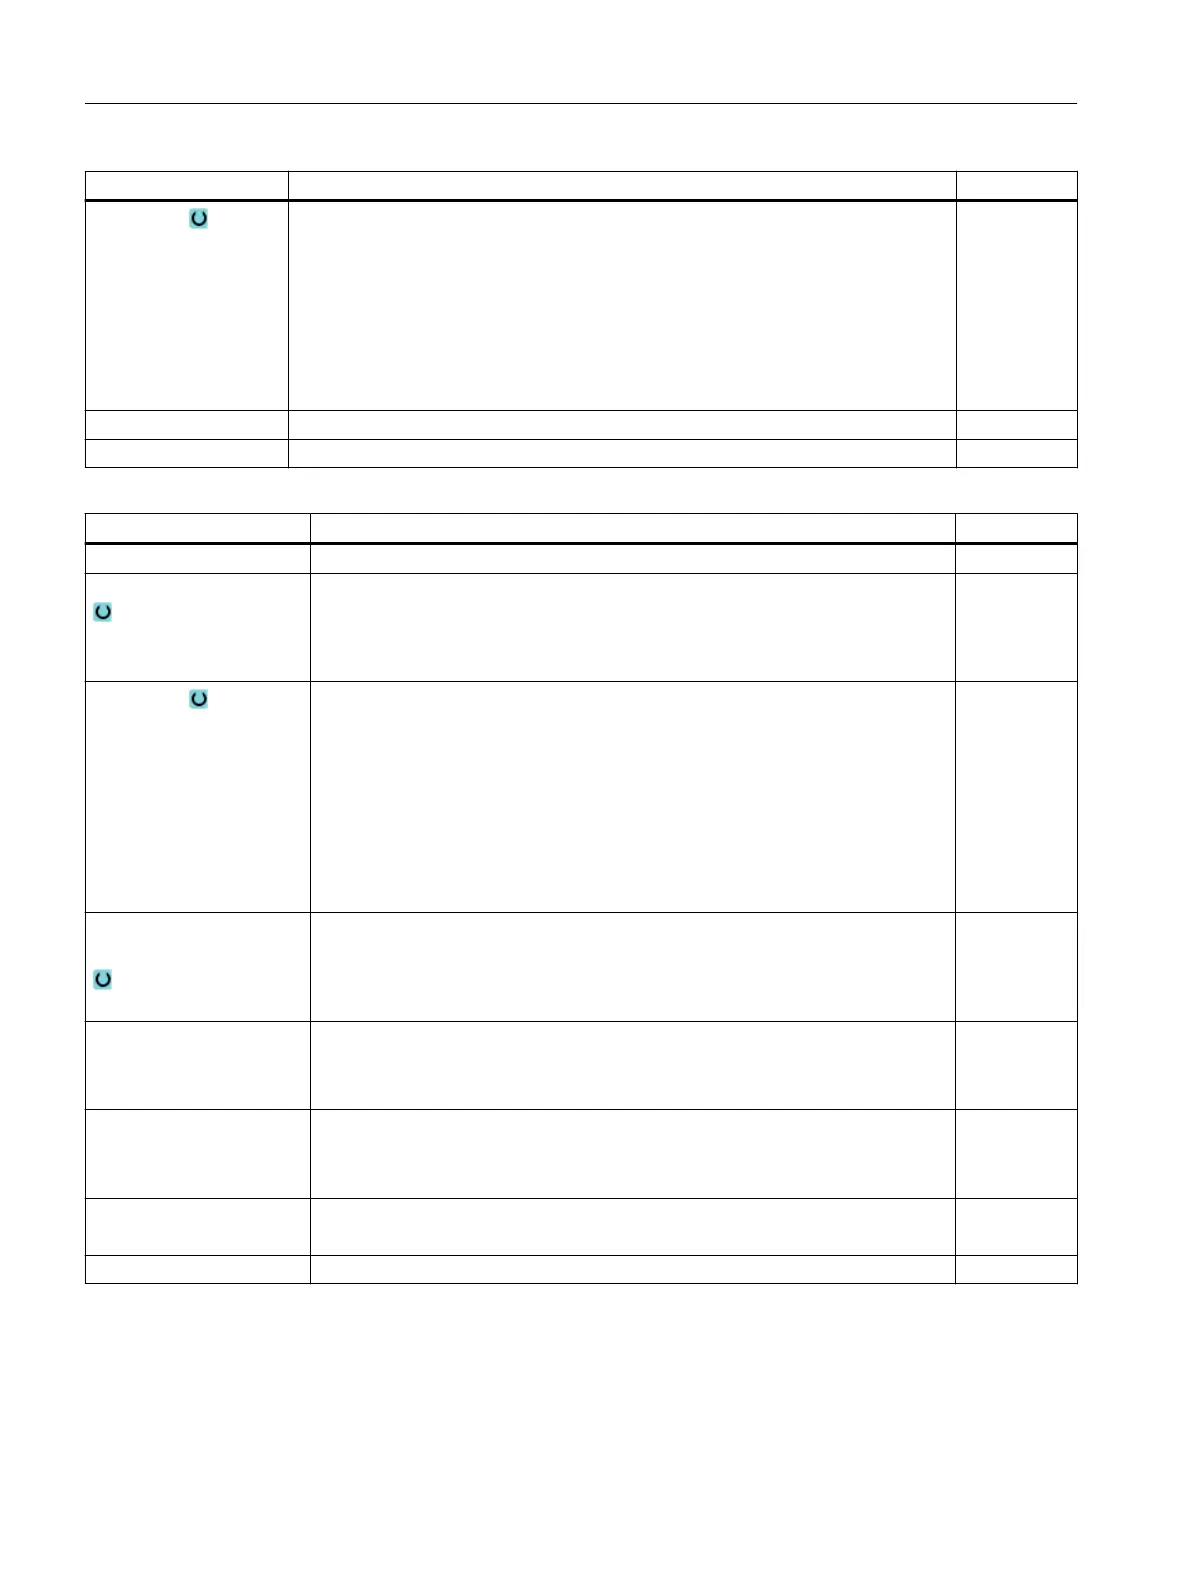
Parameters Description Unit
Work offset
- for take zero point
"yes"
Work offset in which the coordinate system offset by Z1 must be saved.
● Basic reference
● G54
● G55
● G56
● G57
● ...
Z1 Amount by which the workpiece is withdrawn from the main spindle (inc)
F Feedrate mm/min
Parameters Description Unit
Machining side function
Spindle selection
● Main spindle
Machining along the main spindle
● Counter-spindle
Machining along the counter-spindle
Work offset Work offset in which the coordinate system, which was shifted according to ZW
and by ZV as well as mirrored in Z, must be saved:
● Basic reference
● G54
● G55
● G56
● G57
● ...
Work offset
write to
● Yes
The Z value of the work offset can be directly written to the input screen form.
● No
The actual Z value of the work offset is used.
ZV - only for
work offset
write "yes"
● Offset Z = 0
● Workpiece zero is offset in Z direction (inc, the sign is also evaluated)
Park counter-spindle Traverse counter-spindle to park position - for "main spindle" selection
● Yes
● No
Z4P - for park counter-
spindle "yes"
Park position of the counter-spindle (abs); MCS
mm
Z4W Machining position of the counter-spindle (abs); MCS mm
Multi-channel machining
11.2 Multi-channel support
Turning
710 Operating Manual, 06/2019, A5E44903486B AB



 To Next Page